
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


Bending, Cutting, and Straightening in One Unit: The Process Integration Logic of Multi-Function Hydraulic Rebar Processors in Precast and Cast-in-Pla
Why Rebar Bender Cutters Matter for Process Integration
In modern precast and cast-in-place operations, traditional thermal cutting has physical and structural limits. Abrasive saws rely on high-speed friction, generating extreme heat that alters the steel's microstructure, creating a heat-affected zone (HAZ) at connection points. This heat damage can compromise the integrity of mechanical sleeve splicing or welding. Furthermore, abrasive cutting often leaves sharp burrs on the cut end, requiring extra grinding time that increases labor costs and extends project timelines.
Reducing Separate Cutting and Bending Steps
To address these issues, many construction workflows use multi-functional hydraulic processors. Rather than relying on separate stations for cutting and shaping steel, a 3-in-1 unit consolidates cutting, bending, and straightening. Interchangeable dies help achieve precise bending angles, while the straightening function corrects transit deformations. Integrating these steps minimizes material handling and saves space on crowded jobsites. However, while integration streamlines workflows, multi-function machines introduce operational trade-offs. Operators experience setup delays when physically reconfiguring the machine to switch between cut, bend, and straighten modes. Because of these changeover times, dedicated stationary machines often outperform portable multi-function units in high-volume, single-task precision.
Avoiding Heat-Affected Zones
Cutting and bending without heat damage requires capable hardware. Modern integrated units typically feature 1600W to 1700W motors, providing the torque to process rebar ranging from 4 to 25 mm (0.16 to 0.98 inches). For instance, a representativeRebar Bender Cutter illustrates typical category specifications in a portable form factor, weighing around 31 kg (68.3 lbs) with dimensions of 53 x 23 x 52.5 cm. Operating at cycle speeds of 2.5 to 3.0 seconds, machines in this class help maintain a steady operational pace. While cold processing preserves the steel's structural integrity by avoiding heat, operators must still verify if local building codes (such as ACI 318) require minor end preparation, as cut-end deformation can interfere with the threading of certain mechanical couplers.
Improving Jobsite Workflow
The operational improvements from using a combined unit are straightforward. Functional integration reduces initial equipment costs by eliminating the need to buy and maintain separate cutting, bending, and straightening machines. Housed within protective carrying cases, portable units are easy to move across complex, multi-site deployments. This mobility allows crews to position the equipment directly at the installation area, helping contractors lower capital investment, reduce material transport bottlenecks, and streamline overall site logistics.
How Hydraulic Cold Shear Technology Improves Performance
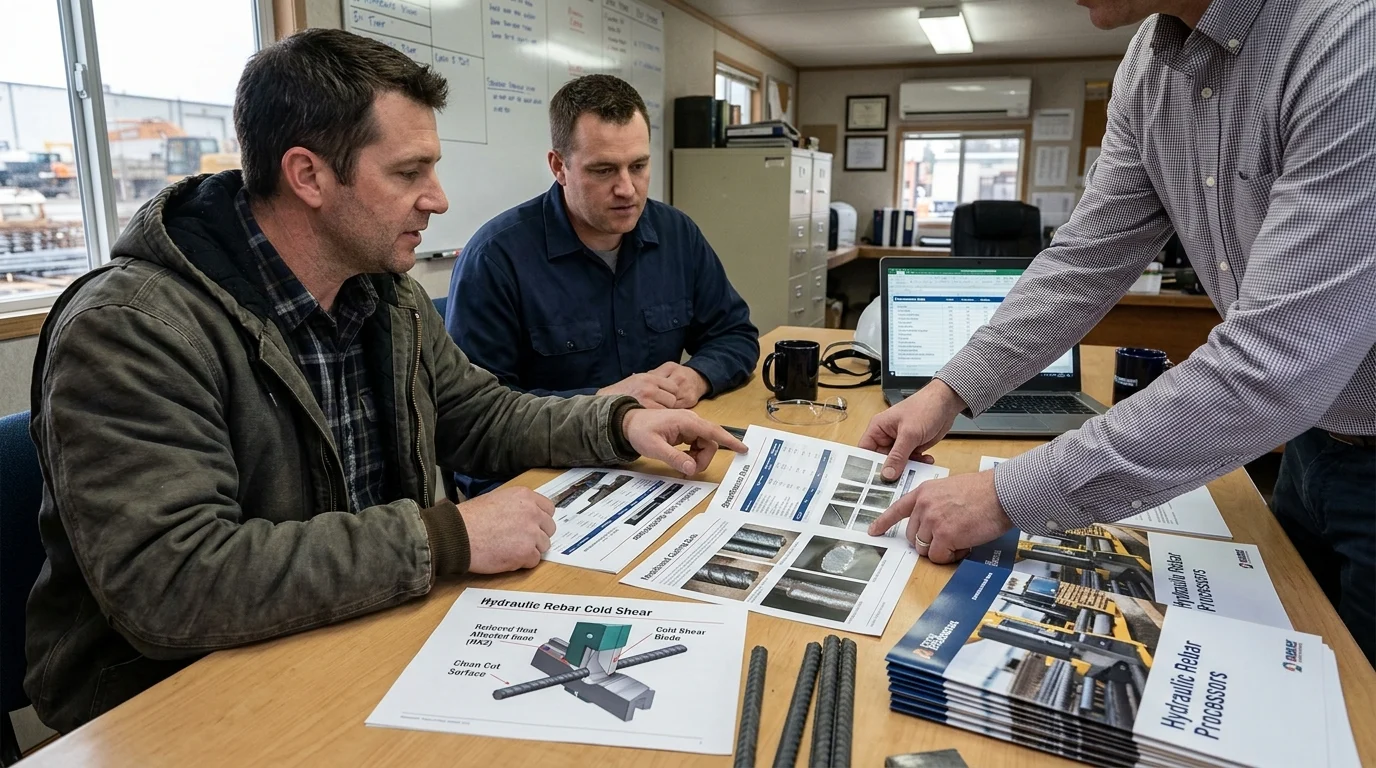
Transitioning from abrasive cutting to mechanical shearing fundamentally changes material handling on the jobsite. Because high-temperature cutting alters the steel and poses risks for load-bearing connections, modern engineering standards increasingly favor cold processing. By removing abrasive friction, contractors eliminate the heavy deburring phase and significantly reduce fire and burn hazards caused by sparks.
What Hydraulic Cold Shear Means
Hydraulic cold shear offers a mechanical alternative to friction-based cutting. This technology uses a hydraulic pump to produce high-pressure oil, which drives a heavy piston forward. The attached blade exerts localized shear stress onto the steel bar. Once the stress surpasses the material's ultimate shear strength, the rebar undergoes a rapid shear cut. While this mechanical action severs the steel without generating heat, operators must account for cut-end deformation, which can be problematic for flush-fit mechanical splices. Additionally, these systems require strict maintenance protocols, including hydraulic fluid replacements every 100 hours of operation, regular O-ring seal inspections to prevent pressure loss, and routine blade rotations to mitigate uneven wear.
Cold Shear vs. Abrasive Hot Cutting
Comparing these two methods highlights the hardware differences required for optimal performance. Cold shear units are optimized for fieldwork, leveraging high-torque motors to deliver rapid cutting speeds across a broad range of rebar sizes. Packaged in compact footprints, these units are designed to replace hazardous thermal equipment. The table below illustrates typical industry parameters for both approaches:
| Parameter | Abrasive Hot Cutting | Hydraulic Cold Shear |
|---|---|---|
| Cutting Mechanism | High-speed friction & melting | High-pressure oil & piston shear |
| Metallographic Impact | Heat-affected zone (HAZ) present | No heat damage (deformation present) |
| Edge Quality | Burred, requires heavy grinding | Shear cut (minor end deformation) |
| Cycle Time | Variable, often > 10 seconds | 2.5 to 3.0 seconds |
Quality Control Benefits
Implementing these hardware specifications improves quality control and site logistics. Integrating bending, cutting, and straightening optimizes limited workspace and ensures consistent fabrication tolerances. Furthermore, the portable form factor makes it easier for crews to move between high-rise floors or distinct precast zones. By processing the rebar directly at the point of installation, teams can immediately verify bend angles and cut lengths against structural plans, helping maintain strict quality control across the site.
Powertrain and Safety Logic
Evaluating powertrain design requires prioritizing operator safety and equipment longevity. Enclosed hydraulic processors significantly reduce the spark, noise, and dust hazards that operators historically faced with abrasive saws. Enclosing the cutting and bending mechanisms also reduces the risk of projectile debris and eliminates the fire hazards associated with hot works, creating a substantially safer working environment.
Role of Pure-Copper Motors
To avoid operational hazards, these powertrains rely on high-efficiency electrical components. At the heart of the system, motors utilizing high-purity copper windings power the hydraulic pump. Copper offers low electrical resistance and superior thermal dissipation during continuous use. This engineering ensures the motor can sustain the high torque required to actuate the heavy-duty piston without overheating, even during demanding bending and straightening cycles. Additionally, these motors are often configured for dual power-source compatibility (110V or 220V) to accommodate diverse jobsite electrical grids.
Hydraulic Power Transmission
The hardware required for hydraulic power transmission must balance output with mobility. The core powertrain uses the motor to generate high-pressure oil, translating into efficient cutting and bending speeds. This setup accommodates a broad processing range of standard rebar diameters. Despite the high output, the hydraulic assembly is contained within a compact chassis, optimizing the power-to-weight ratio for portable applications without sacrificing the force necessary to manipulate heavy-gauge steel.
Overload and Thermal Protection
Advanced units incorporate thermal overload protections and pressure relief valves that automatically disengage the powertrain if safe operating temperatures or pressure thresholds are exceeded. This prevents motor failure and blown seals during continuous heavy-duty use. Combined with a durable carrying case and an enclosed mechanical action, the system provides portability and safety, allowing a single operator to deploy the unit across various construction zones with minimal risk of equipment damage.
Key Specifications That Affect Productivity
In demanding construction schedules, equipment specifications directly dictate productivity. When crews are forced to wait on underpowered machinery, daily output bottlenecks occur, and subsequent installation tasks are delayed. Selecting a multi-function processor with the correct capacity and cycle times ensures that fabrication keeps pace with project requirements.
Rebar Diameter Capacity
Achieving peak productivity requires matching the machine's capacity to the project's demands. A diameter range of 4 to 25 mm (0.16 to 0.98 inches) covers the majority of standard rebar sizes used in commercial and residential construction. The hydraulic system must generate sufficient force to shear the thickest bars in this range and smoothly bend them to precise angles without micro-cracking the steel. Interchangeable bending dies allow operators to adjust the bending radius according to the rebar diameter, ensuring structural code compliance.
Cycle Time and Layout Efficiency
The hardware parameters dictating this workflow are engineered for maximum throughput. Powered by high-efficiency motors, premium systems ensure rapid cycle speeds. This processing time is crucial when fabricating high volumes of stirrups or preparing heavy foundation mains. The relationship between diameter capacity and cycle efficiency is detailed in the representative industry classifications below:
| Rebar Diameter | Motor Power Class | Typical Cycle Time | Processing Range |
|---|---|---|---|
| 4 to 10 mm (0.16-0.39 in) | Standard (e.g., 900W - 1200W) | 1.5 - 2.0 seconds | High-volume stirrups |
| 12 to 16 mm (0.47-0.63 in) | Mid-Range (e.g., 1200W - 1500W) | 2.0 - 2.5 seconds | Column/beam longitudinals |
| 18 to 25 mm (0.71-0.98 in) | Heavy-Duty (e.g., 1600W+) | 2.5 - 3.0 seconds | Heavy foundation mains |
Portability and Machine Weight
By leveraging 3-in-1 processing capabilities, site managers reduce initial equipment investment. A lightweight design ensures easy transport across the site. Instead of moving heavy steel bundles to a centralized fabrication shop, crews can relocate the equipment to the exact point of need, improving layout efficiency and reducing material handling bottlenecks. However, this portability means the unit requires more frequent maintenance checks—such as monitoring hydraulic fluid levels and inspecting seals—compared to heavy, stationary shop equipment.
Choosing the Right Portable Hydraulic Rebar Bender Cutter
Effective equipment procurement involves mitigating traditional process defects while maximizing utility. Transitioning to a multi-functional hydraulic processor resolves inefficiencies by combining cutting, bending, and straightening into one operation. However, selecting the correct unit requires evaluating site-specific power availability, processing volume, and structural code requirements.
Matching Parameters to Site Needs
To secure optimal field performance, equipment selection must be grounded in the specific requirements of the jobsite. Procurement teams should evaluate power-source compatibility, ensuring the unit supports the available 110V or 220V infrastructure. Furthermore, understanding the mechanics of hydraulic cold shear—where a mechanical piston applies targeted shear stress for an instantaneous shear cut—helps set realistic expectations for maintenance intervals. While this mechanical process guarantees a metallurgically stable cross-section, buyers must verify if their specific application requires perfectly square, deburred ends to meet local structural codes for mechanical splices.
Selection Decision Matrix
Evaluating hardware parameters against project demands is the most critical step in procurement. Rather than relying on a single benchmark, buyers should use a decision matrix to weigh jobsite power, processing volume, bar size, and mobility needs to find the right equipment fit:
| Project Requirement | Key Consideration | Recommended Specification |
|---|---|---|
| Jobsite Power | Generator vs. Grid availability | Dual 110V/220V compatibility; 1600W+ for heavy loads |
| Processing Volume | High-volume vs. Intermittent | Cycle times under 3.0 seconds; active cooling systems |
| Bar Size (Diameter) | Maximum thickness on site | 4 to 25 mm capacity; interchangeable bending dies |
| Mobility Needs | Multi-floor vs. Centralized | Weight under 35 kg; protective carrying case |
Commercial Value Summary
Ultimately, rigorous selection criteria are validated by tangible operational improvements. Deploying a 3-in-1 integrated machine reduces equipment investment and simplifies site logistics. The portable form factor guarantees easier transport across the jobsite, allowing fabrication to occur directly at the installation point. By consolidating cutting, bending, and straightening into a single unit, contractors can improve operational efficiency across diverse precast and cast-in-place deployments, provided they account for the necessary maintenance schedules and mode-switching setup times.
Further reading:
Key Takeaways
- Use a 3-in-1 hydraulic rebar processor when cutting, bending, and straightening must happen near the installation area with minimal material handling.
- Choose cold hydraulic shearing over abrasive cutting when avoiding heat-affected zones, sparks, and heavy deburring is important for structural connections.
- Match machine capacity to the project’s bar schedule, since typical portable units process rebar from 4 to 25 mm with 1600W to 1700W motors.
- Plan for mode changeover time because multi-function units improve flexibility but may not beat dedicated machines in high-volume single-task production.
- Inspect cut ends before using mechanical couplers, as some codes or threading systems may still require minor end preparation.
- Consider portability specifications such as 31 kg weight and compact dimensions when crews need to move equipment across multi-site or congested jobsites.
Frequently Asked Questions
What does a hydraulic rebar bender cutter straightener do?
It combines three jobsite tasks in one unit: cutting rebar, bending it to required angles, and straightening bars that were deformed during transport or handling.
Why is cold hydraulic cutting preferred over abrasive cutting?
Cold hydraulic shearing avoids heat-affected zones, reduces sparks and burn hazards, and typically leaves fewer burrs than abrasive cutting, helping preserve rebar integrity at connection points.
What rebar sizes can a typical 3-in-1 unit process?
Machines in this category commonly handle rebar from 4 to 25 mm, depending on steel grade, die setup, and operating conditions.
Is a multi-function rebar processor faster than separate machines?
It can speed up mixed-task workflows by reducing handling, but dedicated machines may be faster for high-volume cutting or bending because multi-function units require setup changes between modes.
How portable is the referenced MAXMach rebar bender cutter?
The referenced unit is designed for jobsite mobility, weighing about 31 kg and measuring approximately 53 x 23 x 52.5 cm.