
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


Floating to Finishing: The Engineering Sequence of Ride-On Power Trowel Operations for FF/FL-Compliant Concrete Floors

Ride-On Concrete Power Trowel Basics
When I look at achieving strict floor tolerances on large-scale concrete pours, equipment selection is everything. The transition from manual or walk-behind tools to a ride-on concrete power trowel fundamentally shifts how we manage both labor and slab quality. Let's break down the engineering parameters that make this possible.
Why FF/FL Floor Tolerances Matter
To understand floor compliance, we have to look at the physical parameters of the equipment. A ride-on trowel features a substantial operating net weight of 268kg/591lb spread across a non-overlapping 2000mm/78.7in double-pan design. In contrast, a standard walk-behind unit offers a much smaller working footprint of 600-900mm/23.6-35.4in and significantly less downward mass.
The difference here lies in compaction and consistency. The heavier self-weight of the ride-on, combined with its ergonomic driving platform and comfortable seat, changes the dynamic of the pour. Walk-behind operators accumulate massive physical fatigue over hours of wrangling a vibrating machine, which inevitably leads to inconsistent overlapping passes and fluctuating finishing quality.
For FF (Flatness) and FL (Levelness) compliant floors in high-standard warehouses or airports, consistent downward compaction is non-negotiable. The ride-on's stable double-pan balance prevents the dips and ridges caused by tired operators. Eliminating operator fatigue while maintaining uniform compaction translates directly into passing strict FF/FL compliance tests on the first try.
Floating vs Finishing Sequence
Concrete finishing is a time-sensitive sequence requiring distinct power and speed profiles. A ride-on unit like the ST836 utilizes a twin-cylinder, electric-start engine delivering 22.5HP/16.8kW, driving 10 blades with an infinitely variable speed of 60-155 r/min. Meanwhile, a typical walk-behind relies on a single-cylinder 5.5-13HP/4.1-9.7kW engine, pushing 4 to 8 blades at a narrower 40-140 r/min.
The twin-cylinder design provides much smoother torque and lower vibration than a single-cylinder block. During the floating stage—which must happen before the concrete's initial set—I keep the blades flat and run at a low 60-80 r/min to lift the paste and level the slab. As we transition to the finishing and sealing stage before the final set, I increase the blade pitch and ramp up to a high 120-155 r/min to burnish the surface.
The ride-on's wider RPM range and twin-cylinder stability allow it to handle the heavy drag of wet floating and the high-speed friction of final finishing without bogging down. This precise RPM control across a wider speed band means we can flawlessly transition from pulling up paste to sealing the surface with optimal structural integrity.
Key Benefits for Large-Area Slabs
When bidding on massive industrial slabs, throughput dictates profitability. A dual-rotor ride-on trowel achieves an output of 500-1000 m²/h. Conversely, a walk-behind trowel peaks at roughly 100-200 m²/h.
We are looking at a 3x to 5x productivity multiplier. One ride-on unit effectively replaces three to four walk-behind machines and, crucially, saves the labor costs of three to four skilled operators. For large logistics centers or parking garages, we prioritize ride-on machines for the main expanses, keeping walk-behinds strictly reserved for complex edges and tight corners.
Beyond just speed, this equipment comes with long-term peace of mind. With mechanical test reports provided upfront and a solid 1-year warranty on core components, the production capacity guarantees stable quality day in and day out. Ultimately, a 5x efficiency gap translates directly into compressed project timelines, slashed labor overhead, and a massive competitive advantage in commercial bidding.
Further reading:
MAXMACH ST836 vs Walk-Behind Trowels
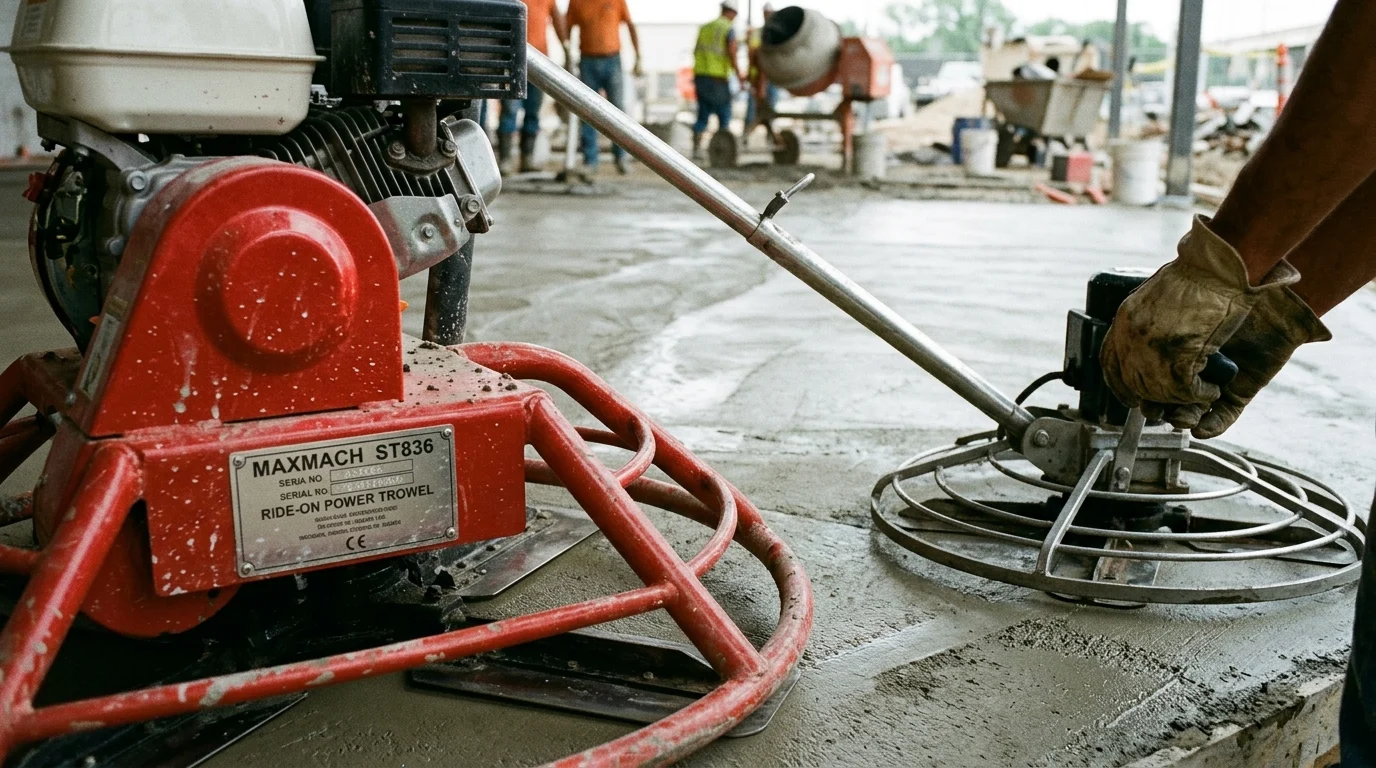
To understand the shift in project dynamics, it helps to put specific machine classes head-to-head. Taking a close look at a heavy-duty unit like the MAXMACH ST836—used here as a representative example of modern ride-on capabilities—alongside standard walk-behind trowels highlights exactly where and why each type should be deployed. It is not about one rendering the other entirely obsolete; it is about deploying the right mechanical advantage for the specific geometry and scale of the pour.
Let's break down the operational contexts, the dimensional realities, and the weight disparities. By quantifying these differences, a clear framework for equipment selection can be built for any given job site.
When to Use a Ride-On Trowel
Deploying a ride-on trowel is a practical choice for expansive, unobstructed concrete pours, such as factory floors, warehousing facilities, parking garages, and airport aprons. In these environments, the sheer volume of concrete requires high-capacity equipment.
A ride-on machine features a dual-pan design engineered for continuous operation across open terrain, whereas a walk-behind machine features a single pan designed for pedestrian-paced, localized finishing. Because the ride-on trowel thrives on momentum and wide-open spaces, it lays down a consistent, overlapping pattern that minimizes surface deviations.
For high-tolerance, large-area slabs, the ride-on trowel is a highly effective mechanical solution for meeting strict flatness specifications. However, operating these heavy machines requires strict adherence to safety and operational caveats. Heavy ride-on units require a minimum slab thickness and sufficient load-bearing capacity to prevent structural damage. Operators must also be acutely aware of tip-over hazards on uneven transitions, the necessity of Roll-Over Protective Structures (ROPS) or fall protection near drop-offs, and struck-by or edge-collapse risks if the machine is driven too close to unsupported slab perimeters.
When Walk-Behind Trowels Still Fit
Despite the prevalence of ride-on machines in open spaces, modern walk-behind trowels remain an essential tool in a concrete contractor's arsenal. Complex floor plans cannot be finished with massive machinery alone.
Walk-behind trowels offer maneuverability with a compact footprint, easily navigating around plumbing stub-outs, columns, and tight edge boundaries where a ride-on trowel is physically incapable of reaching.
This dictates a hybrid approach. The ride-on machine acts as the primary workhorse for the bulk of the square footage, while the walk-behind serves as the precision instrument for the perimeter, obstacle-heavy zones, and smaller tolerance-critical pours. Retaining walk-behind units ensures uniform finishing quality across the entire slab, preventing the perimeter from becoming the weak link in the floor's overall integrity.
Size, Weight, and Coverage Comparison
The physical attributes of the trowel—size, weight, and coverage—dictate how it interacts with the curing concrete, determining the density and smoothness of the final wear layer. The table below outlines the specifications of a representative heavy-duty ride-on unit compared to a standard walk-behind model. Note: These parameters are illustrative examples; exact specifications vary significantly by manufacturer and model.
| Specification | MAXMACH ST836 (Ride-On) | Typical Walk-Behind |
|---|---|---|
| Working Diameter | 2000 mm (78.7 in) | 600-900 mm (23.6-35.4 in) |
| Net Weight | 268 kg (591 lb) | 75-100 kg (165-220 lb) |
| Dimensions (L×W×H) | 2019×1040×1270 mm (79.5×40.9×50 in) | Varies, typically compact |
| Productivity Rate | 500-1000 m²/h (5381-10763 sq ft/h) | 100-200 m²/h (1076-2152 sq ft/h) |
| Rotors | Dual (Non-overlapping) | Single |
The ride-on's mass, distributed over a wide dual-rotor base, provides greater downward compaction force compared to the lighter, single-rotor walk-behind. This heavier footprint forces the aggregate down and seals the surface tighter. This balance of weight and expansive coverage translates into improved surface density and a more consistent final floor profile.
Honda GX690 Powertrain Performance
The engine is a critical component of any Power Trowel. When pushing heavy steel blades against curing concrete, consistent, smooth torque is required. If the engine bogs down or vibrates excessively, that inconsistency transfers directly into the slab, leaving chatter marks and uneven finishes.
The powertrain is where the separation between light-duty and professional-grade equipment becomes obvious. Analyzing a setup like the Honda GX690 found on many premium ride-ons versus the standard powerplants on walk-behind units illustrates the importance of sustained torque.
Twin-Cylinder Engine Advantages
The architectural design of the engine block dictates the machine's capability under load. When finishing concrete, especially during the high-speed burnishing phase, the resistance on the blades is immense.
Heavy-duty ride-ons often utilize a twin-cylinder, 4-stroke Gasoline Engine, such as the Honda GX690, boasting a 688cc displacement and delivering a rated power of 22.5 HP (16.8 kW) at 3600 rpm. Walk-behind trowels typically utilize smaller, single-cylinder engines ranging from 5.5 to 13 HP (4.1 to 9.7 kW).
This twin-cylinder engine provides consistent torque, allowing the heavy machine to maintain blade speed even when the concrete begins to set hard. While single-cylinder engines are perfectly suited for the lighter frames of walk-behinds, they can face challenges matching the sustained torque of a twin-cylinder on expansive, rapidly curing slabs. The twin-cylinder architecture helps ensure consistent blade rpm under heavy load, preventing the machine from digging in and compromising the floor's flatness.
Power Smoothness and Operator Control
Power is most effective when it can be controlled smoothly. Operator ergonomics and machine vibration play a significant role in the outcome of a large-area pour. Concrete finishing is exhausting work, and fatigue can lead to surface inconsistencies.
A twin-cylinder ride-on typically features an electric start, an ergonomic seat, and dual joysticks, with the V-twin engine design inherently canceling out primary vibrations. A single-cylinder walk-behind requires the operator to walk on the uneven concrete and can transfer more engine vibration directly into the operator's hands and arms.
The ride-on effectively isolates the operator from much of the physical toll of the job. The smooth power delivery minimizes micro-chatter at the blade tips. Reducing operator fatigue and machine vibration translates into focused control, minimizing human error and maintaining flatness over thousands of square meters.
Fuel, Reliability, and Maintenance Factors
On a commercial job site, equipment downtime during a pour can lead to permanent slab defects that require expensive grinding and remediation.
Premium powertrains offer a predictable lifecycle and robust reliability for high-volume contractors. Walk-behind engines are also highly reliable, but their proximity to the floor exposes them to more dust ingestion, requiring strict maintenance schedules.
The electric start on modern ride-on units prevents the downtime associated with manual recoil cords. Utilizing a smooth, tested twin-cylinder setup translates into better operator focus, consistent finishes, and long-term equipment uptime, ensuring the machine is ready during the critical curing window.
Finishing System and Operating Control
Moving from the powertrain to the working components of the machine, the finishing system—comprising the pans, rotors, and blades—is where the actual concrete manipulation occurs. The mechanics of how these blades interact with the slab surface determine the final density, gloss, and durability of the floor.
This system's effectiveness relies heavily on proper tooling selection. Using float pans or clip-on float blades during the initial passes helps break open the surface and generate paste without digging into the concrete. As the slab stiffens, operators switch to combination blades or dedicated finish blades, increasing the pitch to burnish and seal the floor. The ability to precisely control these variables allows an operator to adapt to the changing state of the curing concrete.
Dual Non-Overlapping Pan Layout
The geometry of the rotors dictates the machine's footprint and its operational balance. A wider, more stable base creates a flatter floor.
Many ride-on trowels feature a dual non-overlapping pan layout. Because the rotors themselves do not overlap, the machine leaves a small uncut gap between the two spinning pans. To prevent ridges and ensure the center strip is finished evenly, the operator must deliberately overlap their driving passes by a few inches on each subsequent run. This non-overlapping design allows the rotors to spin without the risk of blades colliding, simplifying the mechanical drivetrain.
The dual rotors provide a large, stable platform that distributes the machine's weight evenly, preventing it from tipping or gouging the surface. This creates a stable compaction zone, essential for sealing large areas without introducing tilt or wave defects.
Low-Speed Floating at 60–80 rpm
The initial floating stage is critical. It must be completed before the concrete's initial set to push down the coarse aggregate and bring a layer of workable cement paste to the surface.
During this phase, a typical ride-on trowel operates at a low speed of 60-80 rpm, with the blades (or float pans) pitched completely flat, utilizing the machine's weight to massage the concrete. The walk-behind also operates at lower speeds (around 40-60 rpm) with flat blades, but relies on multiple, overlapping manual passes to achieve the same paste generation.
The ride-on's heavier weight combined with this specific rotation generates a uniform paste layer efficiently. Executing the low-speed float correctly ensures the slab is prepped and leveled precisely within the optimal hydration window.
Blade Speed Range and Finish Quality
As the concrete stiffens and approaches its final set, the objective shifts from leveling to sealing and polishing. This requires higher blade speeds and a steeper blade pitch.
Modern ride-on trowels offer a stepless adjustable blade speed range, allowing the operator to increase the rotational speed for the final finish with an increased blade angle.
| Finishing Parameter | Ride-On Trowel (Example) | Walk-Behind Trowel |
|---|---|---|
| Total Blades | 10 (Dual 5-blade rotors) | 4 to 8 (Single rotor) |
| Speed Adjustment | Stepless variable | Stepped / Manual throttle |
| Speed Range | 60-155 rpm | 40-140 rpm |
| Floating Speed | 60-80 rpm | 40-60 rpm |
| Finishing Speed | 120-155 rpm | 90-140 rpm |
(Note: Speed ranges and blade counts are illustrative examples and vary by manufacturer.)
The ride-on's ability to reach higher RPMs provides the friction and heat generation necessary to tightly seal the pores of the concrete and create a hard, burnished finish. The difference in blade count and rotational speed translates into efficient compaction and faster sealing during the final passes.
Productivity, Quality, and Payback
Ultimately, the decision to upgrade equipment comes down to the bottom line. Engineering specs must generate a return on investment (ROI) through productivity rates, labor reduction, and the avoidance of costly quality disputes.
Let's look at the economics of deploying a ride-on trowel versus relying on a fleet of walk-behind units. By quantifying the output per shift and the associated labor costs, the financial argument for large-scale mechanization becomes clear.
How to Estimate Output per Shift
Estimating output per shift is the first step in bidding a job accurately. Contractors need to know exactly how much square footage a crew can handle before the concrete sets.
As noted in the specifications, a single operator on a ride-on trowel can theoretically finish up to 1000 m²/h (10763 sq ft/h) under ideal conditions, whereas a walk-behind unit yields a fraction of that. However, as established earlier, practical output is often lower. Meeting strict FF/FL tolerances demands deliberate, controlled pacing rather than operating at top speed, which naturally reduces the maximum theoretical coverage rate.
Even with this adjusted pacing, the multiplier effect remains substantial. One ride-on machine effectively replaces multiple walk-behind trowels in terms of raw coverage. This level of throughput allows contractors to schedule larger single pours, reducing the number of construction joints and formwork setups required, which accelerates the construction timeline.
Labor Savings vs Walk-Behind Methods
Labor is consistently the highest variable cost on any concrete project. Optimizing the headcount required for the finishing phase improves profit margins.
Utilizing one ride-on trowel requires only one trained operator seated on a platform. Achieving the same output with walk-behinds requires multiple operators walking on the wet slab, managing machine torque for hours.
This isn't just about reducing salaries per shift; it is about preserving quality. In large projects, operator fatigue with walk-behinds accumulates, which can lead to a drop in focus and a fluctuation in finishing quality toward the end of the shift. The ride-on mitigates much of this physical fatigue. By reducing operator exhaustion, contractors can maintain consistent finishes from the first square meter to the last, while simultaneously optimizing payroll.
Decision Guide for Buying a Ride-On Trowel
Choosing the right equipment profile requires an honest assessment of a contractor's typical project pipeline. The machinery must match the environment.
If a portfolio consists primarily of large, open commercial slabs, investing in a ride-on trowel is easily justified by the labor savings and schedule acceleration. However, if projects involve narrow aisle widths, complex formwork, or strict budget constraints on smaller pours, maintaining a fleet of reliable walk-behind units might be the more practical choice. Ultimately, the decision should factor in project size thresholds, minimum slab thickness requirements, transport logistics, capital cost barriers, and the specific geometric constraints of typical job sites to ensure the equipment matches operational realities.
Key Takeaways
- Establish FF/FL compliance before troweling through proper subgrade preparation, strike-off, screeding, bull-floating, and straight-edging.
- Use Ride-On Power Trowels on large slabs to apply wider, heavier, and more uniform compaction than walk-behind machines can provide.
- Begin the floating stage with pans or flat blades at low speed only after the concrete can support the machine without aggregate displacement.
- Increase blade pitch gradually as the slab stiffens to move from floating into combination and final finishing passes.
- Avoid late or excessive high-speed burnishing because it can trap moisture and cause surface delamination.
- Match troweling timing to the concrete mix design, slab conditions, temperature, humidity, and wind rather than relying on a fixed clock schedule.
Frequently Asked Questions
Can a ride-on concrete power trowel correct poor FF/FL results?
No. FF/FL performance is primarily established by subgrade preparation, accurate strike-off, screeding, bull-floating, and straight-edging. A ride-on trowel helps preserve and refine those numbers, but it cannot repair a poorly placed slab.
When should a ride-on power trowel begin floating?
Begin only after bleed water has disappeared and the concrete can support the machine without sinking or displacing aggregate. Starting too early can damage the slab and reduce surface quality.
Why are ride-on trowels preferred for large commercial floors?
Ride-on trowels cover more area, apply more consistent pressure, and use dual rotors to compact and flatten the surface over a wider span than walk-behind units, improving productivity and finish consistency.
What is the correct troweling sequence from floating to finishing?
Start with float pans or flat blades at low speed, then increase blade pitch as the slab stiffens. Finish with higher-speed burnishing only when the surface can tolerate it without trapping moisture.
How do blade pitch and speed affect the final floor?
Flat blades help open and level the surface during floating. As pitch and speed increase, the machine densifies, smooths, and seals the surface. Incorrect timing can cause waves, tearing, or delamination.