
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


From Grinding to Polishing: Evaluating the Dual-Action Trowel Machine for Concrete Floor Densification and Surface Sealing
Why Concrete Trowel Machines Matter
In large-scale industrial flooring projects, the evolution of surface finishing technology has fundamentally shifted the approach to concrete preparation. The industry is no longer reliant on labor-intensive manual screeding and hand-troweling to achieve a durable surface. Instead, the introduction of mechanized finishing equipment has standardized quality across massive square footages. To understand this shift, one must examine the process through a strict technical lens, progressing from the equipment's underlying mechanics to its operating parameters and measurable quality results.
The core philosophy driving modern concrete finishing is the concept of completing the primary surface work before the slab fully sets. By eliminating the need for a separate mortar leveling layer, operators integrate mechanical compaction directly into the primary pour. While subsequent steps like grinding, polishing, and the application of chemical densifiers (such as silicates) or liquid sealers are required later to achieve true chemical densification and long-term sealing, the trowel machine provides the crucial mechanical foundation. It delivers mechanical surface compaction—closing the pores and creating a hard, burnished surface that improves surface abrasion resistance rather than the bulk compressive strength of the slab. This monolithic approach demands precise timing and reliable machinery to manipulate the concrete during its critical curing phases.
Commercial and engineering challenges
The primary engineering challenge in industrial flooring is managing the hydration rate of a massive concrete pour while ensuring a uniform, defect-free surface. When pouring high-standard factories, warehouses, or airport hangars, the concrete begins to cure immediately, creating a narrow window of workability that is highly sensitive to ambient temperature, humidity, and mix design. Historically, manual finishing could not keep pace with large pours, leading to cold joints, uneven curing, and structural weak points. Commercially, contractors face immense pressure to reduce labor costs and accelerate project timelines without compromising the floor's load-bearing capacity or aesthetic finish.
Mechanized solutions address these challenges head-on by replacing human physical force with consistent, engine-driven pressure. To succeed, operators must maintain high coverage rates (detailed in the productivity tables below) to keep pace with the curing concrete. In practice, operators deploy machines exactly as the bleed water dissipates, dramatically reducing surface delamination and ensuring adherence to strict commercial tolerances. However, operators must also be cautious of over-troweling, which can trap bleed water beneath the surface and cause blistering or delamination. Furthermore, contractors must implement strict safety protocols, including providing proper ventilation for carbon monoxide when using combustion engines indoors and maintaining clear safety zones around rotating blades.
Dual-action machine definition
To navigate these commercial and engineering hurdles, contractors rely on versatile equipment such as a Concrete Trowel Machine. While the term "dual-action" in common industry parlance often refers to dual-rotor (ride-on) machines, in the context of this article, it explicitly describes the machine's dual-purpose functionality: utilizing pan-type tools for initial floating and blade-type tools for final finishing. These machines are available in single-rotor (walk-behind) and dual-rotor (ride-on) setups. Powered either by electric motors or internal combustion Gasoline Engines, these machines provide the necessary torque to manipulate curing concrete.
These machines operate by driving a rotor equipped with cross-arranged blades or a floating pan. As the rotor spins, it applies targeted downward pressure and rotational friction to scrape, compact, and tighten the slab. While traditional dry diamond polishing involves abrasive grinding on fully cured concrete, Power Troweling achieves a high-gloss, hard-troweled finish on wet concrete through high-friction mechanical mechanical compaction. Operating this equipment requires transitioning from the broad, flat contact of the pan to the precise, angled contact of the blades, executing both the initial heavy floating and the final burnishing within the same operational lifecycle.
Productivity and finish quality goals
The ultimate goals in deploying these machines are maximizing productivity and achieving an impeccable finish. The methodology mandates that all floating and finishing occur before the concrete reaches its final set. By integrating the surface finishing with the initial placement, contractors avoid the delamination risks associated with applying secondary mortar leveling layers. Timing is critical: rough floating must conclude before the initial set, and final troweling must wrap up prior to the final set.
During construction, the concrete's plasticity is monitored constantly. The operator typically steps onto the slab when it can support a person's weight while leaving only a slight footprint—generally estimated at 3 to 5 millimeters (0.12 to 0.20 inches) deep, though this serves as a rough guideline that varies significantly based on the mix design and slab thickness. The machine is then guided systematically over the surface. The result is a floor that exhibits exceptional flatness and high abrasion resistance. It is important to note that while power troweling creates a dense surface, it is not a substitute for proper curing methods (such as moisture curing or curing compounds) or the timely cutting of control joints to prevent random cracking. Additionally, not all slabs require a glossy, burnished finish; floors slated for certain coatings or tile often require a more open, lightly floated texture.
The transition from raw placement to a tightly compacted slab is a precisely timed response to concrete's hydration kinetics—a response that the Trowel Machine executes through mechanical pressure and rotational control.
How the Process Moves from Floating to Finishing
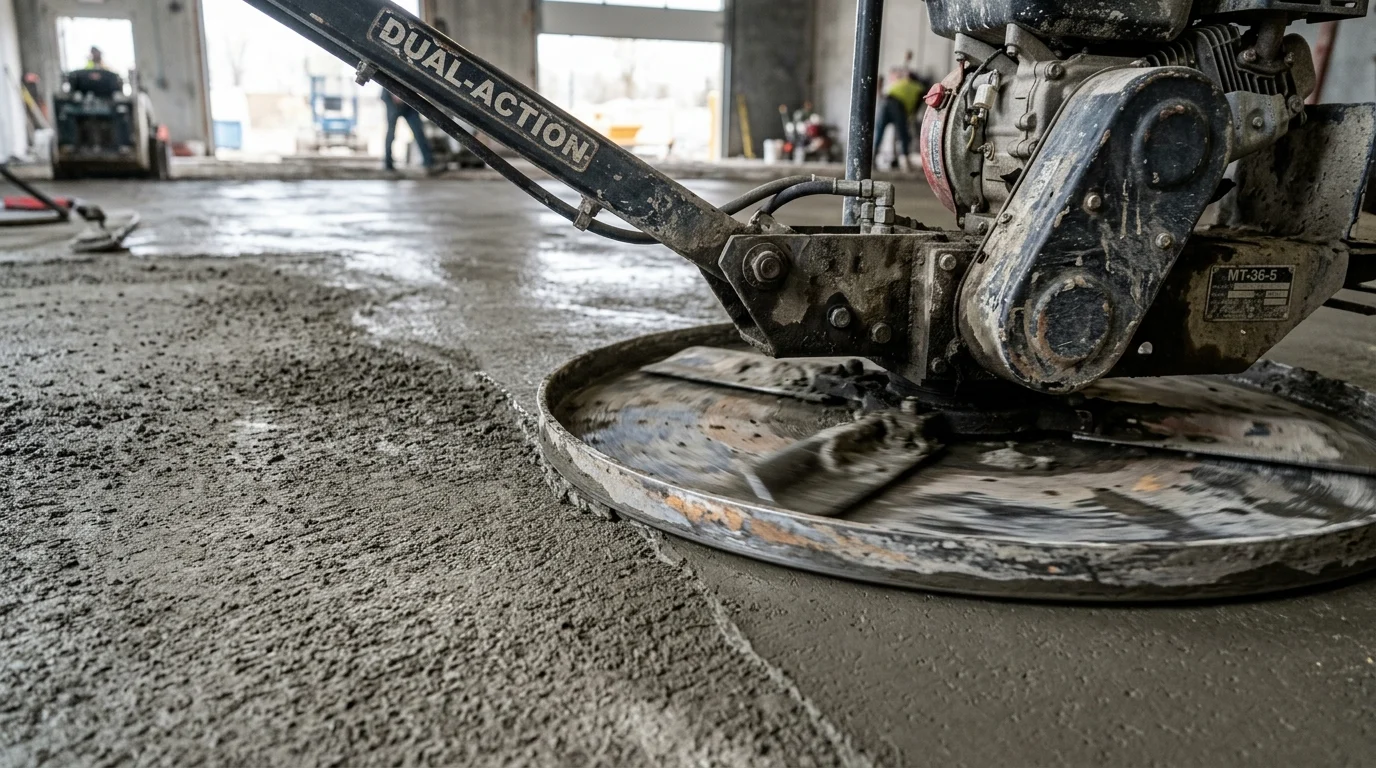
Transitioning from a freshly poured, wet slab to a hard, finished floor requires a phased mechanical approach. This workflow is divided into two distinct stages: floating and finishing. Each stage utilizes different attachments on the trowel machine to achieve specific physical changes in the concrete's surface layer. By adhering to a rigorous, well-timed progression, operators ensure that the floor achieves its maximum potential strength and aesthetic appeal.
Rough floating with pan-type tools
The initial stage of surface preparation relies on pan-type tools, commonly referred to as floating pans. Pan floating serves a twofold purpose: downward compaction and upward slurry extraction. As the heavy, flat pan rotates over the wet concrete, it forces the coarse, sandy aggregate downward into the slab. Simultaneously, the vacuum and friction created by the pan draw the fine cementitious paste—or slurry—upward to the surface. This action opens the concrete's pores, allowing trapped air and excess bleed water to escape.
Operators typically aim to extract a slurry layer of approximately 3 millimeters (1/8 inch) as a general example, though this fluctuates based on the concrete mix, slab thickness, and ambient temperature. The operation must be meticulously timed; pan floating must be completed before the cement reaches its initial set. Operators guide the machine in overlapping passes, ensuring every square inch of the surface is agitated and leveled. The result is a uniform, porous surface layer rich in cement paste, perfectly primed for the subsequent finishing steps.
Fine finishing with blade-type trowels
Once the surface has been floated and the initial set begins, the pan is removed to expose the blade-type trowels for fine finishing. The focus now shifts from extraction to compaction and mechanical tightening. The rotating blades, arranged in a cross pattern on the chassis, glide over the slurry-rich surface. As the concrete hardens, the blades compress the paste, closing the porous structure created during the floating phase.
Rotor speed is typically adjusted based on the concrete's stiffness. During this operation, the operator gradually increases the blade pitch (the angle of the blades relative to the floor) as the concrete stiffens. This finishing work must be entirely concluded before the concrete's final set. The result is a dense, smooth surface that minimizes moisture loss, promoting optimal curing and maximizing the floor's surface abrasion resistance.
Recommended step-by-step workflow
To guarantee consistent results, a strict, step-by-step workflow aligned with industry guidelines, such as ACI 302, is typically implemented on the jobsite. Systematic coverage is essential for uniform mechanical compaction. A typical hard-troweling process might require around five complete passes as a baseline example, though this fluctuates based on ambient conditions, concrete mix, and machine type.
The operation usually begins with two perpendicular passes using the floating pan to ensure all aggregate is submerged and the slurry is evenly distributed. Following the pan removal, crews execute additional passes with the finishing blades. With each successive pass, the operator increases the blade pitch and engine RPM to match the increasing hardness of the slab. Surface flatness is continually measured during these passes, allowing the machine to perform repeated finishing on any localized areas that do not meet the required tolerances. The ultimate result is a floor that meets exacting standards for surface flatness, straightness at the skirting lines, and perfectly aligned joint grids.
This shift from floating to finishing adapts to the concrete's curing phases to build structural density.
Key Working Principles and Technical Parameters
To master concrete floor finishing, operators must understand the mechanical synergy between the trowel machine and the curing slab. The equipment is a highly tunable device designed to apply specific forces at specific times. In this section, we will break down the key working principles and technical parameters that define machine performance, exploring how machine performance translates to floor quality.
Powered rotor and blade contact mechanics
Trowel machines transfer rotational kinetic energy into downward compressive and lateral shearing forces. This is achieved through a powered rotor driving a set of four to eight blades arranged in a precise cross configuration on the chassis. When equipped with a pan, the contact mechanics distribute the machine's weight over a large surface area, producing low unit pressure. When equipped with blades, the contact area shrinks drastically, concentrating the machine's weight onto the narrow leading edges of the steel blades.
Machine weight plays a major role in this interaction, ranging from lightweight units for small edge-work up to heavy-duty walk-behind models. During operation, the operator must balance the machine's throttle and steering to maintain a consistent glide path over the concrete. The result of these precise contact mechanics is the ability to selectively scrape, compact, and smooth the surface, pushing the concrete paste into a tightly bound matrix.
Pan-type vs blade-type specification comparison
Understanding the distinct specifications of pan-type versus blade-type setups is crucial for jobsite planning. Different surface areas yield different compaction rates. A floating pan maximizes surface contact to lift slurry, while blades minimize contact to apply high-friction compaction.
To illustrate these parameters, consider the following technical comparison typical of standard commercial equipment:
| Specification Feature | Metric Parameter | Imperial Parameter |
|---|---|---|
| Standard Rotor Diameter | 720 mm | 28 in |
| Operating Speed Range | 40 - 70 r/min | 40 - 70 RPM |
| Electric Motor Power | 2.2 - 3.0 KW | 3.0 - 4.0 HP |
| Combustion Engine Power | 4.1 - 9.7 KW | 5.5 - 13.0 HP |
| Standard Machine Weight | 34 - 125 kg | 75 - 275 lb |
During operation, crews must swap from pans to blades swiftly to avoid missing the curing window. Adhering to these specification limits ensures a standardized finish that prevents burning or tearing the concrete surface.
Power, speed, weight, and blade size factors
The interplay of power, speed, weight, and blade size determines the overall efficacy of the machine. Higher horsepower engines maintain consistent rotor speeds even when the concrete becomes highly viscous near its final set. A typical rotor diameter, such as 720 mm (28 in), offers an optimal balance between coverage area and maneuverability, especially in complex topographies or around structural columns.
In terms of operation, the operator uses the throttle to adjust the speed from lower RPMs during the initial wet passes to higher RPMs during the final finishing phase. The machine's weight provides the necessary downward thrust without requiring the operator to physically push the machine into the floor. Routine maintenance—such as checking engine oil, monitoring blade wear, and ensuring safety guards are intact—is critical to maintaining this efficiency and protecting the operator.
Why Blade Pitch Is Critical
Among all the adjustable parameters on a trowel machine, blade pitch is arguably the most critical. It is the primary mechanism through which the operator responds to the minute-by-minute hardening of the concrete slab. By manipulating the angle of the blades, operators directly alter the physics of how the machine interacts with the floor, moving seamlessly from broad compaction to aggressive, high-pressure smoothing.
How pitch changes contact area
Blade pitch adjustment relies on the inverse relationship between contact area and unit pressure. The trowel machine is equipped with a pitch adjustment mechanism that allows the operator to change the blade angle rapidly and precisely without stopping the engine. By turning a manual control handle, the blades can be tilted on their axes.
An example adjustable pitch range spans from 0° (completely flat) to 12° (maximum tilt), though operators should consult the manufacturer manual for specific limits based on the equipment and slab thickness. As the pitch angle increases, the surface area of the blade in contact with the concrete decreases. Consequently, the weight of the machine is distributed over a much smaller area, drastically increasing the downward pressure per square inch. This operation physically raises the machine's chassis slightly higher off the ground. The result is a highly concentrated shearing force that is necessary for the final surface tightening before the concrete reaches its final set.
Practical pitch adjustment sequence
Executing the proper pitch adjustment sequence requires matching the blade angle to the exact hydration state of the concrete. If the pitch is too steep too early, the blades will slice into the soft concrete, creating deep ridges; if it is too flat too late, the machine will merely glide over the surface without properly compacting it.
The sequence generally begins at 0° during the first pass after pan removal. At this stage, the concrete is still relatively relatively plastic. As the floor stiffens, the operator incrementally adjusts the manual control handle, increasing the pitch in typical increments of 2° to 3° with each successive pass. By the final pass, the blades are often pitched near their maximum angle, and the rotor speed is maximized. This progressive compaction yields a dark, hard-troweled finish.
Common pitch-related troubleshooting
Even with a clear sequence, operators frequently encounter pitch-related troubleshooting scenarios on the jobsite. Troubleshooting relies on reading the concrete's feedback. For instance, if the machine begins to bounce or chatter violently, it often indicates that the unit pressure is too high for the current state of the concrete. However, operators should also note that chattering or bouncing can result from blade wear, rotor imbalance, or underlying subgrade issues, not solely from an excessive pitch angle.
If the pitch is the culprit, the operator must immediately reduce it, backing off the manual control handle to drop the maximum angle closer to a mid-range pitch, thereby increasing the contact area and stabilizing the machine. Conversely, if the surface appears cloudy and fails to develop a sheen, the pitch is likely too flat, and the operator must increase the angle to apply more pressure. Proactive troubleshooting prevents surface tearing and ensures a uniform, defect-free slab.
How to Select and Validate the Right Machine
The final phase of project planning involves selecting the appropriate machinery for the scale of the job and establishing rigorous validation criteria to ensure the finished product meets engineering specifications. Making the correct choice between walk-behind and ride-on units directly impacts project profitability and timeline adherence. Project managers must evaluate machine selection, calculate productivity, and define the ultimate acceptance criteria for project closeout.
Walk-behind vs ride-on selection criteria
Machine selection hinges on the physical scale and logistical constraints of the jobsite, including ambient conditions, bleed-water behavior, joint layout, and column density. Walk-behind trowels are highly maneuverable and excel in confined spaces, complex topographies, or projects with strict budget limitations. In contrast, ride-on trowels are dual-rotor machines designed for massive, unobstructed pours, applying immense weight and dual-directional finishing power.
To compare these parameters, we look at the operational multipliers. A ride-on trowel machine boasts an operational efficiency typically 3 to 5 times greater than a walk-behind unit. In practical terms, a single ride-on machine can replace 3 to 4 walk-behind units on a large warehouse pour.
| Selection Criteria | Walk-Behind Trowel | Ride-On Trowel |
|---|---|---|
| Ideal Project Scale | Small to Medium, Edges | Large Commercial, Warehouses |
| Efficiency Rate | 100 - 200 m²/hr | 400 - 1,000 m²/hr |
| Operator Fatigue | Moderate to High | Low (Seated Operation) |
| Weight / Compaction | 34 - 125 kg (75 - 275 lb) | 300+ kg (660+ lb) |
Typically, crews deploy walk-behinds for edge work and tight corners, while ride-ons handle the vast center expanses. This creates an optimized equipment fleet that balances capital expenditure with aggressive pour schedules.
Productivity assumptions for jobsite planning
Accurate productivity assumptions are the bedrock of successful jobsite planning. Machinery must outpace the concrete's setting time across the entire poured area. If the equipment fleet is undersized, the concrete will reach its final set before finishing is complete.
As detailed in the selection criteria table, a standard walk-behind unit typically covers 100 to 200 square meters per hour (1,076 to 2,152 square feet per hour). When planning a 1,000 square meter (10,760 square feet) pour, a project manager must calculate the curing window—which might be 3 to 4 hours as a typical example, heavily dependent on ambient temperature and mix design. Operationally, this means scheduling at least three walk-behind units or one ride-on unit to comfortably complete the required passes before the final set. Proper operator training is also essential here; skilled operators can navigate edges and corners efficiently, maximizing the machine's effective coverage rate. Strict productivity planning eliminates cold joints and guarantees every square foot receives equal mechanical compaction.
Acceptance criteria before project closeout
Before a project can be officially closed out, the finished surface must undergo rigorous validation against established quality standards. Acceptance is based on measurable, objective data rather than subjective visual inspection.
Further reading:
Key Takeaways
- Use the trowel machine after bleed water disappears to reduce delamination risk and achieve a stronger surface finish.
- Treat troweling as mechanical surface compaction, not a substitute for chemical densifiers or liquid sealers.
- Select pan tools for initial floating and finishing blades for the final burnished surface.
- Avoid over-troweling because it can trap bleed water beneath the surface and cause blistering.
- Match the machine type to the job scale, using walk-behind units for controlled finishing and ride-on units for high-coverage industrial slabs.
Frequently Asked Questions
What does a concrete trowel machine do in floor densification?
It mechanically compacts and burnishes the fresh concrete surface, closing pores and improving abrasion resistance. It does not replace later chemical densifiers or sealers used for long-term surface protection.
When should operators start using a power trowel?
Operators should begin after bleed water has dissipated and the slab can support the machine without tearing. Starting too early can trap water and increase the risk of blistering or delamination.
What does dual-action mean for a trowel machine?
In this context, dual-action means the machine supports two finishing stages: pan-type tools for initial floating and blade-type tools for final finishing and burnishing.
Is a walk-behind power trowel suitable for commercial floors?
Yes. A walk-behind model, such as the MaxMach hand-push type concrete finishing power trowel, is practical for smaller commercial areas, edges, repair zones, and projects requiring precise operator control.
Can troweling increase the concrete slab’s compressive strength?
Not significantly. Troweling improves the surface layer by compacting and smoothing it, but the slab’s bulk compressive strength mainly depends on mix design, curing, and placement quality.