Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


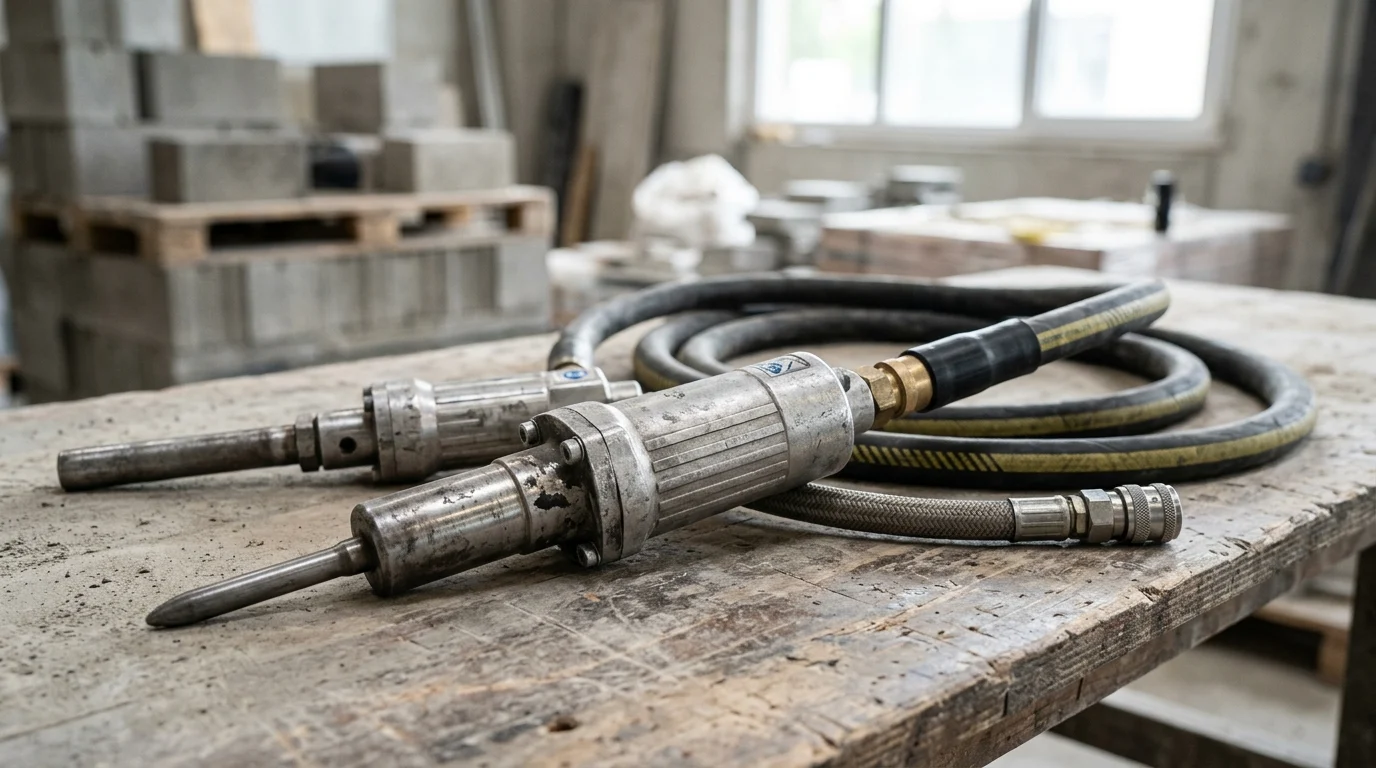
Air-powered vibration remains a workhorse on demanding concrete jobs because it solves two persistent site problems: trapped air and harsh operating conditions. In fresh concrete, even small voids can reduce strength, expose rebar, and create costly honeycombing.Pneumatic Concrete Vibrators use compressed air—typically around 85 to 100 psi—to generate high-frequency motion directly inside the vibrator head, helping concrete flow tightly around reinforcement and formwork. This article explains how the air-driven mechanism works, why it is valued on wet and heavy civil sites, what compressor support it requires, and how contractors can use it effectively for durable, well-compacted placements.
Why Pneumatic Concrete Vibrators Matter
Consolidation is a non-negotiable phase in concrete placement, directly dictating the structural integrity, durability, and surface finish of the cured element. Without adequate vibration, entrapped air voids and honeycombing severely compromise compressive strength and expose reinforcing steel to corrosive elements.
Among the various technologies deployed for internal consolidation, pneumatic concrete vibrators occupy a specialized and highly resilient tier. By leveraging compressed air rather than electrical current, these units provide reliable operation in the most demanding heavy civil and industrial construction environments.
What pneumatic concrete vibrators are
Pneumatic concrete vibrators, often referred to as air vibrators or pneumatic pokers, are internal consolidation tools driven entirely by compressed air. Unlike their electric or mechanical counterparts, which rely on external motors or high-frequency inverters, pneumatic units house a robust air-driven rotor directly within the vibrator head.
These tools require a continuous supply of compressed air, typically operating at a standard pressure band of 85 to 100 psi (approximately 6 to 7 bar). The absence of complex electronics or fragile mechanical flexible shafts makes them exceptionally durable, capable of withstanding rough handling, complete submersion, and highly abrasive concrete mixes.
Why air-powered vibration is still used
Despite the widespread adoption of high-frequency Electric Vibrators, air-powered vibration remains indispensable due to its inherent safety and thermodynamic advantages. Electric units, particularly those running on 115V or 230V, present distinct electrocution hazards in wet concrete environments if cables are compromised. Pneumatic systems eliminate this electrical risk entirely.
Furthermore, pneumatic vibrators do not suffer from thermal overload. While electric stators can quickly burn out if operated outside of the concrete (which normally acts as a heat sink), pneumatic vibrators are actively cooled by the expansion of exhaust air passing through the outer hose. This allows them to run continuously without overheating, reducing equipment mortality rates on high-volume pours.
Where pneumatic internal vibrators fit on site
The ideal setting for pneumatic internal vibrators involves sites where heavy-duty air compressors are already a staple of the logistics plan. They are predominantly found in mass concrete applications, such as hydroelectric dam construction, bridge pier casting, and heavy tunneling operations.
In these environments, contractors often deploy large towable compressors generating 185 CFM to over 400 CFM. Because these sites utilize compressed air for breakers, rock drills, and shotcrete pumps, integrating pneumatic vibrators requires no additional power infrastructure. Their ability to consolidate large volumes of harsh, low-slump concrete makes them the primary choice for heavy civil engineering rather than light commercial or residential flatwork.
How Pneumatic Concrete Vibrators Work
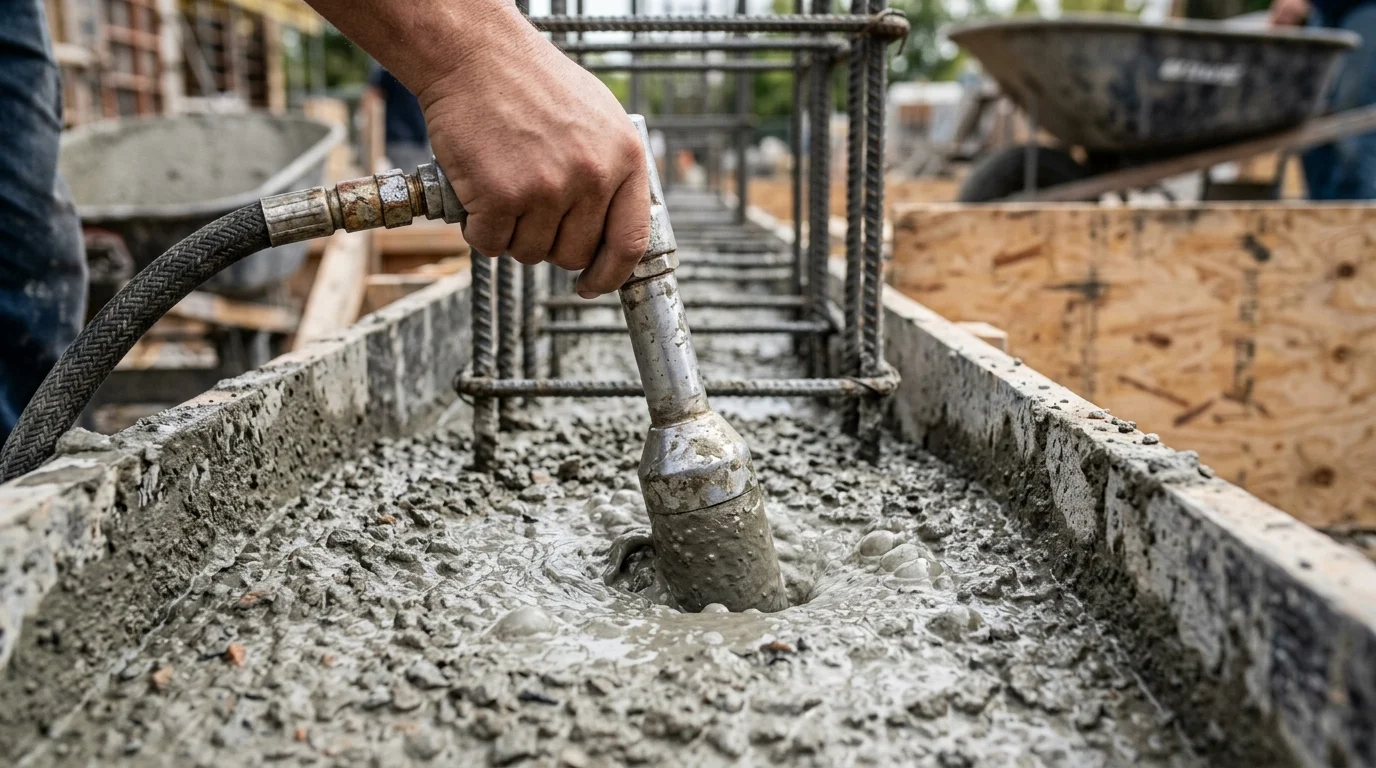
Understanding the mechanics of pneumatic consolidation requires examining how fluid power is converted into high-frequency mechanical energy. The efficiency of a pneumatic poker relies on a carefully engineered airflow path that generates the necessary centrifugal force to displace entrapped air from the concrete matrix.
How compressed air drives the vibrator head
The internal architecture of a pneumatic vibrator head relies on straightforward mechanical principles. Compressed air enters through a control valve at the operator's end and travels down a reinforced inner hose. Upon reaching the steel head, the pressurized air strikes a specialized rotor—often utilizing an eccentric mass or a turbine-vane mechanism.
As the air forces the rotor to spin, it generates rotational speeds typically ranging from 12,000 to 21,000 vibrations per minute (VPM). The centrifugal force created by the off-center mass causes the entire steel casing to oscillate rapidly. After driving the rotor, the depressurized exhaust air is forced back up through the annular space between the inner and outer hoses. It safely vents out at the operator's end (near the handle and control valve) to prevent injecting unwanted air into the concrete.
How frequency, amplitude, and head size affect consolidation
Effective consolidation relies on the interplay between frequency, amplitude, and the physical diameter of the vibrator head. High frequency (VPM) is primarily responsible for liquefying the mortar fraction of the concrete, reducing internal friction and allowing trapped air bubbles to rise. Amplitude—the maximum distance the vibrator head moves from its resting axis—provides the kinetic punch required to move heavy coarse aggregates into a dense matrix.
Head size dictates the radius of action and the overall volume of concrete consolidated per hour. A standard 55 mm (2.2-inch) pneumatic head typically offers a radius of action between 250 and 350 mm. However, this radius varies significantly based on the concrete slump; stiffer mixes restrict the radius, while higher slumps allow the vibratory waves to travel further.
| Vibrator Head Diameter | Typical Frequency (VPM) | Est. Radius of Action (mm)* | Consolidation Capacity (m³/hr)* |
|---|---|---|---|
| 35 mm (1.4 in) | 16,000 - 18,000 | 150 - 200 | Typically 5 - 12 |
| 55 mm (2.2 in) | 14,000 - 17,000 | 250 - 350 | Typically 15 - 25 |
| 75 mm (3.0 in) | 12,000 - 15,000 | 400 - 500 | Typically 25 - 40 |
| 150 mm (6.0 in) | 9,000 - 11,000 | 550 - 650 | Typically 40 - 65 |
*Note: Radius of action and capacity are highly dependent on concrete slump and mix design.
Which concrete mixes suit pneumatic vibration
Pneumatic vibrators excel in challenging mix designs that stall lesser equipment. They are particularly suited for low-slump, stiff concrete mixes (typically exhibiting a slump of less than 50 mm). These harsh mixes are common in slipform paving, precast elements, and roller-compacted concrete boundaries.
Because pneumatic units deliver high amplitude without the torque drop-off that some electric motors experience under heavy load, they can effectively fluidize dense mixes containing large-nominal-size aggregates (up to 150 mm aggregate in mass pours). Conversely, highly fluid self-consolidating concrete (SCC) requires no internal vibration, and using high-amplitude pneumatic tools on high-slump mixes risks severe aggregate segregation.
Pneumatic vs Electric Concrete Vibrators
Procurement managers and site engineers frequently weigh the merits of pneumatic systems against high-frequency electric vibrators. While both achieve the same ultimate goal of concrete consolidation, their operational profiles, infrastructure demands, and long-term economic footprints diverge significantly.
Key comparison criteria
When comparing pneumatic and electric vibrators, the primary evaluation criteria include power source availability, mechanical durability, operator ergonomics, safety in hazardous zones, and the total cost of ownership. The decision rarely hinges on the quality of consolidation, as properly sized units of either type will meet structural specifications.
Site logistics and physical demands often dictate the choice. Electric units require stable voltage and proximity to Generators or grid power, making them highly portable for spread-out commercial sites. Pneumatic units demand heavy, rigid air hoses and industrial compressors, anchoring them to sites where heavy air power is the baseline utility. Furthermore, pneumatic vibrators come with notable ergonomic disadvantages: their heavy hoses make them more fatiguing to operate, they produce higher levels of hand-arm vibration, and routing thick air lines requires more complex setup time.
Performance, cost, and maintenance differences
Performance-wise, pneumatic vibrators maintain consistent amplitude under heavy loads, whereas standard electric units may experience RPM drops if voltage sags over long extension cords. In terms of maintenance, pneumatic vibrators are exceptionally resilient. With proper inline lubrication, the lifespan of a pneumatic rotor can typically reach 3,000 to 5,000 operating hours. In contrast, standard electric vibrators with carbon brushes typically require brush replacement every 300 to 500 hours, and high-frequency inverters are vulnerable to electronic failure.
Financially, pneumatic systems present a higher operating cost due to the diesel fuel required to run a 185 CFM compressor compared to a small 5 kW generator. However, the capital expenditure replacement rate is much lower for pneumatics due to their rugged, burn-out-proof nature.
| Comparison Criteria | Pneumatic Concrete Vibrators | High-Frequency Electric Vibrators |
|---|---|---|
| Power Source | Towable/Industrial Air Compressor | Grid Power or Portable Generator |
| Overheating Risk | Zero (Air-cooled by exhaust) | High (If operated outside concrete) |
| Typical Lifespan | 3,000 - 5,000 hours (maintenance dependent) | 1,000 - 2,500 hours (inverter/motor) |
| Operating Cost | High (Compressor fuel consumption) | Low (Efficient electrical draw) |
| Safety Hazard | Hose whip, high noise, operator fatigue | Electrocution, short circuits |
When pneumatic vibrators outperform alternatives
Pneumatic vibrators objectively outperform electric alternatives in highly specific, extreme conditions. The first is in continuous mass pours where equipment duty cycles reach 100%. Because pneumatic units cannot overheat, operators can run them continuously for 24-hour slipform or dam placements without cycling them out to cool.
The second scenario involves hazardous or highly combustible environments. In underground mining, tunneling, or chemical plant construction, the sparking risk associated with electric motors is strictly prohibited. Pneumatic vibrators are intrinsically safe, making them the only viable internal consolidation method for explosive-rated (EX) zones.
Setup, Operation, and Maintenance
Deploying pneumatic concrete vibrators requires strict adherence to fluid dynamic principles and best practices in concrete placement. Improper setup restricts airflow, starving the vibrator of the CFM required to reach optimal frequency, while poor operational technique can lead to structural defects.
Compressor capacity, hoses, couplings, and lubrication
The foundation of pneumatic operation is matching the compressor capacity to the tool's consumption rate. A standard 55 mm pneumatic vibrator consumes between 35 and 45 CFM of air at 90 psi. Running multiple pokers simultaneously requires calculating the aggregate CFM and ensuring the compressor can deliver that volume without pressure drops. Hoses must be sized correctly; using an undersized supply hose creates friction loss, severely reducing the vibrator's VPM.
Equally critical is the use of an inline lubricator. The internal rotor spins at up to 21,000 RPM and relies entirely on oil mist carried by the compressed air for lubrication. The inline oiler should be calibrated to deliver approximately 1 to 2 drops of specialized pneumatic tool oil per minute. Running a pneumatic poker dry will cause catastrophic friction failure of the rotor and vanes within hours.
Insertion spacing, depth, and withdrawal technique
The technique for using a pneumatic vibrator mirrors standard internal consolidation rules but requires managing the heavier, stiffer air hoses. The vibrator head must be inserted rapidly and vertically under its own weight. Angled insertions can push the top layer of concrete laterally and damage the reinforcing cage.
The head should penetrate the current concrete lift and extend approximately 150 mm (6 inches) into the underlying, previously placed lift to eliminate cold joints. The operator must hold the vibrator in place for 5 to 15 seconds until the surface takes on a localized sheen and large air bubbles cease escaping. Withdrawal must be deliberately slow—roughly 25 mm (1 inch) per second—allowing the fluid concrete to collapse and fill the void left by the vibrating head.
Noise, air quality, hose safety, and routine maintenance
Safety and maintenance protocols for pneumatic systems center on air pressure management and noise mitigation. Pneumatic vibrators are inherently loud, often generating noise levels exceeding 90 dB(A) at the operator's ear due to the mechanical impact and exhaust air. Mandatory double hearing protection is required on most sites.
Routine maintenance involves inspecting the outer exhaust hose for abrasions, as a rupture will vent high-pressure air and concrete slurry unpredictably. Couplings, typically heavy-duty claw-style or Chicago fittings, must be secured with whip checks to prevent lethal hose whipping in the event of a disconnection. Post-pour maintenance is minimal but vital: the exterior must be pressure-washed before concrete cures, and a brief burst of air should be run through the system to clear any moisture condensation from the internal lines before storage.
How to Choose a Pneumatic Concrete Vibrator
Specifying the correct pneumatic concrete vibrator is an exercise in matching mechanical output to structural geometry. Over-sizing the vibrator can lead to rebar damage and formwork blowouts, while under-sizing results in honeycombing and rejected elements.
Selection factors for element geometry and site conditions
The primary geometric constraint when selecting a vibrator is the density of the reinforcing steel (rebar). As a strict operational rule, the diameter of the vibrator head must be small enough to pass through the rebar grid without wedging. The clearance between the vibrating head and the rebar should be at least 1.5 times the maximum aggregate size used in the mix. For example, if a mix contains 40 mm aggregate, the clearance space must be at least 60 mm.
Environmental and site conditions also dictate equipment viability. Pneumatic vibrators perform poorly in freezing conditions where moisture in the air lines can ice up and block valves. Additionally, their efficiency drops at high altitudes due to reduced air density, which lowers the compressor's effective CFM output. When selecting hose lengths, standard pneumatic whips range from 2 to 6 meters. While deep wall pours require longer whips, engineers must account for the pressure drop over extended hoses. For exceptionally deep elements, rigid extension tubes can be fitted, though these reduce operator maneuverability.
Lifecycle cost, spare parts, and service support
While the initial purchase price of a pneumatic poker is generally competitive, lifecycle costs depend heavily on the availability of spare parts and serviceability. The outer rubber hose, which drags across abrasive rebar and concrete, is the most frequently replaced component. Procurement should prioritize models that allow for field-replacement of the outer hose without requiring specialized factory crimping tools.
Service support is another critical factor. Because the internal rotor operates at extreme speeds, the wear parts—specifically the steel vanes or eccentric bearings—will eventually require replacement. Selecting equipment from established manufacturers ensures that rebuild kits are readily available, allowing a site mechanic to refurbish a stalled vibrator in under an hour rather than scrapping the entire unit.
Final decision checklist
To finalize the selection of a pneumatic concrete vibrator, project managers should apply specific operational thresholds rather than relying on guesswork:
- Compressor Sizing: Ensure the site compressor provides a minimum buffer of 20% excess CFM above the combined requirement of all connected pneumatic tools. For example, running two 40 CFM vibrators requires a compressor rated for at least 96 CFM.
- Rebar Clearance: If the minimum rebar spacing is 100 mm, select a vibrator head diameter no larger than 65 mm to ensure the required clearance (1.5 times the maximum aggregate size for a standard mix).
- Insertion Grid: Establish the insertion spacing grid based on the concrete slump and head size. Overlap the radius of action by 1.5 times to prevent unconsolidated gaps between insertion points.
- Infrastructure Compatibility: Standardize air couplings (e.g., universal claw fittings) across all tools to match the site's existing pneumatic infrastructure, minimizing setup delays and maximizing the efficiency of the concrete consolidation phase.
Key Takeaways
- Use pneumatic concrete vibrators when site conditions are wet, abrasive, or electrically hazardous, because compressed air eliminates the need for live electrical power at the vibrator head.
- Maintain the air supply within the typical 85 to 100 psi operating band to keep vibration frequency stable and achieve reliable consolidation.
- Match compressor capacity to the number and size of vibrator heads, especially on heavy civil pours where 185 CFM to 400+ CFM compressors may already be available.
- Select pneumatic internal vibrators for mass concrete, bridge piers, dams, tunneling, and harsh low-slump mixes where durability and continuous operation are critical.
- Avoid relying on vibration to fix poor placement practices; insert the poker methodically so entrapped air escapes and honeycombing around reinforcement is minimized.
Frequently Asked Questions
What air pressure do pneumatic concrete vibrators typically require?
Most pneumatic concrete vibrators operate in the 85 to 100 psi range, or about 6 to 7 bar. Always match the compressor output, hose size, and vibrator head requirements to maintain consistent frequency and compaction performance.
How does compressed air improve concrete compaction?
Compressed air spins a rotor inside the vibrator head, creating high-frequency vibration. This energy liquefies the fresh concrete momentarily, helping trapped air rise out and allowing aggregates, cement paste, and reinforcement zones to consolidate more densely.
Why use pneumatic vibrators instead of electric models on site?
Pneumatic vibrators remove electrical shock risks in wet concrete environments and are less vulnerable to overheating. They are especially practical on heavy civil sites where compressors already power breakers, drills, pumps, or other air tools.
Where are pneumatic internal vibrators most useful?
They are best suited for demanding pours such as bridge piers, dams, tunnels, foundations, and mass concrete work. These jobs often involve harsh mixes, long operating hours, and large compressors that can support continuous air-powered vibration.
Can a pneumatic concrete vibrator run continuously?
Pneumatic vibrators tolerate continuous operation better than many electric units because exhaust air helps cool the head and hose. However, operators should still avoid unnecessary dry running to reduce wear and preserve service life.