Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


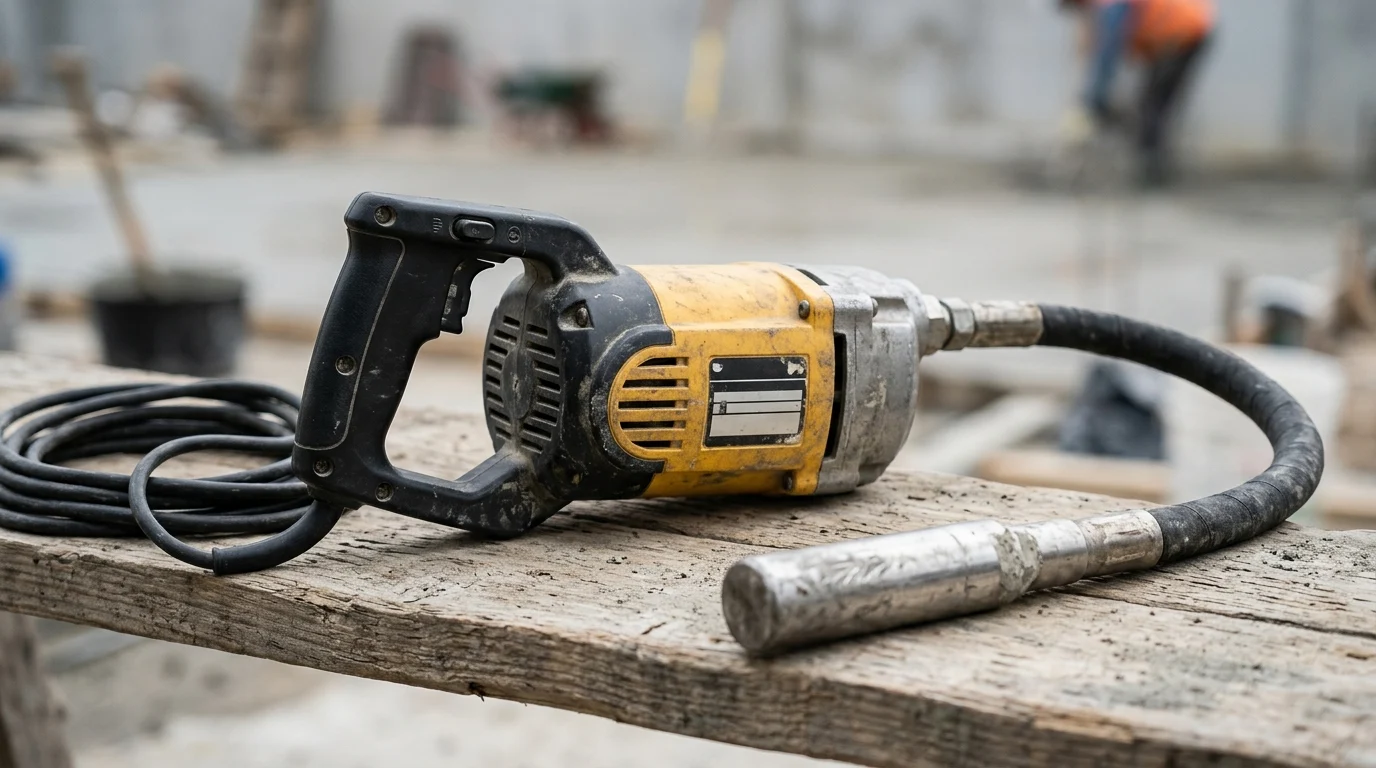
Concrete strength is won or lost during consolidation.Even a well-designed mix can underperform if trapped air, aggregate bridging, or poor flow leaves hidden voids inside the formwork. Eccentric Concrete Vibrators solve this problem by converting the rotation of an off-center mass into high-frequency force that temporarily fluidizes fresh concrete, allowing air to escape and aggregates to pack densely around reinforcement. This article explains the mechanics behind that vibration force, why frequency and amplitude matter, how proper consolidation reduces honeycombing, and how to choose suitable vibrator heads for demanding site conditions. For contractors and equipment buyers, understanding these principles leads directly to stronger, more durable concrete and fewer costly defects.
Strategic Value of Eccentric Concrete Vibrators
Achieving maximum density and structural integrity in cast-in-place concrete relies heavily on mechanical consolidation. Freshly mixed concrete behaves as a Bingham plastic; it possesses a yield stress that must be overcome before it can flow. When deposited into formwork, internal friction between aggregate particles and the high viscosity of the cement paste trap significant volumes of air. Without mechanical intervention, uncompacted concrete can retain up to 20% entrapped air by volume.
The strategic value of eccentric concrete vibratorslies in their ability to dynamically alter the rheology of the concrete mix. By introducing high-frequency mechanical waves, these devices temporarily overcome the mixture's yield stress, inducing a state of thixotropy where the concrete behaves as a viscous fluid. This fluidization allows gravity to pull the heavier aggregate particles downward into a dense matrix, while the lighter entrapped air bubbles are forced to the surface. Since every 1% of retained entrapped air reduces the final compressive strength of the concrete by approximately 5%, deploying highly efficient Eccentric Vibrators is a critical risk-mitigation strategy in structural engineering.
How vibration quality reduces honeycombing
Honeycombing occurs when coarse aggregates bridge together, leaving large macroscopic voids unfilled by mortar. This defect severely compromises the load-bearing capacity of the element and exposes reinforcing steel to corrosive environmental factors. The eccentric vibrator directly combats this by producing radial compression waves that break the friction between aggregate particles. As the mortar fluidizes, it flows seamlessly into the interstitial spaces between the coarse aggregates and tightly against the formwork.
The quality of this vibration dictates the uniformity of the final matrix. An eccentric vibrator operating at the correct frequency and amplitude ensures that the mortar is sufficiently liquefied without causing aggregate segregation. Segregation—where heavy aggregates sink to the bottom and excess water and cement paste rise to the top—is a common consequence of over-vibration or incorrect equipment specifications. By matching the vibrator's centrifugal output to the mix design's specific slump and aggregate size, contractors can achieve a homogeneous consolidation that virtually eliminates honeycombing and significantly reduces the permeability of the cured structure.
Where eccentric vibrators fit in concrete placement
Eccentric vibrators, commonly referred to as internal or poker vibrators, are the primary consolidation tool for the vast majority of cast-in-place applications. Their design allows them to be submerged directly into the fresh concrete mass, delivering kinetic energy precisely where it is needed. This direct-contact method is highly efficient, making it the standard approach for deep structural elements such as foundation footings, columns, retaining walls, and heavily reinforced transfer slabs.
In highly congested rebar environments, where the distance between steel bars may be less than 2.5 inches,specialized micro-eccentric vibrators become indispensable. The ability to swap vibrator heads of varying diameters ensures that the equipment can be tailored to the exact spatial constraints of the pour. Unlike external form vibrators, which require rigid, heavy-duty formwork to withstand the transferred energy, internal eccentric vibrators apply force directly to the concrete, making them adaptable to almost any conventional formwork system.
Key Components and Performance Parameters
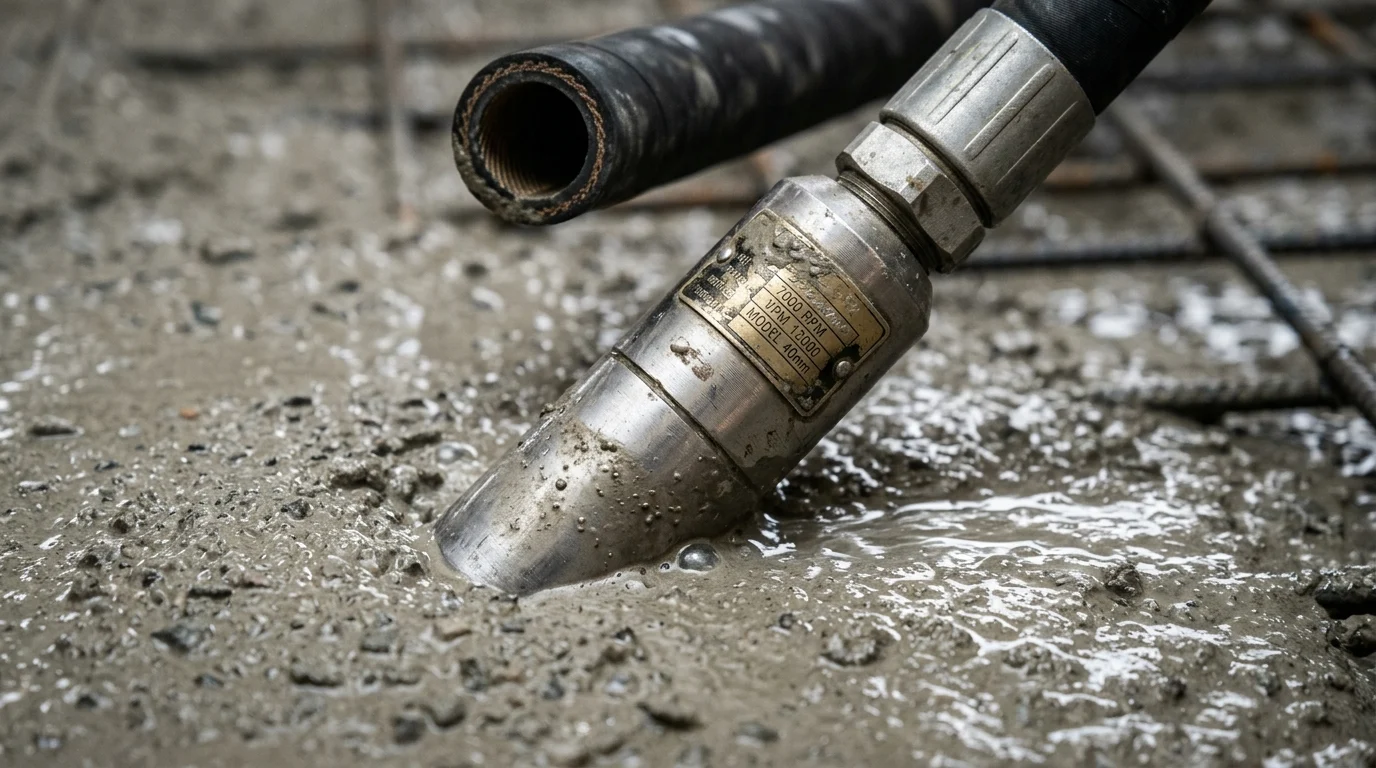
The effectiveness of an eccentric concrete vibrator is determined by the precise interaction of its mechanical components and its operational parameters. Understanding these variables is essential for specifying the correct equipment for a given mix design, particularly when dealing with low-slump, high-strength concrete formulations that require immense energy to fluidize.
What an eccentric concrete vibrator is
An eccentric concrete vibrator is an internal consolidation tool consisting of three primary components: a prime mover (motor), a flexible drive shaft, and a vibrating head. The prime mover, which can be powered by electricity, gasoline, or compressed air, generates rotational kinetic energy. This rotation is transmitted through the flexible shaft—a core of wound high-tensile steel wire encased in a durable rubber and steel-braid casing—down to the vibrating head.
Inside the sealed steel cylinder of the vibrating head lies the eccentric mechanism. This consists of an unbalanced weight, or an off-center mass, attached to the rotating shaft. As the shaft spins at high speeds, the asymmetric mass forces the entire steel casing to oscillate violently. This continuous, rapid oscillation generates the mechanical waves that are transferred into the surrounding fresh concrete.
Core variables: frequency, amplitude, and centrifugal force
The performance profile of an eccentric vibrator is defined by three interrelated core variables: frequency, amplitude, and centrifugal force. Frequency, measured in vibrations per minute (vpm), dictates how rapidly the kinetic waves are emitted. Most modern eccentric vibrators operate between 10,000 and 17,000 vpm. High frequencies are critical for liquefying the cement paste and moving smaller aggregate particles.
Amplitude represents the maximum distance the vibrator head deviates from its resting axis during one oscillation cycle. Typically ranging from 0.04 to 0.10 inches, amplitude determines the physical punch or "kick" of the vibrator, which is necessary for moving large coarse aggregates. Centrifugal force is the outward force generated by the spinning eccentric mass, calculated using the mass, the radius of eccentricity, and the square of the rotational speed. Ranging from 150 lbs in micro-heads to over 4,000 lbs in massive dam-pouring vibrators, centrifugal force dictates the overall radius of action and the speed of consolidation.
How to compare motor power, speed, and head size
Selecting the optimal vibrator requires balancing motor power, rotational speed, and head size against the concrete mix and formwork geometry. A more powerful motor is required to maintain high vpm when a larger head is submerged in stiff, low-slump concrete. If the motor is underpowered, the resistance of the concrete will cause the frequency to drop significantly, resulting in inadequate fluidization.
Head size directly correlates with the radius of action—the cylindrical zone of concrete effectively consolidated around the inserted vibrator. According to American Concrete Institute (ACI) 309R guidelines, vibrators are categorized into groups based on head diameter, which informs the expected compaction rate. Contractors must select a head size large enough to maximize placement rates but small enough to navigate the reinforcing steel without becoming entangled.
| ACI 309R Group | Head Diameter (in) | Typical Frequency (vpm) | Radius of Action (in) | Concrete Placement Rate (cu yd/hr) |
|---|---|---|---|---|
| Group 1 | 0.75 - 1.50 | 10,000 - 15,000 | 3 - 6 | 1 - 5 |
| Group 2 | 1.25 - 2.50 | 9,000 - 13,500 | 5 - 10 | 3 - 10 |
| Group 3 | 2.00 - 3.50 | 8,000 - 12,000 | 7 - 14 | 6 - 20 |
| Group 4 | 3.00 - 6.00 | 7,000 - 10,500 | 12 - 20 | 15 - 40 |
How Eccentric Vibration Works in Concrete
The physical process of consolidating concrete via eccentric vibration relies on the efficient transfer of kinetic energy from a mechanical source into a heterogeneous fluid mixture. Mastering this energy transfer is what allows structural engineers to specify concrete with lower water-to-cement ratios, knowing that mechanical consolidation will compensate for the reduced natural workability.
How off-center mass creates vibration force
Because the force increases with the square of the angular velocity, minor increases in the motor's RPM yield substantial increases in vibrational energy. When the motor drives the flexible shaft at 12,000 RPM, the eccentric weight spins 200 times per second. The asymmetrical nature of this spinning mass forces the vibrator's outer casing to orbit its own central axis, creating a high-energy whipping motion that aggressively impacts the surrounding concrete.
How force transfers through the vibrator head
The transfer of this eccentric force into the concrete is mediated entirely by the vibrator's steel casing. As the casing oscillates, it acts as a transducer, converting the rotational kinetic energy into longitudinal compression waves that radiate outward into the concrete matrix. These stress waves propagate through the aggregate structure, rapidly alternating between compression and tension.
This rapid cycling breaks the cohesive and adhesive bonds within the cement paste and overcomes the internal friction of the aggregates. The effective transmission of this force requires the vibrator head to remain in firm, direct contact with the concrete. As the casing wears down over time from the highly abrasive concrete environment, its mass decreases, which subtly alters the amplitude. Industry standards dictate that a vibrator head should be replaced when its diameter has been reduced by 10% to 15%, as the loss of mass severely degrades the force transfer efficiency.
Best practices for insertion depth, spacing, and timing
To achieve a homogeneous concrete matrix, operators must follow strict spatial and temporal protocols. The vibrator must be inserted rapidly and completely vertically under its own weight. Rapid insertion prevents the premature compaction of the upper layers, which could trap air in the lower layers. The distance between insertion points should be approximately 1.5 times the established radius of action, ensuring a visual overlap of the fluidization zones.
Depth control is equally critical when pouring in multiple lifts. The vibrator head must penetrate 6 inches (150 mm) into the previously placed, still-plastic lift. This intermingling of the layers prevents the formation of cold joints, seamlessly knitting the lifts into a monolithic structural element.
Timing dictates the quality of the finish and the final strength. The vibrator should be held stationary at the bottom of the insertion for 5 to 15 seconds. The operator must watch the surface; consolidation is complete when the concrete surface takes on a glistening sheen, coarse aggregates blend into the surface, and large trapped air bubbles stop escaping. Finally, the withdrawal must be slow and deliberate—ideally at a rate of 1 inch per second (25 mm/s)—allowing the fluidized concrete to flow back together and fill the void left by the exiting vibrator head.
Comparison with Other Concrete Vibration Methods
While internal eccentric vibrators are the default choice for the majority of concrete placement tasks, they are part of a broader ecosystem of consolidation technologies. Evaluating eccentric mechanisms against external, surface, and pneumatic alternatives clarifies their specific operational advantages and limitations in complex structural scenarios.
Eccentric vibrators vs
. internal, external, and surface vibrators
Eccentric internal vibrators are designed for direct submersion, providing localized, highly efficient energy transfer. In contrast, external vibrators (also known as form vibrators) are bolted directly to the exterior of the formwork. They consolidate the concrete by vibrating the entire form structure, which requires heavily reinforced steel or timber forms to withstand the intense, distributed energy without failing.
Surface vibrators, such as vibrating screeds or truss screeds, operate exclusively on the top layer of poured concrete. They utilize a spinning eccentric weight mounted on a flat metal beam to consolidate and level the concrete simultaneously. Pneumatic internal vibrators, while still functioning internally, use compressed air to drive an air motor in the head rather than relying on a flexible shaft, making them ideal for ultra-heavy-duty continuous pours like dams, but less practical for standard commercial sites due to the need for massive air compressors.
Trade-offs in compaction depth, speed, and finish quality
The choice between these methods involves strict trade-offs. Internal eccentric vibrators offer unmatched compaction depth; a standard flexible shaft can reach depths of 20 feet or more in columns and walls. However, they rely heavily on the operator's skill to ensure uniform coverage without leaving un-vibrated pockets. Surface vibrators provide exceptional speed and finish quality for large flatwork areas but are physically limited to an effective compaction depth of 6 to 8 inches (150-200 mm).
External form vibrators excel at producing superior, void-free architectural finishes on the exterior faces of the concrete, as the vibration originates at the formwork interface. However, their effective depth inward from the form is limited, often requiring supplementary internal vibration for walls thicker than 12 inches. External systems also represent a significantly higher setup cost and require precise engineering to ensure the forms are not destroyed by the resonant frequencies.
| Vibration Method | Primary Application | Effective Compaction Depth | Setup Time / Cost | Finish Quality on Formed Faces |
|---|---|---|---|---|
| Internal Eccentric | Columns, walls, beams, deep slabs | Unlimited (limited only by shaft length) | Low | Good (depends on insertion proximity) |
| External (Form) | Precast, architectural concrete, tunnels | 12 - 18 inches inward from form | High | Excellent (minimizes bugholes) |
| Surface (Screed) | Flatwork, pavements, bridge decks | 6 - 8 inches downward | Medium | N/A (finishes top surface) |
| Pneumatic Internal | Mass concrete (dams, thick mats) | Unlimited | High (requires heavy compressors) | Good |
Compliance and quality-control considerations
From a compliance perspective, the American Concrete Institute’s ACI 309R "Guide for Consolidation of Concrete" dictates the acceptable parameters for all vibration methods. Quality control inspectors heavily scrutinize the choice of vibrator to ensure it aligns with the mix design's slump and maximum aggregate size. For instance, using a surface screed alone on a 10-inch thick slab violates standard compliance, as the bottom 2-4 inches will remain unconsolidated, leading to structural weakness.
When deploying eccentric internal vibrators, quality control teams monitor the frequency of the units under load. A vibrator that operates at 12,000 vpm in the air but drops to 8,000 vpm when submerged indicates an underpowered motor, which risks non-compliance due to incomplete consolidation. Regular tachometer testing of vibrators on site is a mandatory quality-control practice on highly regulated commercial and infrastructure projects.
Selection, Operation, and Maintenance Guidance
The longevity of structural concrete is intrinsically linked to the equipment used during its placement. For contractors, the selection, operation, and maintenance of eccentric concrete vibrators are not merely logistical details, but critical factors that influence labor efficiency, mitigate rework, and ensure long-term structural viability.
How contractors should choose the right vibrator
Selecting the correct eccentric vibrator requires a rigorous assessment of the concrete mix and the formwork geometry. The cardinal rule of sizing is that the vibrator head diameter must be 0.75 to 1.0 inch smaller than the narrowest gap between the reinforcing steel bars. If the head is too large, it will wedge against the rebar, potentially damaging the epoxy coating on the steel and failing to reach the bottom of the form.
Contractors must also match the vibrator's frequency and amplitude to the workability of the concrete. High-slump, highly fluid mixtures require smaller, higher-frequency vibrators to release entrapped air without causing the heavy aggregates to sink rapidly. Conversely, low-slump, stiff concrete (such as that used in slip-form paving) demands large-diameter heads with high amplitude to physically force the coarse aggregates into alignment. Mismatching the equipment—such as using a low-amplitude micro-head in a stiff mix—will result in massive labor overruns and inevitable honeycombing.
Inspection and maintenance practices
Eccentric vibrators operate in one of the most hostile environments in construction, subjected to high temperatures, continuous abrasion, and highly alkaline cement paste. Preventive maintenance is critical to avoiding catastrophic equipment failure mid-pour. For electric-driven units, contractors must inspect the carbon brushes every 50 operating hours; worn brushes will cause arcing, power loss, and eventual motor burnout.
The flexible shaft and vibrating head require equally stringent oversight. The core of the flexible shaft must be re-lubricated with a high-temperature, non-separating grease every 100 hours of operation to prevent friction-induced snapping. Furthermore, maintenance personnel must regularly measure the diameter of the vibrating head with calipers. A head that has lost 10% of its original diameter due to concrete abrasion will suffer a drastic reduction in centrifugal force output, necessitating immediate replacement of the casing.
When an eccentric concrete vibrator is the best choice
The eccentric concrete vibrator remains the most versatile and economically viable choice for over 80% of standard cast-in-place operations. Its portability, scalability, and direct-contact efficiency make it the definitive tool for consolidating deep structural elements, congested rebar cages, and standard foundational work.
When contractors face tight project schedules, strict structural density requirements, and complex formwork geometries, the internal eccentric vibrator provides the necessary operational flexibility. By combining rigorous equipment selection protocols with disciplined insertion techniques and proactive maintenance, construction teams can leverage eccentric vibration to consistently deliver dense, durable, and structurally sound concrete elements.
Key Takeaways
- Use eccentric concrete vibrators to overcome fresh concrete’s yield stress and release trapped air before the mix begins to stiffen.
- Treat entrapped air as a structural risk because uncompacted concrete can retain up to 20% air by volume.
- Control consolidation carefully because every 1% of retained entrapped air can reduce final compressive strength by about 5%.
- Match vibrator frequency, amplitude, and head diameter to slump, aggregate size, member geometry, and reinforcement spacing to prevent honeycombing and segregation.
- Use smaller or micro-eccentric vibrator heads when rebar spacing is below about 2.5 inches or access is limited.
- Avoid over-vibration because excessive energy can separate coarse aggregate from paste and reduce concrete uniformity.
Frequently Asked Questions
How does an eccentric concrete vibrator create vibration?
It uses an off-center rotating mass inside the vibrator head. As the mass spins, it generates centrifugal force that produces rapid radial vibration, temporarily fluidizing fresh concrete so trapped air can rise and aggregates can settle into a denser matrix.
Why is vibration important in concrete compaction?
Fresh concrete can trap significant air and resist flow. Proper vibration overcomes internal friction, reduces voids and honeycombing, improves contact around rebar, and helps achieve higher density, strength, and durability in the cured structure.
What happens if concrete is not vibrated enough?
Under-vibration can leave entrapped air, rock pockets, honeycombing, weak zones, and poor bonding around reinforcement. These defects increase permeability and may reduce load-bearing performance, especially in columns, walls, foundations, and heavily reinforced members.
Can over-vibration damage concrete quality?
Yes. Excessive vibration can cause segregation, where coarse aggregate sinks and water or cement paste rises. The result may be a non-uniform concrete matrix with reduced surface quality, inconsistent strength, and higher risk of durability problems.
Where are eccentric concrete vibrators commonly used?
They are widely used in cast-in-place concrete work such as foundations, columns, retaining walls, slabs, beams, and reinforced structural elements. Internal poker-type vibrators are especially effective because they deliver vibration directly inside the fresh concrete.