Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


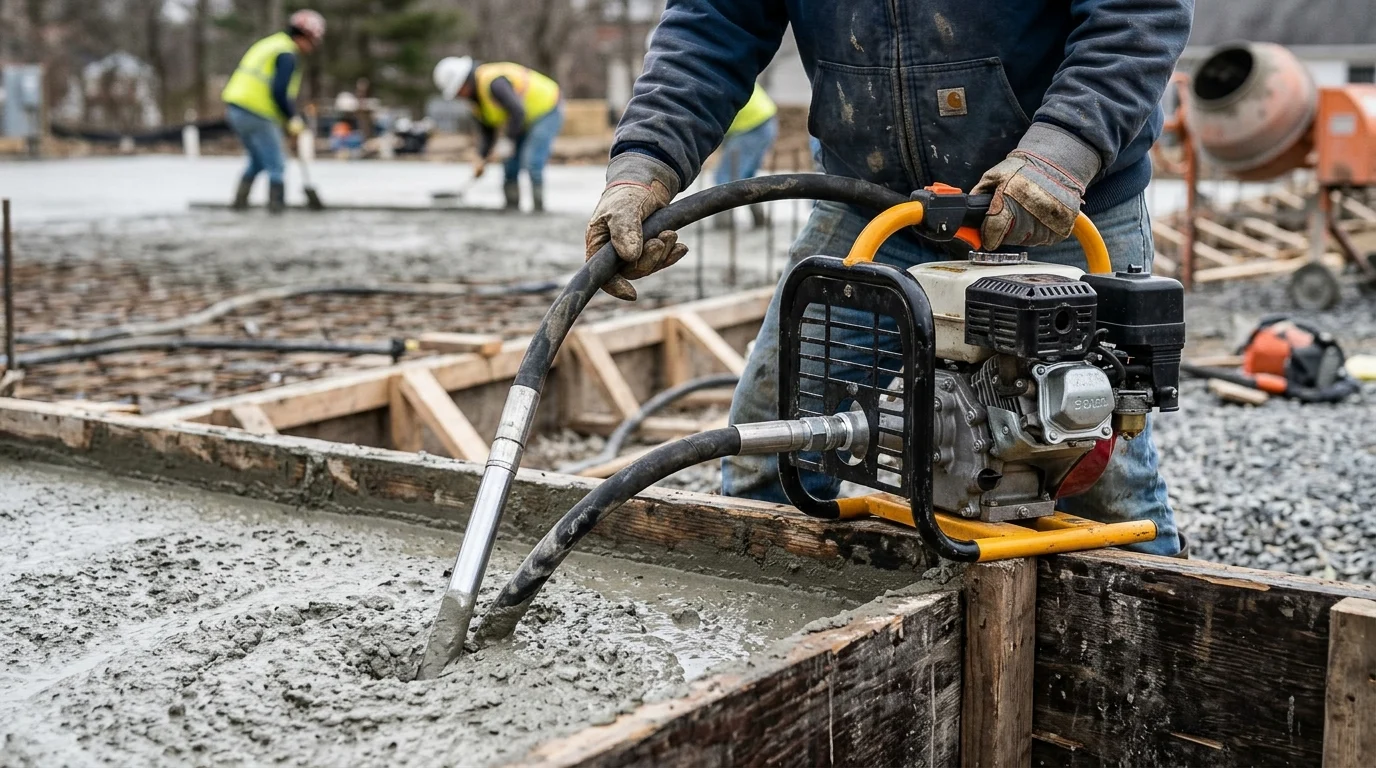
Even a well-designed concrete mix can fail in the field if it is not consolidated correctly. Fresh concrete may contain 5% to 20% entrapped air, and those hidden voids can reduce strength, increase permeability, expose reinforcement to corrosion, and create visible defects such as honeycombing or bug holes. Choosing the right vibrator is therefore not just an equipment decision—it is a quality-control decision. This guide explains how vibrator type, frequency, amplitude, concrete slump, aggregate characteristics, and placement conditions work together, helping contractors match the tool to the pour and avoid both under-vibration and over-vibration.
Why Concrete Vibrator Selection Matters
Consolidation represents a critical phase in concrete placement, directly dictating the structural integrity, durability, and aesthetic finish of the final element. Freshly poured concrete naturally contains a significant volume of entrapped air—typically ranging from 5% to 20% by volume depending on the mix design and placement method. Without active consolidation, this entrapped air forms voids that compromise the density and strength of the matrix.
Mechanical vibration remains the most efficient and widely specified method for concrete consolidation. By transmitting high-frequency impulses into the fresh concrete, vibrators temporarily reduce internal friction between aggregate particles. This fluidization allows the concrete to settle under the influence of gravity, displacing entrapped air pockets which then rise to the surface. Selecting the precise vibration equipment for a specific pour is not a generic process; it requires an engineering assessment of the mix characteristics, structural geometry, and ambient site conditions.
How vibration protects concrete placement quality
The primary mechanical function of vibration is to transition the concrete from a plastic state into a temporary liquid state. When a vibrator operates at the correct frequency and amplitude, it breaks the surface tension of the cement paste and forces the coarse aggregate into a tighter, interlocking matrix. This process effectively drives out macroscopic air voids.
Achieving optimal density through this method can increase the final compressive strength of the concrete by up to 30% compared to unvibrated or poorly consolidated placements. Furthermore, eliminating internal voids dramatically decreases the permeability of the concrete, offering superior protection to embedded steel reinforcement against chloride ingress and subsequent corrosion.
Common defects caused by poor vibrator selection
Applying the wrong type of vibrator—or using inadequate specifications—routinely leads to severe structural and cosmetic defects. Honeycombing occurs when coarse aggregate clusters together without sufficient mortar to fill the interstitial spaces, a direct result of undersized vibrators failing to fluidize the mix adequately. Conversely, over-vibration with an oversized unit can cause segregation, driving heavy aggregates to the bottom of the formwork while bringing weak cement paste and water to the surface.
Surface blemishes, commonly known as bug holes, proliferate when the vibrator's amplitude is insufficient to drive entrapped air away from the formwork face. Internally, inadequate consolidation can result in a loss of up to 50% of the mechanical bond strength between the concrete matrix and the reinforcing steel, creating hidden structural vulnerabilities.
Key factors that affect consolidation results
Several physical and environmental variables dictate how effectively a vibrator will consolidate a given pour. The concrete slump is the most critical mix-related factor; a stiff mix with a 1-inch to 2-inch slump demands high-amplitude vibration to overcome internal friction, whereas a highly fluid 6-inch slump mix requires minimal, lower-energy vibration to prevent segregation.
Aggregate size and shape also play a role. Angular, crushed stone aggregates lock together more aggressively than smooth river rock, requiring longer vibration cycles or higher frequencies to achieve proper settlement. Finally, the density of the reinforcement layout acts as a physical barrier to the vibrator's radius of action, absorbing energy and necessitating adjustments to both the equipment size and the insertion pattern.
Choose the Right Concrete Vibrator Type
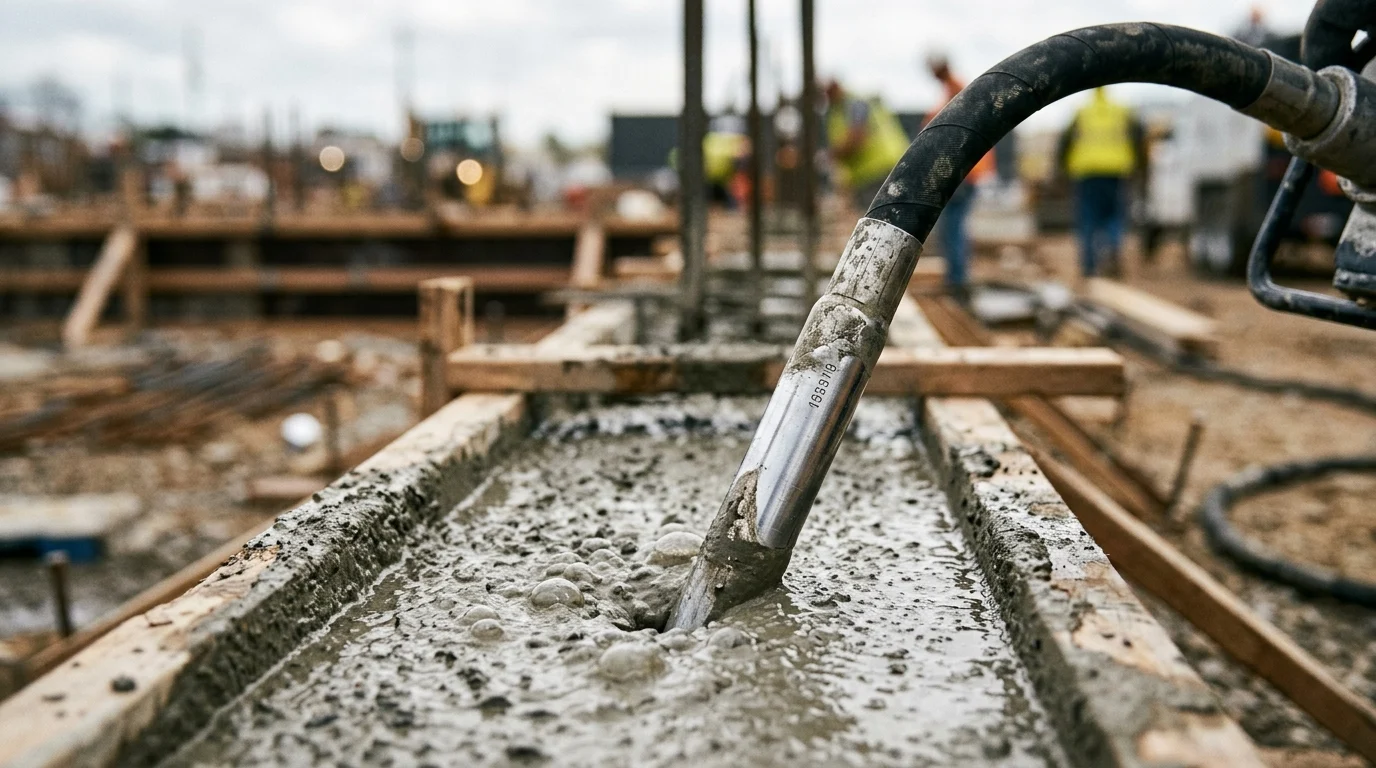
Matching the vibrator category to the specific structural application is the first step in equipment selection. Construction projects utilize three primary classes of concrete vibrators: internal (poker or spud), surface, and formwork (external) vibrators. Each category is engineered to deliver kinetic energy through different mediums, and utilizing the incorrect category can render the consolidation process entirely ineffective.
When to use an internal concrete vibrator
Internal vibrators, often referred to as poker or spud vibrators, are the industry standard for approximately 90% of structural concrete placements. These units consist of a vibrating head immersed directly into the fresh concrete, transmitting energy radially outward. They are the mandatory choice for structural elements with significant depth, including foundation walls, columns, footings, and heavily reinforced beams.
Because the energy is applied directly into the mass of the concrete, internal vibrators offer the highest efficiency for deep consolidation. They are capable of penetrating multiple lifts of concrete, ensuring that newly placed layers are seamlessly knitted into the previously placed, still-plastic layers below, thereby preventing cold joints.
When to use a surface concrete vibrator
Surface vibrators apply energy directly to the top surface of the poured concrete. This category includes vibrating screeds, pan vibrators, and roller screeds. They are exclusively deployed for flatwork applications where the depth of the concrete is relatively shallow.
As a strict industry guideline, surface vibrators are only effective for consolidating slabs up to 8 inches (200 mm) in thickness. If the slab exceeds this depth, the kinetic energy dissipates before reaching the bottom of the pour, leaving the lower strata unconsolidated. For slabs thicker than 8 inches, an internal vibrator must be used ahead of the surface screed to ensure full-depth compaction.
How formwork and placement method affect vibrator choice
When structural geometries or extreme reinforcement congestion prevent the insertion of an internal poker, formwork vibrators become necessary. These external units bolt directly to the outside of the formwork, vibrating the entire mold to consolidate the enclosed concrete. This method requires highly robust, engineered formwork—typically steel or reinforced timber—capable of withstanding continuous dynamic loads ranging from 3,000 to 10,000 vibrations per minute (VPM) without fatiguing or blowing out.
| Vibrator Category | Primary Application | Effective Depth/Thickness | Typical Frequency (VPM) |
|---|---|---|---|
| Internal (Poker) | Walls, columns, deep slabs | Unlimited (depends on shaft) | 10,000 - 17,000 |
| Surface (Screed) | Flatwork, pavements | Up to 8 inches (200 mm) | 3,000 - 6,000 |
| Formwork (External) | Highly congested walls | 12 to 18 inches inward | 3,000 - 10,000 |
The placement method also dictates external vibrator deployment. In pumped concrete applications, particularly self-consolidating concrete (SCC) or tunnel linings where access is sealed, external vibration guarantees that the material flows into every architectural detail without requiring manual access to the wet mix.
Compare Key Concrete Vibrator Specifications
Once the correct category is established, contractors must evaluate the technical specifications of the vibrator to ensure it matches the production rates and physical constraints of the site. The performance of an internal vibrator is governed by a combination of head diameter, frequency, amplitude, and the power delivery system. Misaligning these specifications with the pour requirements leads to either labor inefficiencies or compromised concrete quality.
Head diameter, frequency, and amplitude
The diameter of the vibrator head directly determines the radius of action—the distance from the center of the head to the outer edge of the effectively consolidated concrete. As a general heuristic, the radius of action is approximately four times the diameter of the head. Commercial head diameters range from 0.75 inches for highly congested precast work up to 6 inches for mass concrete placements like dams.
Frequency, measured in vibrations per minute (VPM), and amplitude, the peak-to-peak displacement of the head, work in tandem. High frequency (12,000 to 17,000 VPM) with low amplitude (0.015 to 0.03 inches) is ideal for liquefying the mortar and moving small aggregates. Conversely, lower frequencies (8,000 to 10,000 VPM) combined with high amplitude (0.04 to 0.08 inches) are required to move heavy, large-diameter coarse aggregates in mass pours.
| Head Diameter | Average Radius of Action | Min. rebar Clear Spacing | Est. Compaction Rate |
|---|---|---|---|
| 1 inch (25 mm) | 3 to 5 inches | 1.5 inches | 1 to 5 cu yd/hr |
| 2 inches (50 mm) | 7 to 10 inches | 3.0 inches | 10 to 17 cu yd/hr |
| 3 inches (75 mm) | 11 to 14 inches | 4.5 inches | 25 to 40 cu yd/hr |
| 6 inches (150 mm) | 20 to 24 inches | 9.0 inches | 40+ cu yd/hr |
Power source, shaft length, and portability
Vibrators are driven by electric, gas, or pneumatic power sources. Electric Vibrators (operating on standard 115V or 230V) are the most common in commercial construction due to their consistent power delivery and lack of exhaust emissions, making them safe for enclosed spaces. Gas-powered backpack vibrators, typically generating 2.5 to 4 horsepower, offer unmatched mobility for sprawling sites like highway paving where trailing electrical cords are a hazard.
Pneumatic vibrators utilize compressed air and are highly durable, often deployed in heavy civil projects where heavy-duty 80 to 100 psi air compressors are already on site. Shaft length is another critical portability factor; flexible shafts range from 2 feet for shallow footings up to 30 feet for deep column pours. Selecting a shaft that is excessively long increases friction, reduces power transmission to the head, and creates a tripping hazard.
Performance trade-offs by application
Selecting the perfect specification requires balancing performance trade-offs. A large 3-inch head will boast a compaction rate of up to 40 cubic yards per hour, easily keeping pace with high-volume concrete pumps. However, this large head is heavy, rapidly fatiguing the operator, and physically cannot fit into wall forms with dense rebar mats.
Conversely, a highly portable 1-inch pencil vibrator is easy to maneuver but maxes out at roughly 5 cubic yards per hour. If a contractor attempts to consolidate a 50-cubic-yard slab pour with a 1-inch vibrator, the concrete will begin to set long before the operator can cover the necessary area, resulting in cold joints and inadequate compaction.
Match the Vibrator to Site Conditions
Even the highest-grade equipment will fail to perform if it is not properly matched to the immediate site conditions and operated according to strict procedural standards. The dynamic environment of a construction site requires project managers to assess physical obstructions, pour logistics, and occupational safety parameters before finalizing equipment selection.
Pour volume, reinforcement density, and access
The density of the reinforcing steel is the primary limiting factor for vibrator sizing. Engineering standards dictate that the clear spacing between rebar must be at least 1.5 times the diameter of the vibrator head to prevent the equipment from becoming wedged. If the structural drawings show a minimum clear spacing of 3 inches, the maximum allowable vibrator head is 2 inches.
Pour volume and delivery logistics also dictate equipment needs. If concrete mixer trucks are scheduled to arrive at a rate of 30 cubic yards per hour, the site must be equipped with enough vibrators—and operators—to match or exceed that 30 cu yd/hr consolidation rate. Failing to match the vibrator output to the pour volume forces operators to rush, inevitably leaving pockets of unconsolidated concrete.
Operating procedures for proper insertion and spacing
Proper operating procedure is just as critical as the hardware. The vibrator must be inserted vertically into the concrete at regular intervals. These insertion points should be spaced so that the radius of action overlaps the previous insertion by 1 to 2 inches, ensuring no dead zones are left behind.
The rate of insertion and extraction is a strict operational metric. The head should be allowed to drop rapidly into the mix under its own weight (approximately 1 inch per second) to reach the bottom of the lift. Extraction, however, must be deliberately slow—roughly 1 inch per second, or about 3 seconds per foot of depth. This slow withdrawal allows the fluidized concrete to collapse back into the void left by the vibrating head, preventing the formation of permanent vertical air shafts.
Safety, maintenance, and compliance requirements
Site conditions must account for occupational safety and compliance. Prolonged exposure to heavy vibration can cause Hand-Arm Vibration Syndrome (HAVS) in operators. Equipment must be selected and rotated to keep operator exposure below the OSHA/regulatory action value, typically standardized at an 8-hour energy equivalent of 2.5 m/s² A(8).
Maintenance schedules are equally vital for site compliance and operational continuity. Concrete Vibrators operate in highly abrasive, alkaline environments. Contractors must mandate routine inspections, checking the flexible shaft for kinks and re-greasing internal bearings every 100 operating hours to prevent catastrophic failure mid-pour.
Make the Final Buying or Rental Decision
The final phase of vibrator selection shifts from engineering specifications to procurement strategy. Contractors must evaluate the financial implications of acquiring the equipment, weighing the lifetime value of a purchased asset against the flexibility and lower upfront burden of renting. This decision is heavily influenced by the firm's project pipeline, maintenance capabilities, and the specific demands of the upcoming pour.
Purchase cost versus rental cost
A comprehensive cost analysis relies on anticipated utilization rates. Commercial-grade internal vibrators carry purchase prices ranging from $300 for basic electric units to over $1,500 for high-frequency, large-diameter systems with extended shafts. In contrast, daily rental rates typically hover between $40 and $80 depending on the model and regional market.
The industry standard rule of thumb dictates that if a specific vibrator model will be utilized for more than 15 operating days per calendar year, purchasing the unit yields a superior return on investment. However, for specialized equipment—such as a massive 6-inch pneumatic vibrator required for a one-off dam repair—renting remains the most fiscally responsible choice, entirely eliminating long-term storage and depreciation costs.
Supplier quality and support questions
When executing a purchase, the quality of the supplier and their post-sale support network is paramount. Contractors should interrogate suppliers on warranty periods, demanding a minimum of 1 to 3 years of coverage for the motor and internal head bearings. Given the harsh operating environment, premature wear is a realistic threat.
Furthermore, supply chain agility must be verified. The lead time for critical replacement parts, specifically flex shafts and replacement heads, should be guaranteed at under 48 hours. A vibrator failure during a critical foundational pour cannot wait a week for parts to ship; the supplier must have a robust local inventory to minimize project downtime.
Final selection checklist
Before issuing a final purchase order or rental agreement, project managers should execute a rigorous final selection checklist. First, verify that the selected head diameter is less than two-thirds of the minimum rebar clearance. Second, confirm that the combined compaction rate of the selected units exceeds the scheduled hourly delivery rate of the concrete supplier.
Finally, ensure adequate redundancy is built into the procurement order. The harsh reality of concrete placement is that equipment fails under load. Standard site protocol requires maintaining a strict backup ratio: for every three active vibrators operating on the pour, there must be at least one fully functional, identical backup unit staged on site, tested, and ready for immediate deployment.
Key Takeaways
- Select vibrator size and output based on concrete slump, reinforcement spacing, form geometry, aggregate type, and pour conditions.
- Use higher-amplitude vibration for stiff 1-inch to 2-inch slump mixes, and reduce vibration energy for more fluid mixes around 6 inches to prevent segregation.
- Proper consolidation removes entrapped air that can range from 5% to 20% of fresh concrete volume.
- Correct vibration can improve concrete density and may increase compressive strength by up to 30% compared with poorly consolidated placements.
- Avoid undersized vibrators because they can cause honeycombing, bug holes, and reduced bond strength around reinforcing steel.
- Avoid oversized or excessive vibration because it can separate aggregate from paste and weaken the finished concrete.
Frequently Asked Questions
What does a concrete vibrator do?
A concrete vibrator transmits high-frequency vibration into fresh concrete, reducing internal friction so the mix settles and trapped air rises out. This improves density, strength, durability, and surface finish.
Why is choosing the right concrete vibrator important?
The wrong vibrator can leave voids, honeycombing, bug holes, weak rebar bond, or segregation. Proper selection helps achieve uniform consolidation and can significantly improve compressive strength and durability.
How does concrete slump affect vibrator selection?
Low-slump concrete, such as 1 to 2 inches, needs stronger vibration with higher amplitude. High-slump concrete, such as around 6 inches, usually requires gentler vibration to avoid segregation.
Can over-vibration damage concrete?
Yes. Over-vibration can separate the mix, forcing heavy aggregate downward while water and cement paste rise to the surface. This reduces uniformity and may weaken the finished concrete.
What defects indicate poor concrete vibration?
Common signs include honeycombing, excessive bug holes, exposed aggregate, uneven surfaces, and poor bonding around reinforcement. These defects usually point to incorrect equipment, poor technique, or insufficient vibration time.