Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


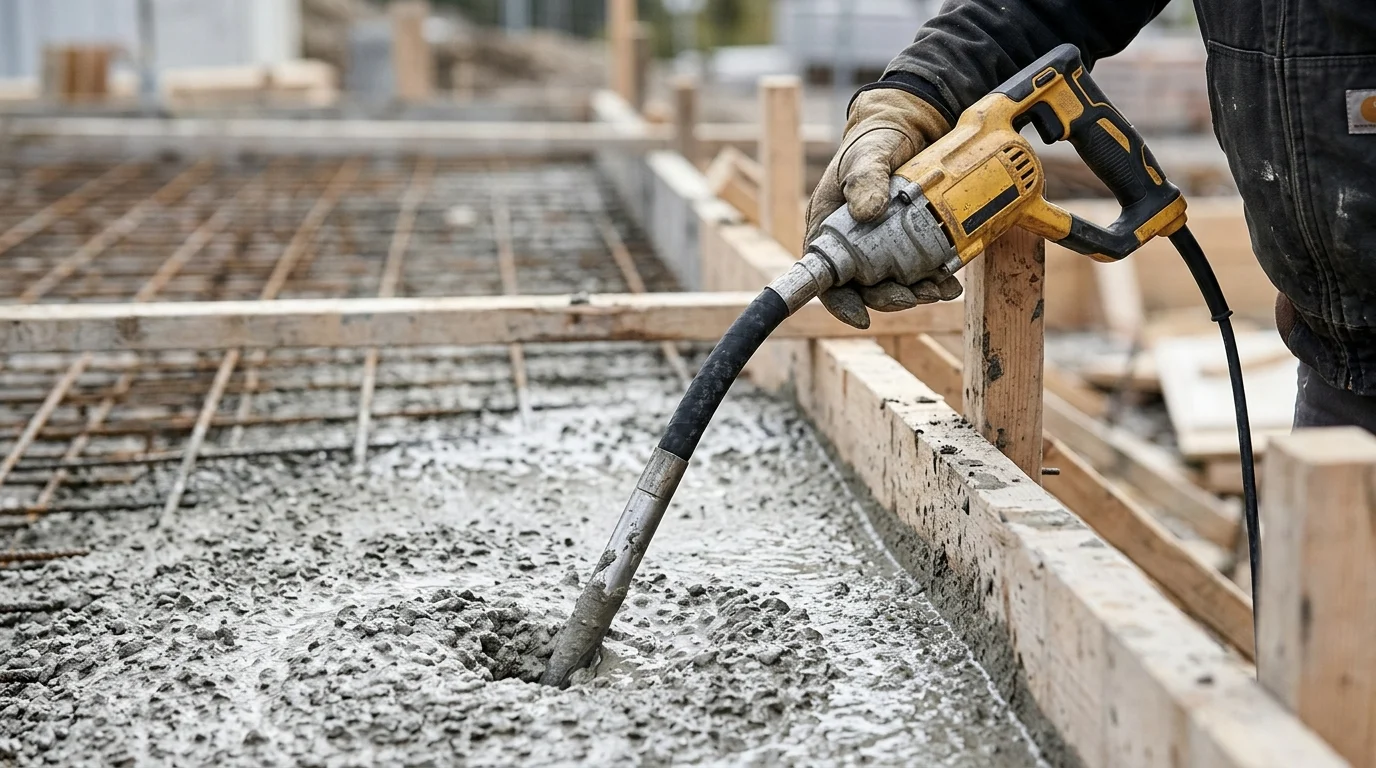
A Concrete Vibrator may look like a simple jobsite tool, but its performance directly affects pour quality, labor efficiency, and structural reliability. Operating at roughly10,000 to 17,000 vibrations per minute, an immersion vibrator works inside one of the harshest environments on site: wet, abrasive, alkaline concrete. Without disciplined inspection, cleaning, lubrication, and electrical checks, small defects can become failed bearings, burned motors, unsafe cables, or poorly consolidated concrete. This guide explains how maintenance teams can protect vibrator heads, flexible shafts, drive units, and power systems while reducing costly downtime and helping every pour achieve consistent density and finish quality.
Why Immersion Concrete Vibrator Maintenance Matters
Immersion concrete vibrators, commonly referred to as poker vibrators, are indispensable for eliminating entrapped air and ensuring the structural density of poured concrete. Given that these devices operate in highly abrasive, alkaline environments while generating internal frequencies between 10,000 and 17,000 vibrations per minute (VPM), baseline wear is inevitable.
Establishing a rigorous maintenance protocol is not merely a matter of asset management; it is a critical requirement for maintaining the structural integrity of the finished concrete and preventing catastrophic equipment failure during active pours. When managing heavy civil or commercial construction projects, understanding the operational threshold of these tools directly impacts both the project budget and the final quality of the concrete matrix.
Maintenance goals for project teams
For project management and equipment maintenance teams, the primary goal of a vibrator maintenance program is to maximize the operational lifecycle of the equipment while sustaining optimal amplitude and frequency. A well-maintained high-frequency vibrator should reliably deliver between 300 and 500 hours of continuous operation before requiring a major mechanical overhaul.
By stabilizing performance metrics—specifically maintaining a consistent amplitude of 1.5mm to 3.0mm depending on the poker head diameter—maintenance teams ensure that the equipment transfers energy into the concrete mix efficiently. This consistency achieves the required radius of action without overtaxing the drive motor, ensuring that every cubic yard of concrete receives uniform consolidation.
Risks of poor maintenance
Failing to adhere to strict maintenance schedules introduces severe operational and safety risks. Mechanical seizure is a primary threat; the vibrator head houses eccentric weights spinning at high velocities, and without adequate lubrication, internal bearing temperatures can rapidly exceed 150°C. This excessive heat leads to thermal expansion, lubricant breakdown, and catastrophic bearing failure.
Electrical hazards are equally prominent in 110V or 220V systems. Compromised cable insulation or worn motor housings can expose operators to lethal shocks, particularly in wet concrete environments. Furthermore, a degrading flexible shaft experiencing excessive internal friction will draw higher amperage, frequently tripping circuit breakers and permanently burning out stator windings.
Impact on concrete quality and downtime
The secondary consequences of poor maintenance manifest directly in the quality of the concrete structure and project timelines. A vibrator experiencing a 20% drop in optimal RPM will fail to mobilize the concrete aggregate properly, leaving entrapped air voids and honeycombing that can reduce the concrete's localized compressive strength by up to 30%. Remediation of such structural defects requires expensive epoxy injections, surface patching, or even localized demolition.
Simultaneously, unexpected equipment failure during a time-sensitive pour leads to compounding downtime costs. With standard concrete pouring crews and pump trucks costing upwards of $500 to $2,000 per idle hour, maintaining a functional, fully serviced vibrator inventory is a strict financial necessity for any general contractor.
Key Components to Inspect Regularly
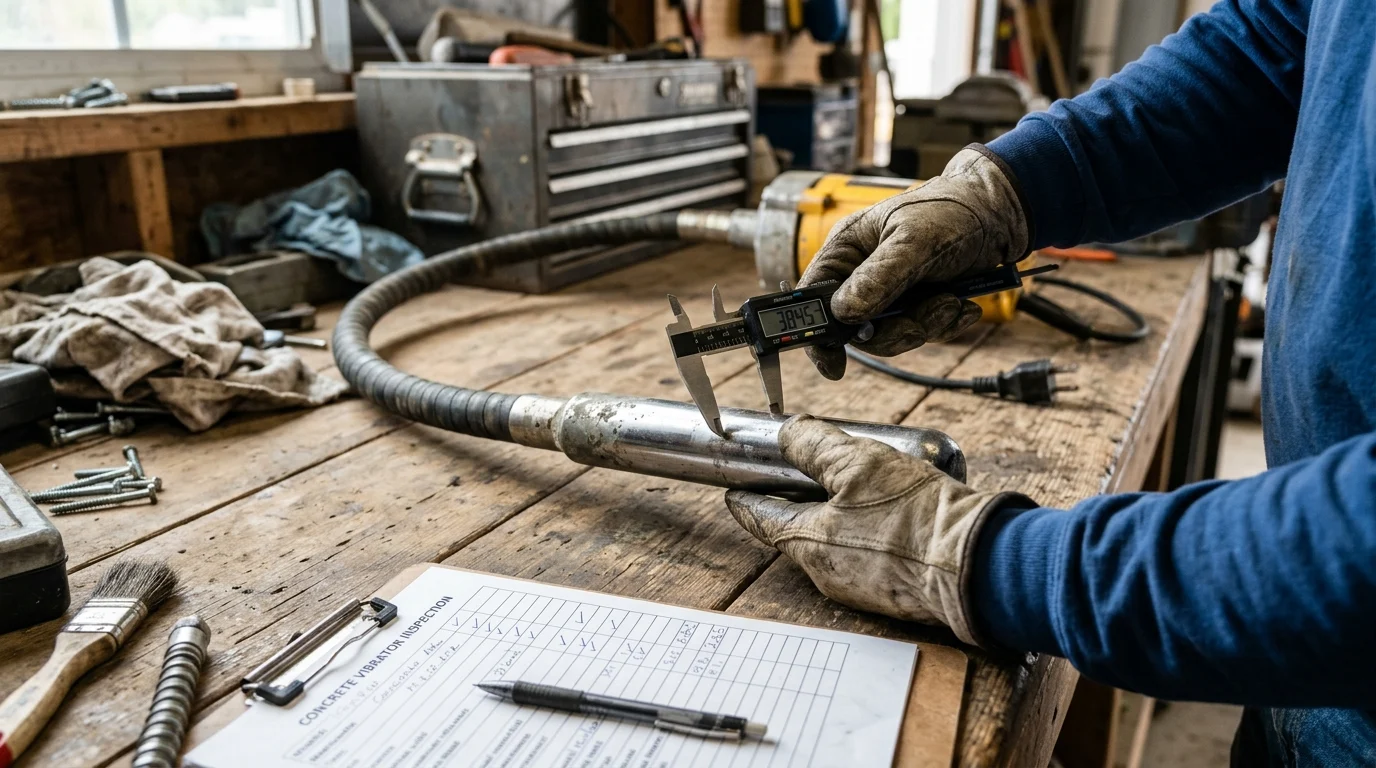
An immersion concrete vibrator is a complex assembly of high-stress mechanical and electrical components. Effective maintenance requires a granular understanding of these parts, as each component exhibits distinct failure modes when subjected to the abrasive slurry and high-impact conditions typical of a construction site.
Motor, shaft, head, bearings, and seals
The core assembly comprises the drive motor, the flexible transmission shaft, the vibrating head (poker), and the internal bearings and seals. The vibrating head, typically ranging from 25mm to 75mm in diameter, houses an eccentric weight supported by specialized high-speed bearings designed to withstand intense radial loads.
The flexible shaft, generally 3 to 9 meters in length, consists of a rotating high-carbon wire core encased in a reinforced rubber and steel mesh outer casing. Oil seals within the poker head are particularly critical; they must prevent the highly alkaline cement paste from infiltrating the bearing chamber while retaining the specialized high-temperature synthetic oil or grease required for high-speed operation.
Signs of wear, overheating, and vibration loss
Technicians must be trained to identify early indicators of component degradation. Overheating is a primary symptom of impending failure; if the exterior casing of the motor or the poker head exceeds 80°C under normal load, it typically indicates failing bearings, severe friction in the flexible shaft, or a lack of internal lubrication.
A noticeable loss of vibration intensity or a drop below the standard 10,000 VPM under load suggests that the flexible core is fraying, the motor brushes are severely worn, or the voltage supply is inadequate. Abnormal acoustic profiles, such as high-pitched squealing or harsh grinding noises, are immediate indicators of metal-on-metal contact due to bearing cage collapse or eccentric weight misalignment.
Electric vs pneumatic vibrator inspection points
Inspection protocols must be tailored to the specific power source of the vibrator. For electric units, technicians must regularly inspect the carbon brushes, replacing them when they wear down to a residual length of 8mm to prevent destructive arcing and commutator damage. Stator vents must also be checked for concrete splatter blockages.
Conversely, pneumatic immersion vibrators require continuous monitoring of the air supply mechanics. Pneumatic units rely on an inline lubricator that must deliver 2 to 3 drops of pneumatic oil per minute to prevent the internal rotor vanes from seizing. Furthermore, pneumatic inspections must verify that the compressor delivers a stable 80 to 100 PSI at the required cubic feet per minute (CFM) rating, as line pressure drops directly correlate to a proportional loss of vibration frequency.
| Feature/Component | Electric Vibrator Inspection | Pneumatic Vibrator Inspection |
|---|---|---|
| Power Supply | Voltage drop, cable insulation, RCD function | Air pressure (80-100 PSI), CFM flow rate, hose leaks |
| Motor/Drive | Carbon brush length (min 8mm), commutator wear | Rotor vane integrity, exhaust port blockages |
| Lubrication | Periodic bearing grease/oil replacement | Continuous inline oiler (2-3 drops/min) |
| Cooling | Air vent clearance, stator temperature | Air expansion cooling (monitor for freezing in high humidity) |
Maintenance Before, During, and After Use
Maximizing the durability of an immersion concrete vibrator requires integrating maintenance practices directly into the daily operational workflow. Equipment degradation is significantly accelerated by improper handling during the pour, making operator training just as critical as the mechanical servicing performed in the workshop.
Pre-use power, cable, and head checks
Prior to any concrete pour, operators must conduct a rigorous series of pre-use checks. Electrical integrity is paramount; technicians should verify that extension cables are appropriately gauged to prevent a voltage drop exceeding 5% over a 50-meter run, which would otherwise cause the motor to overdraw current, overheat, and potentially melt the winding insulation.
All electrical connections must be routed through a Residual Current Device (RCD) tested to trip at a 30mA threshold. Mechanically, the connection threads between the flexible shaft, the motor housing, and the poker head must be inspected for tightness. A loose connection not only leads to power transmission loss but also creates a direct pathway for water and corrosive cement slurry to enter the drive core.
Operating practices that reduce equipment stress
Operating practices dictate the thermal and mechanical stress placed on the equipment. Immersion vibrators rely on the surrounding wet concrete to act as a heat sink. Consequently, operators must never run the vibrator in the open air for more than 10 to 15 seconds, as the internal bearings will rapidly overheat and seize without the cooling effect of the concrete.
During consolidation, the poker should be inserted vertically at uniform intervals of approximately 0.5 meters and left in place for 5 to 15 seconds until air bubbles cease escaping the surface. Operators must avoid using the vibrator to drag or push concrete horizontally across the formwork. This improper technique imparts severe lateral stress on the flexible shaft, leading to core snapping and premature casing rupture. Additionally, bending the flexible shaft tighter than a 500mm radius during operation creates excessive internal friction, accelerating core wear.
Cleaning, lubrication, drying, and storage
Post-operation procedures dictate the equipment's readiness for the next shift. The vibrating head and flexible casing must be cleaned immediately after withdrawal from the final pour, before the concrete can cure. A stiff-bristled brush and clean water are sufficient; operators must never use high-pressure washers directly on electric motor vents or switch housings, as moisture ingress will compromise the stator insulation.
Internally, the flexible shaft core requires lubrication every 50 to 100 operating hours. Technicians should extract the core, clean off the degraded grease, and apply a precise 1.5mm to 2mm layer of high-temperature lithium-based grease. Over-greasing must be avoided, as excess lubricant creates fluid friction that overloads the motor and generates additional heat. Finally, vibrators should be stored in a dry, climate-controlled environment, suspended vertically by the poker head if possible, to allow any internal condensation to drain and prevent the flexible core from taking a permanent structural set.
Preventive Maintenance Program
Transitioning from reactive repairs to a structured preventive maintenance (PM) program is essential for large-scale construction operations. A formalized PM framework minimizes unexpected breakdowns, optimizes parts inventory, and ensures that all equipment complies with stringent occupational safety regulations.
Daily, weekly, and monthly maintenance tasks
A tiered maintenance schedule provides the foundation for equipment reliability. Daily tasks are primarily visual and operational: verifying cable integrity, checking switch functionality, and ensuring thorough post-pour cleaning. Weekly maintenance, typically conducted after 40 hours of operation, involves deeper inspections such as measuring carbon brush wear on universal motors, inspecting the outer rubber casing for deep abrasions, and verifying the tightness of all threaded couplings.
Monthly or quarterly tasks, occurring roughly every 160 to 200 operating hours, require workshop disassembly. During this phase, technicians must extract the eccentric weight assembly, inspect the bearings for radial play, replace the oil seals, and conduct an insulation resistance test on electric motors, ensuring the reading remains strictly above 2 Megaohms.
Inspection records, checklists, and spare parts
Diligent record-keeping transforms raw maintenance data into actionable operational intelligence. Maintenance managers should track the Mean Time Between Failures (MTBF) for each vibrator unit to identify recurring issues related to specific operator habits or abrasive concrete mix designs. Utilizing standardized checklists ensures that no diagnostic step is bypassed during weekly or monthly teardowns.
Furthermore, these records dictate spare parts procurement. To prevent supply chain bottlenecks during peak construction seasons, sites should maintain a 10% to 15% spare parts inventory for high-wear consumables. This inventory must include replacement carbon brushes, flexible core cables, rubber seals, switch assemblies, and end caps for the poker heads.
Safety compliance and electrical protection
Compliance with electrical safety standards is a non-negotiable aspect of the PM program. Immersion vibrators operate in highly conductive, wet environments, making them subject to rigorous OSHA (such as standard 1926.404) and international safety mandates. Technicians must routinely verify the integrity of Class II double insulation or ensure absolute continuity in the grounding conductors of Class I equipment.
Portable Appliance Testing (PAT) should be conducted and logged at least quarterly. Additionally, thermal overload protectors within the motor winding must be tested to ensure they accurately break the circuit if internal temperatures exceed the manufacturer's specified threshold, typically calibrated around 105°C to 120°C.
| Maintenance Interval | Target Operating Hours | Key Inspection / Action Items | Acceptance Threshold |
|---|---|---|---|
| Daily | 8 - 10 Hours | Visual casing check, cable inspection, cleaning | Zero visible copper, zero wet concrete residue |
| Weekly | 40 - 50 Hours | Carbon brush check, coupling tightness | Brushes > 8mm, couplings torqued to spec |
| Monthly | 160 - 200 Hours | Core lubrication, insulation resistance test | Resistance > 2 MΩ, core grease layer 1.5mm |
| Bi-Annually | 500+ Hours | Bearing replacement, seal replacement, stator check | Zero bearing play, stator temp under load < 80°C |
Repair, Replacement, and Upgrade Decisions
Even with meticulous preventive maintenance, the harsh realities of site work dictate that components will eventually reach the end of their serviceable life. Equipment managers must continuously evaluate the Total Cost of Ownership (TCO) to make data-driven decisions regarding when to repair, when to replace, and when to upgrade their immersion vibrator fleet.
When repair is more economical
Determining the economic viability of a repair relies on the standard 50% rule: if the total cost of parts and labor exceeds 50% of the replacement cost of a new unit (which typically ranges from $800 to $1,500 for professional-grade models), replacement is generally favored.
Routine consumable replacements—such as swapping out carbon brushes for $15, replacing a frayed flexible core for $100, or installing a new heavy-duty switch—are highly economical and should be performed without hesitation. However, when multiple subsystems fail simultaneously, such as a burned-out stator combined with a seized poker head, the labor hours required for a comprehensive rebuild quickly outpace the residual value of the aging equipment.
Lifecycle signs that justify replacement
Certain lifecycle indicators clearly signal that an immersion vibrator has surpassed its reliable operational window. Repeated bearing burnouts within a short timeframe often indicate that the internal bearing housing has warped or expanded beyond acceptable tolerances, making further bearing replacements futile. Similarly, a stator winding failure caused by chronic overheating usually degrades the surrounding insulation and commutator beyond repair.
On the mechanical side, technicians must regularly measure the diameter of the vibrating head casing using calipers. If abrasive wear from the concrete aggregate reduces the casing diameter by more than 2mm from its original specification, the structural integrity of the tube is compromised. Operating a poker head with walls worn dangerously thin risks an in-pour rupture, which would destroy the internal mechanisms and contaminate the concrete mix with lubricating oil.
Balancing cost, performance, and concrete quality
Strategic fleet management involves balancing immediate capital expenditures against long-term performance and concrete quality. Upgrading from traditional universal motor vibrators to high-frequency inverter-driven models represents a significant initial investment, often exceeding $2,000 per unit. However, these advanced systems operate at 200Hz, eliminating the need for carbon brushes and flexible drive shafts by placing the motor directly inside the poker head.
This architectural upgrade drastically reduces mechanical friction and maintenance overhead. For projects demanding high-specification architectural concrete or involving heavily congested rebar configurations, the return on investment for upgraded equipment is rapidly realized. The reduction in maintenance downtime, coupled with the elimination of costly honeycombing remediation, ensures that the initial capital outlay is typically recovered within a 6-to-12-month operational window.
Key Takeaways
- Inspect the poker head, flexible shaft, motor, power cable, and connectors before each pour to prevent breakdowns during time-sensitive concrete placement.
- Keep vibrator frequency and amplitude stable, since a drop in RPM can reduce consolidation quality and increase the risk of honeycombing.
- Clean concrete residue from the vibrator head immediately after use to reduce corrosion, seal damage, and performance loss.
- Monitor bearing heat, lubrication condition, and unusual noise because internal temperatures above 150°C can trigger bearing seizure and catastrophic failure.
- Maintain a serviced backup vibrator inventory because idle crews and pump trucks can cost $500 to $2,000 per hour during unexpected downtime.
- Plan major mechanical overhauls around the 300- to 500-hour operating range for well-maintained high-frequency immersion vibrators.
Frequently Asked Questions
How often should an immersion concrete vibrator be inspected on site?
Inspect the vibrator before every pour, focusing on the poker head, flexible shaft, power cable, switch, and connectors. For heavy daily use, schedule deeper servicing at fixed operating-hour intervals to catch bearing wear, lubrication failure, and electrical insulation damage before breakdowns occur.
What operating signs indicate poor maintenance?
Warning signs include reduced vibration intensity, overheating, unusual noise, excessive amperage draw, frequent breaker trips, shaft friction, or inconsistent concrete consolidation. These symptoms often point to worn bearings, inadequate lubrication, damaged cables, or a failing flexible shaft.
Why is cleaning the vibrator head after each use important?
Fresh concrete is abrasive and alkaline, and hardened buildup can trap moisture, accelerate corrosion, restrict heat dissipation, and damage seals. Cleaning the poker head immediately after use helps preserve vibration efficiency and extends the service life of the equipment.
Can a poorly maintained concrete vibrator affect concrete strength?
Yes. If the vibrator loses RPM or amplitude, it may fail to remove entrapped air properly, causing voids, honeycombing, and weak zones. The article notes that poor consolidation can reduce localized compressive strength by up to 30%.
What is a typical service-life target before major overhaul?
A well-maintained high-frequency immersion vibrator should deliver about 300 to 500 hours of continuous operation before a major mechanical overhaul. Actual service life depends on workload, concrete mix abrasiveness, cleaning discipline, lubrication, and storage conditions.