
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


MAXMACH 550 Mini Vibratory Roller: Full-Hydrostatic Drive Meets 550kg Dual-Drum Compaction for Precision Asphalt & Soil Applications
What Is the MAXMACH 550 Mini Vibratory Roller
In my experience evaluating light construction machinery, the MAXMACH 550 stands out as a highly specialized and versatile piece of equipment. As a walk-behind mini Vibratory Roller, it bridges the critical gap between lightweight forward Plate Compactors and larger, less maneuverable ride-on machines, offering commercial-grade compaction in a highly condensed footprint.
How a 550 kg dual-drum roller is defined
A 550 kg dual-drum roller is categorized primarily by its operating weight, drum configuration, and power transmission method. The 550 kg (approximately 1,212 lbs) static weight provides the baseline linear pressure against the ground. However, its true compaction power is generated by internal eccentric shafts that produce high-frequency vibrations, effectively multiplying the dynamic force applied to the soil or asphalt.
The "dual-drum" designation means that both the front and rear steel cylinders provide active compaction, ensuring a uniform, flat finish with fewer passes. For precise technical baselines, the 550 Mini Vibratory Road Roller is defined by its integration of a full-hydrostatic drive system.
I always advise buyers to prioritize hydrostatic over mechanical drives in this specific weight class. A full-hydrostatic system utilizes hydraulic pumps and motors to govern both the travel speed and the vibration of the drums. This engineering choice eliminates reliance on mechanical chains, sprockets, or drive belts, thereby significantly reducing maintenance requirements and the risk of snapped belts on the job site. More importantly, hydrostatic drives allow for infinitely variable speed control and seamless forward-to-reverse transitions. This smooth directional shifting is an absolute necessity to prevent the drums from leaving divots, ridges, or resting marks on freshly laid hot mix asphalt.
Where this compact roller is commonly used
Because of its narrow profile, high maneuverability, and responsive hydraulic controls, I frequently see this compact roller deployed in confined or precision-demanding work zones where heavier equipment cannot safely operate.
The most common field applications include:
- Asphalt Patching and Repair: Ideal for pothole repairs, driveway edges, and road shoulder maintenance. The integrated water sprinkling system prevents hot asphalt from sticking to the dual drums.
- Trench Compaction: The compact width allows the machine to operate safely inside utility and pipeline trenches to compact granular soil, sand, and crushed stone backfill before paving.
- Pathway Construction: Highly effective for compacting both the aggregate sub-base and the final surface layers of pedestrian sidewalks, bicycle paths, and golf course cart paths.
- Commercial Landscaping: Used to establish firm, level foundations for retaining walls, patios, or large-scale decorative hardscapes.
To illustrate exactly where the 550 kg mini vibratory roller fits within a paving or municipal contractor's fleet, consider the following operational breakdown:
| Application Scenario | Standard Plate Compactor (90kg) | 550kg Mini Vibratory Roller | Ride-On Roller (1.5 Ton) |
|---|---|---|---|
| Narrow Utility Trenches | High suitability | High suitability | Cannot fit |
| Hot Mix Asphalt Finishing | Poor (leaves edge marks) | Excellent (smooth finish) | Excellent |
| Large Parking Lots | Highly inefficient | Moderate | Highly efficient |
| Transport Logistics | Fits in a pickup truck bed | Requires a small utility trailer | Requires a heavy-duty flatbed |
By understanding these operational parameters, procurement teams and project managers can accurately match the capabilities of a hydrostatic mini vibratory roller to the specific spatial constraints and finishing requirements of their infrastructure projects.
Further reading:
Which Performance Parameters Matter Most
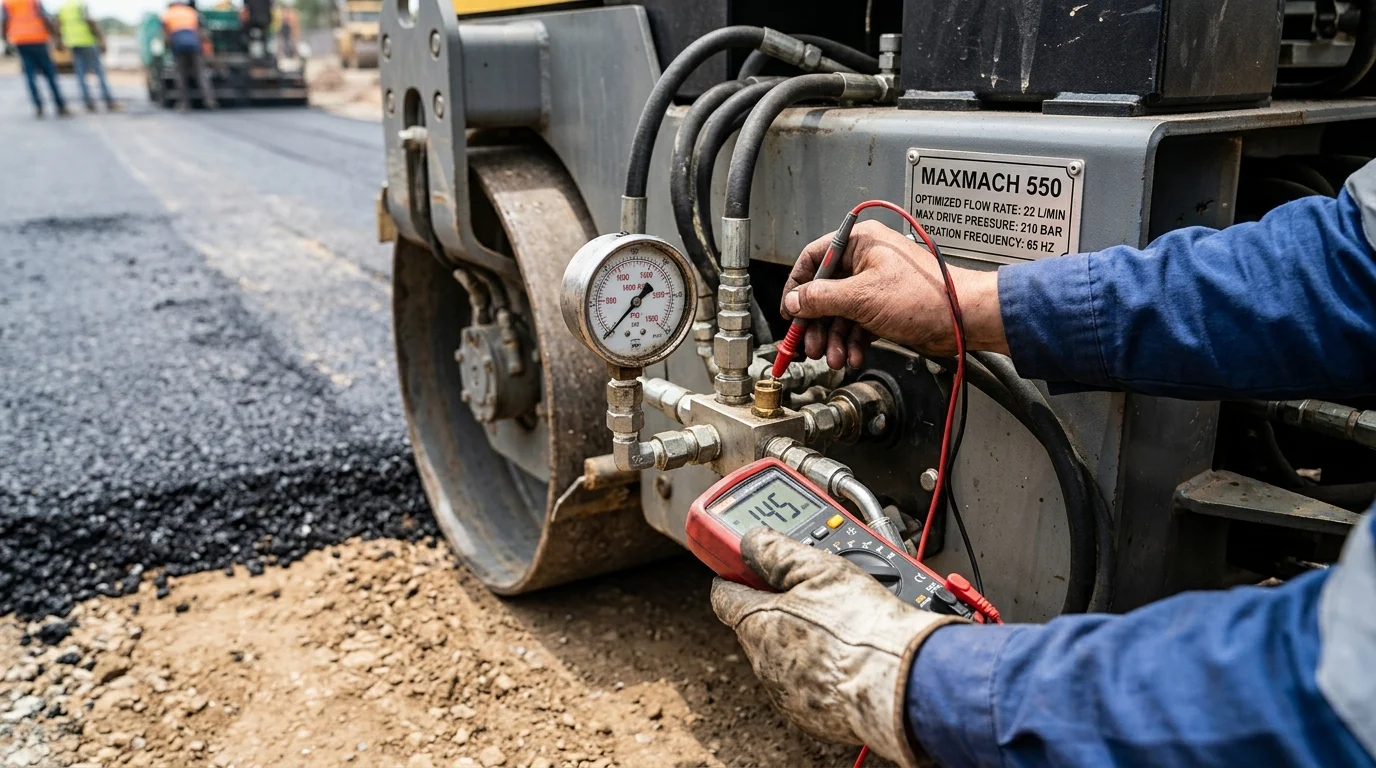
Evaluating the core performance parameters is essential to understand the capabilities of the MAXMACH 550. The physics of dynamic compaction rely on a precise interplay between static weight, centrifugal force, vibration frequency, and amplitude. When assessing a roller's viability for a specific project, these are the metrics scrutinized to ensure the target Proctor density can be achieved efficiently.
How operating weight and centrifugal force affect density
Operating weight provides the baseline static pressure, but centrifugal force drives deep material consolidation. In the 550 kg class, a typical centrifugal force rating ranges from 18 to 22 kN (roughly 4,000 to 5,000 lbf). When the eccentric weights inside the drums rotate, they generate this dynamic force, which is transmitted through the steel drum and into the ground.
The combination of a 550 kg static mass and a ~20 kN dynamic force creates an efficient compaction envelope. The static weight prevents the machine from bouncing uncontrollably, keeping the drum in continuous contact with the surface. Meanwhile, the centrifugal force overcomes the internal friction of soil particles or asphalt aggregates, forcing them into a tightly interlocked matrix. This synergy directly reduces the void ratio, increasing the load-bearing capacity of the compacted layer.
Why vibration frequency influences compaction quality
While centrifugal force dictates the power of the impact, vibration frequency dictates the rhythm. The MAXMACH 550 generally operates at a vibration frequency of around 70 Hz, which translates to 4,200 vibrations per minute (vpm). In field applications, this high frequency is critical for asphalt applications.
When compacting hot mix asphalt, a lower frequency can result in a rippled or "washboard" surface finish because the impacts are spaced too far apart relative to the machine's travel speed. At 70 Hz, the impacts occur so rapidly that, even at a standard travel speed of 2.5 km/h, the impacts overlap seamlessly. This high-frequency, low-amplitude (typically around 0.5 mm) configuration ensures that the asphalt surface is sealed smoothly without fracturing the aggregate.
How to interpret compaction depth claims
Manufacturers often publish maximum compaction depth claims, but these figures must be interpreted with an understanding of material science. For a typical 20 kN, 550 kg class roller, claims of compaction depths up to 30 cm (12 inches) are common. However, this depth is highly dependent on the soil classification and moisture content.
In ideal, well-graded granular soils (sands and gravels) with optimal moisture, achieving 95% standard Proctor density at a 25 to 30 cm depth is feasible after several passes. Conversely, when working with cohesive soils (clays and silts) or hot mix asphalt, the effective compaction depth drops significantly. For asphalt, lift thicknesses no greater than 5 to 8 cm (2 to 3 inches) are recommended to ensure uniform density from the bottom of the lift to the surface.
| Compaction Parameter | Typical Specification Range | Primary Operational Impact |
|---|---|---|
| Static Operating Weight | 500 – 580 kg | Establishes baseline surface pressure; restricts excessive bouncing |
| Centrifugal Force | 18 – 22 kN | Delivers deep dynamic energy; forces particle interlocking |
| Vibration Frequency | ~70 Hz (4,200 vpm) | Determines impact spacing; essential for smooth asphalt finishes |
| Nominal Amplitude | ~0.5 mm | Balances compaction energy with surface finish quality |
| Maximum Travel Speed | 3.0 – 4.0 km/h | Dictates productivity and impacts per linear meter |
How Does Full-Hydrostatic Drive Improve Control
One of the most significant technological advancements in modern walk-behind compactors is the transition from mechanical drive systems to full-hydrostatic drives. The drive system dictates how smoothly the machine accelerates, how it handles gradients, and how precisely the operator can maneuver around obstacles. The MAXMACH 550 utilizes a full-hydrostatic system, which is highly advantageous for professional-grade paving operations.
How full-hydrostatic drive compares with mechanical drive
To appreciate the hydrostatic advantage, it must be contrasted with traditional mechanical drives. Mechanical systems rely on a complex network of belts, chains, clutches, and gears to transfer power from the engine to the drums. In field observations, mechanical drives suffer from inherent drawbacks: chains stretch, belts slip under heavy loads, and engaging the clutch often results in a sudden, jerky movement.
A full-hydrostatic drive eliminates these wear-prone mechanical linkages. Instead, the engine drives a hydraulic variable displacement pump, which sends pressurized hydraulic fluid (such as ISO VG 46, though operators should always follow specific manufacturer recommendations) to hydraulic motors mounted directly inside or adjacent to the drums. This closed-loop hydraulic circuit provides seamless, continuous power transfer. This architecture delivers superior torque for climbing gradients (up to 30% gradeability on certain models) and drastically reduces the mechanical shock transmitted to the machine's frame and the operator.
Why variable travel control supports edge work
The most critical operational benefit of the hydrostatic drive is infinitely variable travel control. Unlike mechanical rollers that have fixed gear ratios, the hydrostatic pump allows the operator to adjust the speed smoothly from 0 to 4.0 km/h using a single control lever. This control is particularly important for edge work and asphalt finishing.
When compacting hot mix asphalt, any sudden stop, start, or jerky directional change will cause the steel drum to dig into the pliable material, leaving a permanent depression or "bow wave" that compromises the structural integrity and rideability of the pavement. The hydrostatic system's ability to feather the speed allows the operator to glide to a gentle stop and reverse direction without scarring the mat. This precision enables operators to work confidently along curbs, gutters, and delicate paver edges.
What hydraulic maintenance trade-offs to consider
While hydrostatic systems offer superior performance, they introduce specific maintenance trade-offs. Mechanical systems require frequent, low-skill interventions—such as tensioning chains every 50 hours. Hydrostatic systems are virtually maintenance-free on a day-to-day basis, but they demand strict adherence to fluid cleanliness protocols.
Operators should strictly follow the manufacturer's hydraulic maintenance schedule. Typically, the initial hydraulic oil and filter change must occur after the first 50 to 100 hours of operation to remove manufacturing break-in debris, followed by regular changes every 500 hours. A contaminated hydraulic system can lead to premature pump failure. Additionally, operators must observe practical safety caveats: adhering to vibration exposure limits, wearing appropriate hearing and vibration protection, ensuring slope stability before traversing inclines, and receiving proper training for hydrostatic controls before operation.
Where Does a 550 kg Dual-Drum Roller Fit Best
Equipment selection is about matching machine capabilities to site conditions. Deploying a 550 kg dual-drum roller involves distinct strategic phases, focusing heavily on asphalt paving logistics and subgrade preparation parameters.
How to plan asphalt compaction passes
When planning asphalt compaction with a machine of this size, the operation is typically structured into three distinct passes: breakdown, intermediate, and finish. Because the MAXMACH 550 is relatively light compared to highway-class rollers, timing is critical. The breakdown pass must be initiated while the hot mix asphalt is still between 120°C and 140°C. At this temperature, the binder is fluid enough to allow the centrifugal force to easily orient the aggregates.
For the breakdown pass, vibration is activated while operating at a slow, steady speed. Two to three vibratory passes are usually planned to achieve the bulk of the density. The intermediate pass follows closely behind, often with vibration still engaged if the mat temperature remains above 90°C. Finally, the finish pass is conducted in static mode (vibration turned off) to iron out any minor drum marks and seal the surface. Throughout this process, it is essential to ensure the water tank is full and the scraper bars are perfectly adjusted to keep the drums wet and clean.
How to adjust for moisture, lift thickness, and material type
For soil or aggregate sub-base preparation, the approach shifts to managing lift thickness and moisture content. For granular base materials like crushed stone or gravel, lift thicknesses should be restricted to a maximum of 150 mm (6 inches) per layer to ensure the 20 kN centrifugal force can penetrate effectively.
Moisture control is equally vital. It is necessary to test the soil to ensure it is at or near its Optimum Moisture Content (OMC). If the material is too dry, the vibration will pulverize the surface aggregates into dust without achieving depth penetration. If it is too wet, the material will pump and yield under the weight, trapping hydrostatic pressure in the soil voids. By controlling lifts and managing moisture, 95% compaction targets can consistently be hit with 4 to 5 passes.
When to choose the MAXMACH 550 over larger rollers
The decision between a 550 kg walk-behind roller and a larger 1.5-ton ride-on unit hinges on spatial constraints, transport logistics, and pass productivity. A 1.5-ton ride-on roller requires a heavy-duty trailer, a dedicated tow vehicle, and a wide turning radius, making it better suited for large, open projects. It cannot easily maneuver around manholes, streetlights, or within narrow residential utility trenches.
The MAXMACH 550 is chosen when agility translates directly into labor savings. Because it fits within a 700 mm footprint and features a foldable or highly ergonomic steering handle, it allows the operator to compact right up to the edge of an obstacle. Furthermore, at 550 kg, the unit can be safely loaded onto a standard flatbed truck or heavy-duty utility trailer using appropriately rated aluminum ramps. It is critical to specify minimum ramp capacities that exceed the machine's operating weight and to use secure tie-downs that meet local towing regulations. This logistical flexibility often makes the mini vibratory roller the most cost-effective choice for high-volume, multi-site urban repair contracts.
How Should Buyers Evaluate the MAXMACH 550
Evaluating heavy machinery requires a rigorous cost-benefit analysis. The true value of the MAXMACH 550, or any roller in its class, is determined by its component quality, its operational efficiency over thousands of hours, and the manufacturer's support infrastructure. A strict set of criteria helps ensure long-term return on investment.
Which buying criteria to compare
The first buying criterion to scrutinize is the powertrain and hydraulic component sourcing. Industry-standard engines—such as the Honda GX390 for gasoline variants or reputable air-cooled diesel engines like the 186F series—provide predictable power curves and global parts availability.
Equally critical is the hydraulic pump and motor assembly. Closed-loop hydrostatic systems featuring premium axial piston pumps from recognized manufacturers are preferred. Additionally, drum shell thickness should be measured. In the 550 kg class, a minimum drum thickness of 10 mm to 12 mm machined steel is expected. Anything thinner is susceptible to denting from large aggregates, which will permanently ruin the roller's ability to leave a flawless asphalt finish.
How to estimate total cost of ownership
Estimating the Total Cost of Ownership (TCO) over a standard 3-to-5-year lifecycle requires calculating fixed capital costs against variable operating expenses. The initial purchase price is merely the starting point. Fuel consumption, which for a 9 to 13 HP engine under heavy vibratory load averages approximately 1.5 to 2.0 liters per hour, must be factored in. Over a 1,500-hour operational life, fuel alone represents a significant portion of the TCO.
The cost of scheduled maintenance and consumable wear parts must also be modeled. This includes hydraulic oil, engine oil, air filters, polyurethane scraper bars, and heavy-duty rubber shock mounts. The shock mounts isolate the vibration from the engine and the operator handle. These isolators generally need replacement every 300 to 500 hours to prevent structural fatigue.
| Cost Category | Estimated Expense | Percentage of 3-Year TCO |
|---|---|---|
| Initial Capital Expenditure | Base Unit Acquisition Cost | ~45% |
| Fuel Consumption | 1.5 – 2.0 L/hr @ 1,500 hrs | ~30% |
| Scheduled Maintenance | Oils, filters, shock mounts, scraper bars | ~15% |
| Unplanned Repairs | Seal replacements, minor hydraulic service | ~10% |
What to check before specifying the roller
Before issuing a purchase order or specifying the roller for a fleet, a final pre-purchase checklist is recommended. First, verify the exact operating weight, drum vibration configuration, and centrifugal force against the most common project specifications to ensure the unit meets local municipal compaction codes. Then assess the ergonomics: does the handle feature safety mechanisms such as a dead-man switch or an emergency reverse / anti-crush protection control? These safety features are non-negotiable for walk-behind equipment.
Finally, evaluate the dealer network and warranty terms. Certainty is needed that replacement parts—specifically hydraulic seals, control cables, and rubber isolators—can be sourced and delivered promptly. A machine that sits idle waiting for a proprietary part costs hundreds of dollars a day in lost productivity. By rigorously checking these criteria, buyers can ensure that the MAXMACH 550 will serve as a durable, profitable asset in a compaction fleet.
Key Takeaways
- Use a 550 kg walk-behind dual-drum roller when a plate compactor is underpowered but a 1.5-ton to 3-ton ride-on roller is too large for the site.
- Confirm the exact configuration before purchase because some 550 kg dual-drum rollers drive both drums but vibrate only one drum.
- A typical 600 mm drum width and sub-700 mm machine width make this roller practical for sidewalks, utility cuts, trench work, and urban repair zones.
- For asphalt patching, use the sprinkler system consistently to reduce hot mix asphalt pickup and improve the final surface finish.
- Always check the official manufacturer datasheet for verified engine output, centrifugal force, vibration frequency, amplitude, gradeability, and water tank capacity.
Frequently Asked Questions
What is the MAXMACH 550 Mini Vibratory Roller best used for?
It is best suited for confined asphalt and soil compaction tasks such as pothole repair, utility trench reinstatement, sidewalks, bicycle paths, landscaping work, and municipal road maintenance.
How heavy is a 550 class walk-behind roller?
A 550 class roller typically operates in the 500 kg to 580 kg range, giving it more compaction mass than a plate compactor while remaining easier to transport and maneuver than ride-on rollers.
Does a dual-drum roller mean both drums vibrate?
Not always. Dual-drum usually means both front and rear drums compact and are driven, but buyers should verify whether one or both drums vibrate on the specific configuration.
Why is hydrostatic drive important on a mini vibratory roller?
Hydrostatic drive provides smooth forward and reverse control, helping operators maintain consistent speed and compaction quality in tight spaces, around edges, and near obstacles.
Can the MAXMACH 550 be used on hot mix asphalt?
Yes. With steel drums and a water sprinkler system, this type of roller is commonly used for hot mix asphalt patching and finishing, where preventing asphalt pickup is essential.