
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


The Dynamics of Dual-Shaft Eccentric Excitation: Performance Benchmarking of Diesel-Powered Reversible Vibratory Plate Compactors
How Dual-Shaft Eccentric Exciters Drive Compaction Performance
Heavy-duty Soil Compaction Equipment relies on the foundational mechanics of its exciter system to determine field performance. As engineering requirements for soil density and load-bearing capacity become more stringent, understanding the transition from basic single-shaft systems to advanced dual-shaft configurations is essential for modern civil construction.
The underlying principle of counter-rotating excitation represents a significant leap in directional control and energy transfer. Examining how these forces interact with granular and cohesive soils reveals how machines maintain optimal dynamic force without causing surface degradation or equipment instability. This analysis serves as a technical product profile detailing how modern reversible plates achieve these engineering outcomes, using a specific heavy-duty model as an illustrative example.
How the MAXMACH SCH450 Uses Dual-Shaft Excitation
The core architecture of a high-performance vibratory plate compactor like the MAXMACH SCH450 relies on a precisely synchronized dual-shaft eccentric exciter. Inside the exciter housing, two heavy-duty shafts equipped with eccentric weights rotate in opposite directions at high speeds. This mechanical design is the physical basis for generating substantial centrifugal forces capable of penetrating deep into the subgrade.
Synchronization of these two shafts dictates the machine's behavior. By coupling the shafts with precisely machined gears, the system ensures that the eccentric weights meet at exact intervals. This generates a unified pulse of kinetic energy that is transferred directly through the base plate and into the material being compacted, overcoming the internal friction of the soil particles. However, buyers must factor in total-cost-of-ownership caveats: this synchronized gear system requires stricter maintenance than simpler single-shaft designs, particularly regarding gear backlash tolerances, bearing life monitoring, and precise lubrication intervals.
How Eccentric Force Enables Forward and Reverse Travel
A primary advantage of the dual-shaft system lies in its ability to manipulate the phase angle between the two rotating eccentric weights. When the phase angle between the weights is exactly 0°, the horizontal force vectors generated by each shaft perfectly cancel each other out, while the vertical force vectors compound. This results in pure vertical vibration, allowing the machine to compact in a stationary position.
As the operator adjusts the hydraulic or mechanical control, the phase angle shifts. This shift disrupts the equilibrium of the horizontal forces, creating a net horizontal force vector that propels the equipment either forward or backward. This dynamic adjustment allows heavy reversible plates to navigate challenging terrain without relying on external propulsion mechanisms, depending entirely on the directional forces generated by the exciter.
Why Horizontal and Vertical Force Components Matter
Breaking down the exciter's output into its horizontal and vertical components clarifies the compaction data. The vertical component is responsible for delivering the compaction energy, maintaining the dynamic impacts required to reduce void ratios and increase density. Meanwhile, the horizontal component provides the directional momentum required to move the heavy chassis across the jobsite.
In heavy-duty models like the SCH450, this system generates a robust 65 kN of centrifugal force. If this dynamic excitation force exceeds the machine's static weight, the base plate will experience a "separation" or bouncing phenomenon, lifting off the soil and severely reducing compaction efficiency. Phase angle control not only enables direction switching but also allows operators to complete two-way compaction in narrow spaces without turning around—an engineering advantage that single-direction Plate Compactors cannot replicate.
Key SCH450 Specifications and Performance Benchmarks
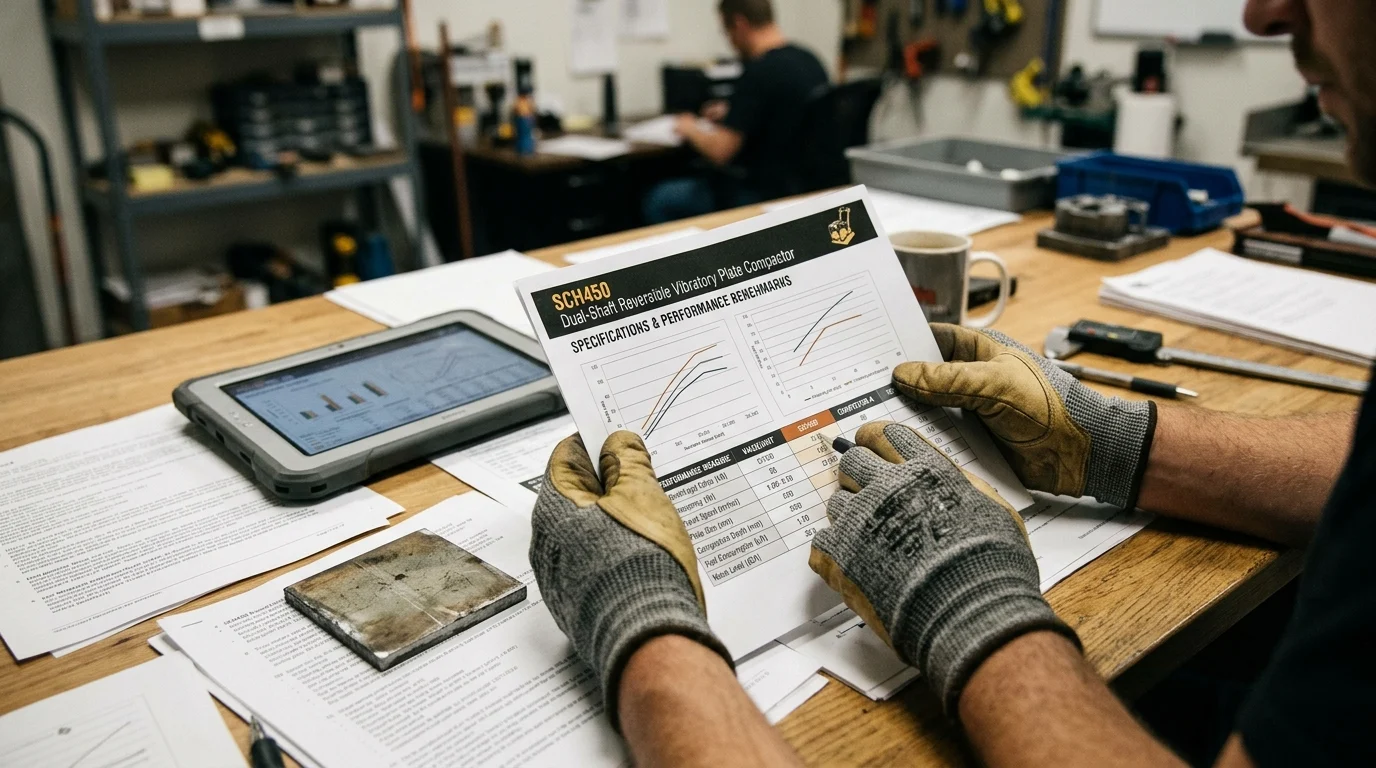
Moving from theoretical mechanics to practical design requires a rigorous look at the machine's core specifications. A compactor's ability to perform on demanding jobsites is strictly governed by its physical dimensions, mass, and power output.
Evaluating the manufacturer specifications provides a look at how a specific combination of weight, frequency, and force translates into verifiable engineering outcomes. These parameters are meticulously calculated to optimize the transfer of kinetic energy into various soil profiles.
Core Specs for Comparing Diesel Reversible Plate Compactors
Evaluating a diesel reversible plate compactor begins with its foundational chassis and mass. The physical footprint of the machine dictates its stability and the surface area over which its centrifugal force is distributed. Below is a detailed breakdown of the core specifications that define the SCH450's operational envelope.
| Specification Parameter | Metric Measurement | Imperial Measurement |
|---|---|---|
| Operating Weight | 500 kg | 1,102 lb |
| Base Plate Footprint (L × W) | 80 × 45 cm | 31.5 × 17.7 in |
| Overall Machine Height | 110 cm | 43.3 in |
| Centrifugal Force | 65 kN | 14,612 lbf |
| Vibration Frequency | 4,400 VPM | 73.3 Hz |
| Vibration Amplitude | 1.9 mm | 0.075 in |
| Compaction Depth | 30 cm | 11.8 in |
| Maximum Gradeability | 30° | 30° |
| Travel Speed | 25 m/min | 82 ft/min |
| Theoretical Area Coverage | 650 m²/h | 6,996 ft²/h |
The mechanical design of this operating weight paired with its base plate creates an ideal static pressure profile. Vibration amplitude—the maximum vertical displacement of the base plate—is a critical metric alongside force and frequency. It determines the compaction depth and dictates whether the plate risks lifting off the soil during operation. Substantial mass is critical; it acts as the necessary counter-weight to the immense upward forces generated by the exciter, ensuring that the maximum amount of energy is directed downward into the soil rather than being lost to machine bounce.
How 65 kN Centrifugal Force and 4,400 VPM Affect
Results
The relationship between centrifugal force and vibration frequency is the primary determinant of compaction depth and overall efficiency. The exciter force breaks the friction between soil particles so they can settle into a denser matrix. The higher the excitation frequency, the greater the compaction energy delivered per unit of time.
Operating at a peak frequency of 4,400 VPM (vibrations per minute), the exciter delivers rapid, successive impacts. Combined with its maximum centrifugal force, the performance data shows reliable deep compaction per pass, depending on the soil type. However, strict performance limitations exist. In highly cohesive clays or overly wet, saturated conditions, vibratory compaction is largely ineffective and risks destabilizing the subgrade; these environments require specialized padfoot rollers or rammers instead. In suitable materials, the synergy between force, amplitude, and frequency determines how quickly optimal soil density is achieved.
Why a 13 HP Diesel Engine Improves Torque and
Reliability
Sustaining peak vibration and force requires a robust power plant. The SCH450 utilizes a 13 HP diesel engine, a choice driven by the specific torque requirements of heavy compaction. Diesel engines inherently produce higher torque at lower RPMs compared to their gasoline counterparts, which is vital for maintaining exciter speed when the base plate encounters highly cohesive or deeply compacted soils.
This continuous, high-torque output directly impacts the machine's mobility, particularly its manufacturer-claimed 30° maximum gradeability. While the engine provides the necessary torque, a 30° incline is unusually steep for Vibratory plates. Achieving this requires ideal soil-shear prerequisites to prevent slippage. Operators must observe strict safety caveats: operating near this limit introduces severe tipping hazards and demands stable, highly cohesive base conditions to maintain traction and safe control. Integrating this high-torque diesel power plant with the dual-shaft exciter creates a balanced compaction system that maximizes energy transfer into the soil.
Best Applications for Reversible Plate Compactors
Understanding the hardware and specifications is only half the equation; deploying the equipment in the correct environment is where engineering theory meets jobsite reality. Reversible Plate Compactors are specialized tools designed to solve specific logistical and spatial challenges that traditional compaction equipment cannot address.
Manufacturer test reports and operator observations indicate that the ability to seamlessly shift directions alters the entire workflow of a trenching or foundation project. Evaluating how this directional flexibility impacts labor hours, machine wear, and the final quality of the compacted surface is essential for proper deployment.
How Reverse Control Reduces Repositioning Time
In confined jobsites, the time spent maneuvering equipment often equals or exceeds the time spent actually compacting material. When utilizing a single-direction plate, reaching the end of a trench requires manual repositioning—a physically demanding and time-consuming process, especially with heavy machinery. The reverse control mechanism fundamentally eliminates this downtime.
With a consistent travel speed in both forward and reverse, operators can maintain continuous compaction passes. This seamless directional switching directly contributes to the machine's theoretical maximum area coverage rate. Actual throughput depends heavily on pass overlap, lift thickness, and operator technique. By keeping the machine in constant motion and actively compacting rather than pivoting, overall labor costs and project timelines are significantly reduced.
Reversible vs Single-Direction Plate Compactors
To clearly illustrate the engineering and operational differences between reversible and single-direction models, it is necessary to look at their respective capabilities in the field. While single-direction plates are suitable for open landscaping or light paving, heavy civil work demands greater versatility.
| Operational Feature | Reversible Plate Compactor (e.g., SCH450) | Single-Direction Plate Compactor |
|---|---|---|
| Directional Mobility | Forward, Reverse, and Stationary Spot Compaction | Forward Only |
| Ideal Environment | Confined trenches, bridge abutments, foundations | Open, unrestricted flat terrain |
| Repositioning Effort | Zero manual lifting/turning required | Requires physical pivoting at boundaries |
| Mass & Force Class | Heavy-duty (e.g., 500kg / 65kN) | Light to medium-duty (typically <150kg) |
| Compaction Depth | Deep subbase penetration (up to 30cm) | Shallow surface compaction (typically <15cm) |
This comparison highlights why reversible models are heavily favored in municipal and infrastructure projects. The ability to perform stationary spot compaction by zeroing the phase angle allows for targeted density increases around rigid structures like manholes or footings, a capability absent in forward-only machines.
Ideal Materials and Jobsite Conditions for the SCH450
Reversible vibratory plate compactors excel when applied to materials with low inter-particle cohesion and friction, such as river sand, crushed gravel, and specialized base mixtures. When outfitted with a water tank kit, the machine becomes effective for asphalt work—though this should be strictly limited to small patches and utility cuts rather than general paving—preventing the bituminous material from adhering to the base plate.
Typical application scenarios include road base and subgrade compaction, pipeline trench backfilling, bridge abutment backfilling, culvert side compaction, and building foundation perimeters. In these restricted zones, translating raw mechanical efficiency into measurable productivity gains relies on matching the equipment to the right granular soil applications.
Cost, Compliance, and Buyer Confidence Factors
Procuring heavy compaction equipment involves more than just evaluating technical specifications; it requires a comprehensive analysis of total cost of ownership, regulatory compliance, and the reliability of the supply chain. For procurement managers and engineering firms, these factors directly influence the return on investment.
It is essential to scrutinize the economic and support frameworks surrounding the machinery. From fuel consumption metrics to international emissions standards and warranty structures, every element plays a role in establishing buyer confidence and ensuring long-term operational viability.
Productivity, Fuel Use, and Hourly Operating Cost
The transition to a diesel power plant offers distinct economic advantages over the lifespan of the compactor. While the initial capital expenditure for a diesel-powered unit may be higher, diesel fuel possesses a higher energy density, allowing the engine to run longer on a single tank under heavy load conditions compared to gasoline alternatives.
When factoring in the machine's theoretical area coverage rate, this extended runtime between refueling stops helps optimize the total cost of ownership. For instance, evaluating manufacturer-stated fuel consumption metrics—often averaging 1.2 to 1.5 liters per hour for a 13 HP engine—allows contractors to calculate precise hourly operating costs. This consistent productivity, combined with steady fuel efficiency, supports continuous, multi-shift operations on large-scale infrastructure projects, making the initial investment highly practical for demanding environments.
EPA Certification, Warranty, and Inspection Evidence
Regulatory compliance and quality assurance are non-negotiable for modern construction fleets. The inclusion of an EPA-certified engine—alongside equivalents like EU Stage V or China Nonroad Stage IV standards for international markets—ensures that the equipment meets stringent environmental regulations, allowing it to be legally deployed without facing emissions penalties or site bans.
Furthermore, buyer confidence is reinforced through tangible quality guarantees. A manufacturer-stated warranty covering core components—typically offering 12-month or 1,000-hour duration terms—provides a concrete financial safety net against manufacturing defects. To bridge the gap in international trade, providing video factory inspections prior to shipment allows buyers to visually confirm the equipment's operational status. Coupled with detailed mechanical test reports that verify the machine's output and frequency, these measures provide empirical evidence of the equipment's capabilities before it ever reaches the jobsite.
After-Sales Support Expectations for Overseas Buyers
For overseas buyers, the anxiety of purchasing heavy machinery often stems from the potential lack of after-sales support. A robust after-sales service infrastructure is critical to minimizing downtime. Knowing that technical support is available is insufficient; buyers must secure concrete support deliverables.
Commitments such as regional spare parts stocking, dedicated remote diagnostics channels, and guaranteed 24-to-48-hour response windows provide a critical layer of operational reliability. This infrastructure ensures that routine maintenance—such as bearing lubrication and gear synchronization—as well as troubleshooting and parts replacement, can be handled efficiently, regardless of the jobsite's global location. The combination of emissions compliance, rigorous mechanical test reporting, and verifiable factory inspections establishes a robust quality assurance framework, giving overseas buyers the engineering confidence required to deploy heavy compaction equipment on critical infrastructure projects.
How to Decide If the MAXMACH SCH450 Is the Right
Arriving at a final procurement decision requires synthesizing the engineering principles, hardware specifications, and economic factors discussed. A heavy-duty reversible plate is a highly specialized piece of equipment, and determining if it is the right choice depends on aligning its capabilities with specific project demands.
Walking through a structured decision matrix allows contractors and engineers to objectively assess whether a diesel-powered reversible plate compactor will deliver the required density, maneuverability, and financial return for their operational portfolio.
Jobsite Decision Checklist
Before committing to a heavy-duty compactor, project managers should evaluate their typical jobsite conditions against the machine's performance thresholds. The first consideration is spatial constraint: does the work frequently involve narrow pipeline trenches or tight foundation perimeters where a turning radius is virtually non-existent? If so, the reversible functionality is a prerequisite.
Next, evaluate the required compaction depth and gradient. If project specifications demand deep compaction per lift, or if the terrain involves navigating steep slopes, the machine's high-torque diesel engine and maximum centrifugal force are necessary to meet engineering codes without requiring excessive passes. Furthermore, buyers should acknowledge genuine alternatives: if the job involves highly cohesive clay, a vibratory rammer is more effective, whereas articulated trench rollers may be better suited for extremely tight, deep utility trenches. If granular soil and moderate space define the project, the reversible plate remains ideal.
Additionally, buyers must prioritize operator safety by addressing hand-arm vibration (HAV) exposure. With declared vibration emission levels often exceeding 5.0 m/s² on heavy-duty models, operating this equipment requires strict adherence to HAV exposure limits, the implementation of vibration-damping handle systems, and enforced operator rotation protocols to prevent long-term occupational injuries.
Trade-Offs of Choosing a 500 kg Class Compactor
Choosing a machine in this heavy-duty weight class involves specific operational trade-offs. The primary drawback is transportability; a machine of this size cannot be manually lifted into a truck bed and requires dedicated lifting equipment like a crane or excavator for deployment and retrieval.
However, this mass is an intentional engineering necessity. As previously noted, substantial static weight is required to anchor the massive centrifugal force. Without this mass to counteract the dynamic force, the machine would suffer from separation, bouncing off the soil rather than compacting it. The trade-off of requiring lifting equipment is heavily outweighed by the ability to achieve deep, uniform soil density in a fraction of the time required by lighter machines.
Final Engineering Value Assessment
In a final assessment, heavy-duty reversible plates represent a calculated balance of raw power and precise directional control. By leveraging counter-rotating eccentric weights, they transform high-frequency vibration into measurable, efficient soil consolidation at peak theoretical coverage rates.
Ultimately, the precision of this synchronized system paired with substantial static mass ensures optimal dynamic energy transfer into subbase materials, delivering a reversible compaction solution that outperforms lighter, single-direction alternatives in both confined maneuverability and absolute compaction depth.
Further reading:
Key Takeaways
- Choose a dual-shaft reversible plate when the job requires controllable forward, reverse, and stationary compaction from the exciter system itself.
- Use the 0° phase angle principle to understand stationary compaction, where horizontal forces cancel and vertical force is maximized.
- Prioritize machines with strong centrifugal force, such as the SCH450’s 65 kN rating, for deeper energy transfer into demanding subgrade materials.
- Evaluate total cost of ownership by accounting for gear backlash checks, bearing monitoring, and strict lubrication intervals in dual-shaft systems.
- Match vertical force to density requirements and horizontal force control to maneuverability needs when comparing heavy-duty reversible compactors.
Frequently Asked Questions
What makes a dual-shaft eccentric exciter different from a single-shaft system?
A dual-shaft exciter uses two synchronized counter-rotating shafts with eccentric weights, allowing stronger vertical force and controllable horizontal force. This enables deeper compaction and reversible travel compared with simpler single-shaft designs.
How does a reversible vibratory plate compactor move forward and backward?
Forward or reverse travel is created by changing the phase angle between the two eccentric shafts. This shifts the horizontal force vector, propelling the plate in the selected direction without a separate drive system.
Why is the 0° phase angle important in compaction?
At a 0° phase angle, horizontal forces cancel while vertical forces combine. This produces near-stationary vertical vibration, useful when compacting a specific spot without advancing the machine.
What does 65 kN of centrifugal force indicate?
A 65 kN centrifugal force rating indicates strong dynamic impact energy for heavy-duty compaction. It helps the plate transmit vibration deeper into soil layers, improving density and load-bearing performance.
What maintenance does a dual-shaft reversible plate require?
Dual-shaft systems need disciplined maintenance, including lubrication at the correct intervals, bearing condition checks, and monitoring of gear backlash. Poor maintenance can reduce synchronization, increase wear, and weaken compaction performance.