
 Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


Tying Diameter Range as a Selection Criterion: Technical Rationale for the 6-58mm Capacity Class in Structural Rebar Consolidation
Why Tying Diameter Range Comes First
The tying diameter range serves as the primary selection factor for structural rebar fastening.Automated rebar tiers are highly specialized instruments, and specific capacity ranges—such as the 6-58mm (0.24-2.28in) class—represent a common mid-to-high-end operational benchmark for heavy construction. Establishing this parameter first defines the necessary tool capabilities, specifically the ability to accommodate varying wire lengths and wire diameters, which typically fall between 0.8-1.2mm (0.031-0.047in).
The tool's jaw geometry must physically accommodate the steel. The feeding mechanism should seamlessly handle the combined cross-sectional area of multiple intersecting rebars without jamming or over-torquing. Matching the correct diameter range to the project prevents equipment failure, minimizes wire waste, and ensures structural integrity at critical load-bearing junctions.
Total tying diameter vs. nominal bar size
Confusing the nominal bar size with the total tying diameter is a common planning pitfall. When lashing two #5 (16mm) rebars together, the required tying diameter is not simply 32mm. Due to the raised deformation ribs on the steel and the crossing angle of the bars, the actual cross-sectional footprint often exceeds the simple arithmetic sum. If a machine's maximum capacity is strictly 32mm, attempting to tie two 16mm ribbed bars will frequently result in jaw jams or incomplete wire wraps.
Tools with a broader capacity range, such as 6-58mm (0.24-2.28in), provide a necessary buffer. By offering a larger jaw aperture and extended wire guide, the tool accommodates the irregular geometries of heavily ribbed or epoxy-coated steel. The tool must feed sufficient wire length to fully encircle the expanded profile. Eliminating micro-voids in the tie ensures that the concrete pour does not dislodge the rebar matrix.
Project data to collect before comparing 4–28 mm models
Precise project data regarding structural detailing is necessary before comparing lighter 4-28mm models against heavier alternatives. Auditing bar bending schedules identifies the maximum intersecting diameters on the site. If 90% of the ties are simple #3 (10mm) meshes, a 4-28mm class tool is sufficient. However, overlapping splice zones or multi-bar column ties inevitably push the requirement toward a larger class like the 6-58mm (0.24-2.28in) range.
During this early data-collection phase, it is also critical to identify non-orthogonal ties (such as parallel laps or three-bar ties) and congested access geometries, as these complex configurations often demand larger jaw clearances than standard perpendicular intersections.
| Bar 1 Nominal | Bar 2 Nominal | Theoretical Sum (Without Rib Buffer) | Required Capacity Class Margin |
|---|---|---|---|
| #3 (10mm) | #3 (10mm) | 20mm | 4-28mm Class |
| #5 (16mm) | #5 (16mm) | 32mm | 8-45mm Class |
| #8 (25mm) | #8 (25mm) | 50mm | 6-58mm Class |
A data-driven approach ensures the chosen tool has the necessary jaw clearance and wire capacity for the site's specific rebar configurations, preventing equipment bottlenecks.
How Capacity Classes Compare
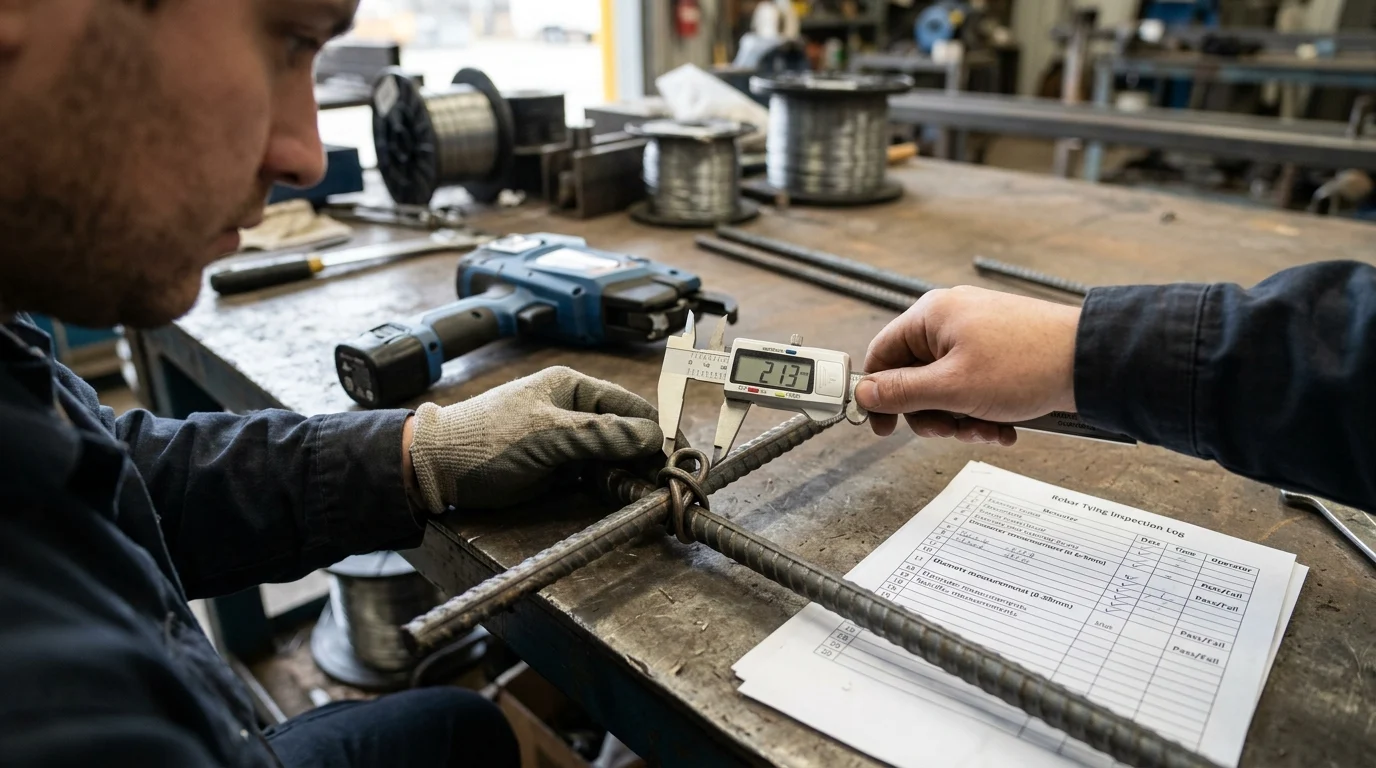
Manufacturers categorize automatic tying machines into distinct tiers, such as 4-28mm, 8-45mm, 8-58mm, and 6-58mm. While the 8-58mm and 6-58mm classes share a high-end capacity for heavy infrastructure, they are distinct specifications; the 6-58mm class offers a slightly lower minimum threshold for thinner meshes. Using these capacity classes as a baseline filter eliminates inadequate tools before they reach the job site. Each tier dictates specific physical features, most notably the internal coil housing size and the length of wire deployed per cycle.
Classification directly correlates with torque delivery. A machine designed for the 4-28mm range lacks the mechanical gearing to properly tension a knot around a 50mm combined diameter. Respecting these capacity classes guarantees that the tension applied to the knot is proportional to the mass of the steel being secured, preventing structural shifting during high-pressure concrete placement.
What a 4–28 mm comparison table should show
Comparing lightweight 4-28mm models against heavier units highlights the inverse relationship between wire length and operational longevity per coil. Because wire consumption is low on a 4-28mm tool, a single coil yields significantly more knots than larger models. This makes the lighter class highly efficient for flatwork and thin precast panels.
Note: The figures below represent typical manufacturer-specific approximations; actual yields vary by model, wire gauge, and manual settings.
| Capacity Class | Applicable Wire Length | Knots per Coil (Approx.) | Typical Structural Application |
|---|---|---|---|
| 4-28mm (0.16-1.10in) | 43-58cm (16.9-22.8in) | 230 knots | Light precast, slab meshes |
| 8-45mm (0.31-1.77in) | 60-82cm (23.6-32.3in) | 180 knots | Standard commercial framing |
| 6-58mm (0.24-2.28in) | 90-115cm (35.4-45.3in) | 110 knots | Versatile commercial/heavy civil |
| 8-58mm (0.31-2.28in) | 102-128cm (40.1-50.4in) | 95 knots | Heavy infrastructure, raft foundations |
The table reveals the limitations of lower-capacity models. As the required tying diameter increases, the tool demands exponentially more wire to achieve the necessary wrapping turns. The logistical trade-off is clear: higher capacity requires more frequent coil changes but delivers the holding power required for heavy structural steel.
Where the 6–58 mm capacity class fits
The 6-58mm (0.24-2.28in) capacity range is a versatile mid-to-high-end solution bridging commercial framing and heavy civil infrastructure, though it comes with trade-offs. These larger models typically involve increased tool weight, higher battery demands, greater upfront costs, and reduced maneuverability in tight reinforcement zones. However, they can deploy substantial wire lengths for massive #8 (25mm) intersections. While some advanced models feature sensors to automatically scale down the wire feed for smaller 10mm bars, others in this class require manual adjustment or rely on fixed-length settings.
This adaptability allows the tool to dynamically adjust its wire feed and tensioning based on the resistance encountered during the wrapping phase. Benchmarking these capacity ranges demonstrates how diameter limits dictate the tool's configuration and establish a baseline for engineering applications.
Wire Specification and Torque Requirements
The physical properties of the tying wire are inextricably linked to the machine's diameter capacity. Wire is a critical component of the fastening system, not a generic consumable. Professional-grade tiers typically require wire diameters strictly between 0.8-1.2mm (0.031-0.047in). If the wire is too thin, it snaps under the torque required for large-diameter steel; if it is too thick, it strains the tool's feeding motors and fails to twist tightly.
Achieving the correct tension requires matching wire stiffness—determined by diameter and material composition, such as soft annealed iron versus rigid galvanized wire—to the tool's capabilities. A perfectly calibrated machine using the wrong wire specification produces loose or broken ties, jeopardizing the stability of the rebar cage.
How wire length scales with tying diameter
As the total tying diameter increases, the required wire length scales up dramatically. Moving from a mid-capacity model to a heavy-duty 8-58mm or 6-58mm model nearly doubles the wire required per tie, halving the overall knot yield per coil. This is not a linear progression; it is a compounding requirement based on the circumference of the intersecting bars and the need for multiple wrapping turns.
The tool's internal spooling mechanism must feed this extended length at high velocity without tangling. If the tool fails to feed the exact required wire, the subsequent twisting phase will either choke the knot prematurely or leave slack. The correct length ensures the final twist sits flush against the steel, providing maximum resistance to shear forces during concrete placement.
Why larger diameters require higher torque
Larger rebar diameters inherently demand higher torque. When tying a 50mm combined diameter, the wire must be pulled tight enough to bite into the steel ribs and prevent the heavy bars from sliding. This requires balancing the wire's stiffness with the tool's twisting mechanism. Annealed wire offers excellent ductility for tight twists, while galvanized wire offers corrosion resistance but requires higher torque to bend.
If the torque threshold is set too high for the specific wire stiffness, the wire shears off rather than fastens. If set too low, the knot remains loose. High-end tools account for this by incorporating adjustable torque dials, allowing the operator to fine-tune the tension based on the specific wire loaded.
How independent feeding and twisting motors improve performance
Many modern high-capacity machines utilize independent dual-motor systems to achieve precise torque control. Dedicating one motor exclusively to feeding the wire and a separate motor to twisting the knot allows for specialized performance: the feeding motor operates at maximum speed to deploy wire rapidly, while the twisting motor engages with calibrated, variable torque.
Separating these functions reduces internal wear and provides more consistent tension across varying rebar diameters, ensuring reliable structural fastening.
Where a 6–58 mm Rebar Tying Machine Fits
Theoretical capabilities must map directly to real-world job site conditions. The specific structural elements being constructed dictate the ideal tool. A machine rated for 6-58mm (0.24-2.28in) offers a broad operational envelope, but its physical dimensions, weight balance, and jaw clearance must suit the deployment environment.
The tool must handle dense, congested rebar configurations just as effectively as open mats. Matching the tool to the site geometry allows workers to maintain a consistent tying rhythm—often achieving rapid cycle times on automated settings—minimizing ergonomic strain throughout a shift.
Common applications for the 6–58 mm class
The 6-58mm (0.24-2.28in) capacity range covers a wide variety of structural reinforcement scenarios. In beam-column joints, where steel congestion is at its highest, intersecting diameters between 16-32mm are frequent. High-capacity tools handle these heavy intersections effectively. In precast component factories, where diameters typically range from 6-25mm, these tools can scale down wire usage to match the application.
For heavy civil projects like bridge piers and tunnel linings, main reinforcement bars often reach 32-40mm in diameter. The robust torque and extended wire length ensure the heavy steel is secured against the immense pressures of slip-form concrete pouring.
Use cases in raft foundations, threaded rebar, and three-bar ties
Raft foundations present a unique challenge, often requiring the tying of massive threaded rebar (36-50mm). The deep, horizontal nature of raft mats requires operators to work in a stooped posture, making the tool's weight and balance critical factors. Furthermore, raft foundations frequently feature longitudinal lap splices and three-bar ties.
As noted during the initial project data collection, automatic rebar tiers are engineered primarily for orthogonal (perpendicular) bar intersections, not parallel laps. The geometry for three-bar parallel ties is highly complex; the combined profile forms a bulky, triangular shape rather than a simple cross. While a 6-58mm (0.24-2.28in) tool mathematically covers the total diameter, parallel lap splices often exceed the machine’s intended application limits and challenge jaw closure. If parallel laps must be tied automatically, explicitly validating the machine's limits on-site is essential.
How bar spacing and access geometry affect suitability
Bar spacing and access geometry dictate whether a machine can physically reach the intersection. Tightly spaced shear reinforcement or complex corbel details restrict the entry of a large jaw. It is crucial to recognize that physical jaw width and nose geometry—not just the theoretical tying diameter—determine whether a machine can actually operate in congested reinforcement and dense beam-column joints.
If the tool's nose profile is too wide to slip between closely spaced bars, its high capacity is rendered useless. Evaluating the physical constraints of the rebar cage ensures the selected model can perform the required ties in situ.
How to Select the Right Machine
Translating technical theory into a procurement decision requires a rigorous workflow based on empirical data from the project's structural requirements. Methodically evaluating the required tying diameter range allows project managers to pinpoint the exact specifications needed to support daily production quotas.
Optimizing the interaction between the tool, the tying wire, and the steel reinforcement reduces labor costs, accelerates project timelines, and standardizes quality assurance.
Step-by-step workflow from bar diameter to machine class
Follow a strict five-step workflow to select the right machine. First, audit the project to compile all common rebar diameters and their intersection combinations. Second, verify that the maximum combined diameter falls safely within the tool's capacity. Third, evaluate the specifications: calculate the required wire length and assess how the resulting knots-per-coil will impact the frequency of reloading.
Fourth, confirm that the tool's torque output is sufficient for the largest steel diameters on the list. Finally, assess the site's physical constraints—such as bar spacing and accessibility—to ensure the tool's jaw geometry can maneuver effectively in the field.
How to evaluate productivity and tying speed
When evaluating productivity, look beyond theoretical maximums. While some manufacturer datasheets cite sub-second tying cycles, real-world output depends on operator pacing and site conditions. Even factoring in repositioning time, the automated approach offers a significant efficiency multiplier compared to skilled manual tying, which averages 5-8 seconds per knot.
Automation lowers the skill threshold required for the labor force and reduces training cycles—a strategic advantage in a market facing severe labor shortages. Furthermore, it mitigates the quality fluctuations caused by worker fatigue, ensuring more consistent torque across ties.
Quality assurance evidence to request
Robust quality assurance evidence must support the procurement. Reputable manufacturers provide independent mechanical test reports verifying torque consistency, wire feeding smoothness, and cutting reliability. Core components like bearings and dual motors should be backed by a substantial warranty. For those seeking verified equipment in this capacity range, reviewing market examples—such as an automatic tying tool for 6-58mm rebar—alongside independent test data provides a clear benchmark for evaluating product specifications.
Progressing systematically from the required diameter range to specific physical validations ensures the chosen equipment delivers measurable value on the job site.
Further reading:
Key Takeaways
- Select the rebar tying machine by total tying diameter first, not by nominal bar size alone.
- Allow capacity margin because ribbed, coated, angled, or lapped bars often exceed the simple arithmetic sum of their diameters.
- Use a 4-28mm class tool mainly for light mesh work, such as typical #3 to #3 intersections.
- Specify a 6-58mm class tool when structural cages include large bars, splice zones, three-bar ties, or congested column reinforcement.
- Audit bar bending schedules and site tie geometries before comparing models to prevent jaw jams, incomplete wraps, and productivity bottlenecks.
- Confirm that the tool supports the required wire length and wire diameter, typically around 0.8-1.2mm for many structural tying applications.
Frequently Asked Questions
Why is tying diameter range the first criterion when choosing a rebar tying machine?
It determines whether the tool jaw, wire feed, and torque can fully wrap the actual rebar intersection without jams, incomplete ties, or excess wire waste.
Is total tying diameter the same as nominal bar size added together?
No. Rib height, coatings, crossing angle, and lap geometry can make the real tying footprint larger than the simple sum of two bar diameters.
When is a 6-58mm rebar tier class appropriate?
It is appropriate for structural work with larger intersections, splice zones, column cages, multi-bar ties, or sites where #8 or similarly heavy bars may be tied.
Would a 4-28mm tool be enough for light mesh work?
Yes, if most ties are small, simple intersections such as #3 to #3 mesh. Confirm schedules first to avoid under-sizing the tool for heavier zones.
What project data should be checked before selecting a rebar tying tool?
Review bar bending schedules, maximum intersecting bar sizes, lap zones, three-bar ties, non-orthogonal ties, coating thickness, and access restrictions.