Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


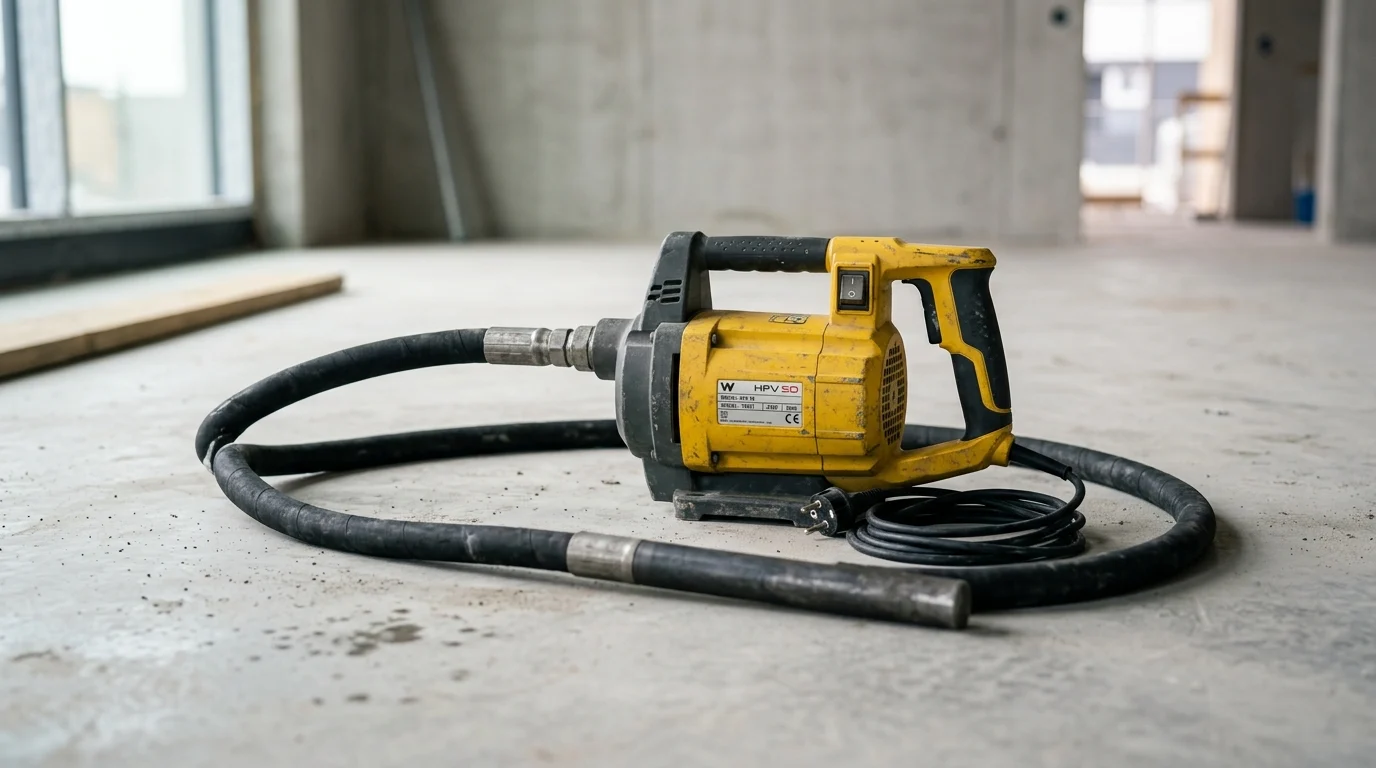
In reinforced concrete work, a small amount of trapped air can become a major structural liability. Fresh concrete may contain substantial entrapped air, and even a 1% void increase can reduce strength by roughly 5% to 6%. That is why high-frequency Concrete Vibratorsmatter on demanding pours, especially where dense rebar cages, deep lifts, and low-slump mixes make consolidation difficult. This article explains how high-frequency internal vibration improves paste flow, strengthens the bond around reinforcing steel, and reduces defects such as honeycombing, cold joints, and void pockets. It also compares high-frequency performance with standard vibrators so contractors can choose equipment that supports safer, denser, and more durable concrete.
Why High-Frequency Concrete Vibrators Matter in Reinforced Concrete
The structural integrity of reinforced concrete relies fundamentally on proper consolidation. When concrete is poured into formwork, it typically contains up to 20% entrapped air by volume. Without adequate internal vibration to expel this air, the voids remain trapped within the matrix, severely compromising the bond between the concrete and the reinforcing steel.
In modern construction, where architectural demands and heavy structural loads necessitate highly congested rebar cages, standard vibration techniques often fall short. High-frequency internal concrete vibrators (sometimes referred to regionally as "high-cycle" vibrators) have emerged as a critical tool for overcoming these barriers. Unlike external form vibrators or surface screeds, these internal tools utilize advanced motor technology and optimized frequencies to fluidize the mix more efficiently in challenging structural environments.
Project Risks They Reduce
Entrapped air voids reduce the compressive strength of concrete significantly. Industry guidelines and structural testing indicate that just 1% of entrapped air can cause a 5% to 6% reduction in overall structural strength. High-frequency vibrators mitigate this risk by rapidly liquefying the mortar phase of the mix, allowing trapped air bubbles to break their surface tension and rise to the top of the pour.
Furthermore, proper high-frequency consolidation drastically reduces the incidence of weak spots and cold joints in deep structural lifts. By ensuring a uniform distribution of the cement paste, high-frequency units prevent the formation of structural flaws that would otherwise require costly epoxy injections, structural patching, or even demolition of the affected element.
How They Differ from Standard Concrete Vibrators
The primary differentiator between vibrator categories lies in their mechanical operation and their vibrations per minute (vpm). Standard pendulum or flexible-shaft vibrators typically operate between 9,000 and 11,000 vpm. In contrast, high-frequency concrete vibrators operate at significantly faster speeds, generally between 12,000 and 17,000 vpm (approximately 200 to 280 Hz).
Mechanically, standard vibrators rely on an external combustion or electric motor that transfers rotational energy through a long flexible shaft. This design inherently loses rotational speed and efficiency under the heavy friction and load of wet concrete. High-frequency vibrators, however, frequently utilize a motor-in-head design. This configuration places a miniaturized, high-speed electric motor directly inside the steel vibrator head. As a result, the frequency remains exceptionally stable and continuous, even when submerged in dense, low-slump concrete mixes.
How High-Frequency Vibrators Improve Concrete Consolidation
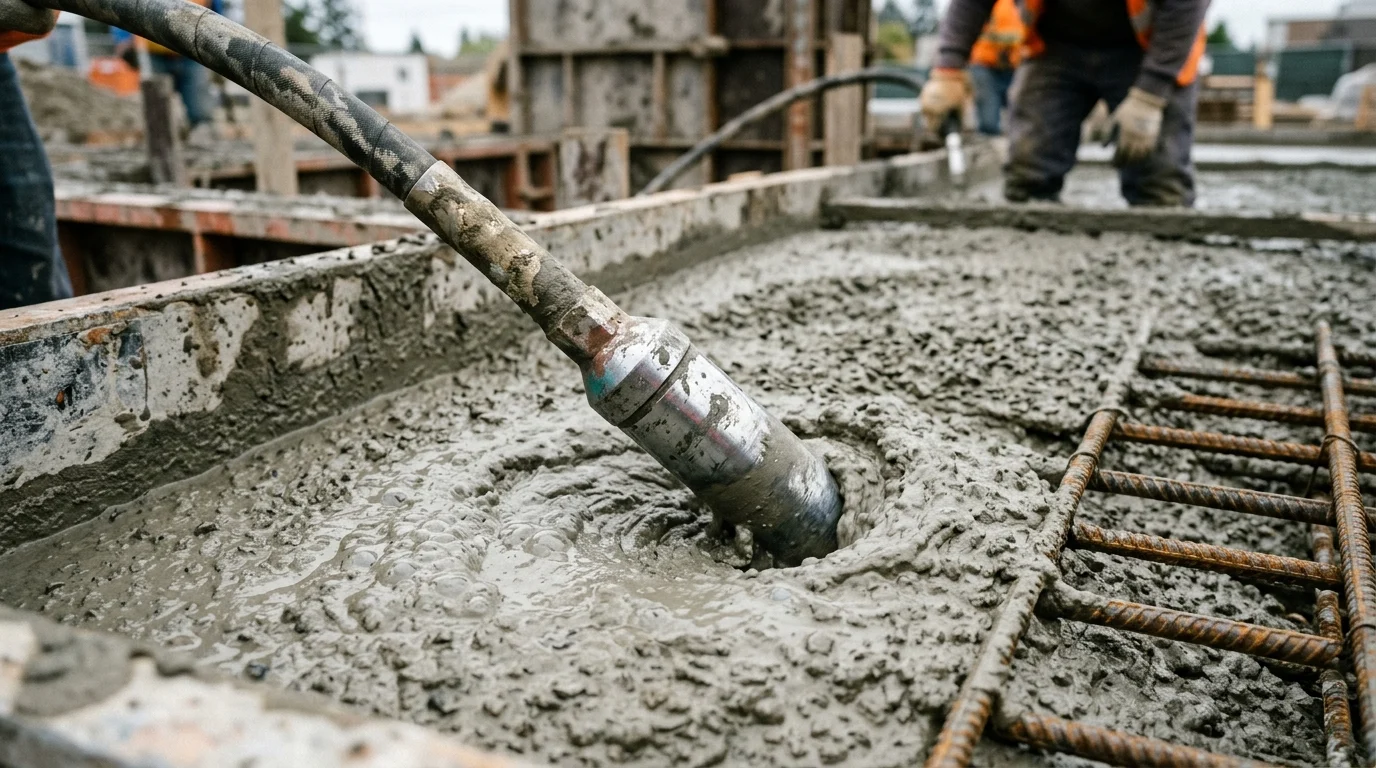
The physics of concrete consolidation dictates that different vibration parameters affect different components of the concrete mix. While amplitude (the physical distance the vibrator head swings) is primarily responsible for moving heavy, coarse aggregates, frequency is the driving force behind the fluidization of the sand and cement mortar.
High-frequency internal vibrators excel in manipulating this mortar phase. By maintaining a rapid, consistent vibration, they break down the internal friction of the mix, which is essential for achieving a dense, impermeable finish in heavily reinforced structures.
Frequency, Amplitude, and Vibration Performance
Operating at these elevated speeds with a relatively low amplitude (typically ranging from 1.0 mm to 2.5 mm) creates a highly localized zone of liquefaction. This specific dynamic allows the mortar to flow seamlessly around complex rebar geometries without displacing the heavy aggregates.
This careful balance prevents the segregation of the mix, a common problem when high-amplitude, low-frequency vibrators over-agitate the concrete, causing coarse aggregates to sink to the bottom of the formwork. The sustained high frequency ensures that the internal yield stress of the mix is rapidly broken down, facilitating optimal compaction while maintaining the homogeneity of the concrete design.
Defects They Help Prevent
High-frequency vibrators are instrumental in preventing major structural and surface defects, streamlining the mitigation of issues like honeycombing and bug holes into a single operational process. Honeycombing occurs when coarse aggregates cluster together without sufficient mortar to bind them—a frequent and dangerous issue in densely reinforced zones. Bug holes (surface air voids) present both a major aesthetic failure for exposed architectural concrete and a vulnerability to freeze-thaw cycles.
By maintaining rapid vibration, these tools excite the microscopic air bubbles that cling stubbornly to the formwork and the reinforcing steel, driving them to the surface. Empirical data from precast manufacturing operations demonstrates that utilizing high-frequency vibration can often reduce surface void ratios to below 0.5%, significantly minimizing the need for labor-intensive post-pour sacking, rubbing, and patching.
Limits in Low-Slump and Dense Reinforcement Conditions
Despite their high efficiency, high-frequency vibrators possess distinct operational boundaries and limitations. In extremely low-slump concrete (where the slump is less than 25 mm), the reduced amplitude of a high-frequency head may struggle to effectively move the rigid mass of coarse aggregates, potentially leading to incomplete consolidation. Conversely, in highly fluid pump mixes, excessive high-frequency vibration can inadvertently cause segregation if the head is left in place too long.
Heat generation is another critical factor. Motor-in-head units rely on the surrounding wet concrete for cooling; in large, continuous pours, they are susceptible to overheating if withdrawn too slowly or operated out of the mix. In ultra-dense reinforcement scenarios where the clear spacing between steel bars is less than 40 mm, even the smallest high-frequency heads—which are available down to 30 mm in diameter—risk becoming wedged. In such extreme conditions, structural engineers often specify self-consolidating concrete (SCC) rather than relying solely on mechanical internal vibration.
Beyond physical constraints, high-frequency units demand reliable power infrastructure and are sensitive to voltage fluctuations. The sophisticated electronic components and built-in inverters also mean that when breakdowns occur, repair and maintenance costs are notably higher than those of simple mechanical shafts.
How to Compare High-Frequency and Standard Concrete Vibrators
Selecting the appropriate consolidation equipment requires a rigorous comparison between standard flexible-shaft vibrators and high-frequency motor-in-head units. Evaluating performance metrics, specific project applications, and long-term economic impacts is necessary to optimize equipment fleets.
Understanding these trade-offs ensures that the right tool is deployed for the right structural element, preventing both over-investment in simple pours and under-performance in critical structural zones.
Key Performance Criteria
When evaluating concrete vibrators, the effective radius of action and the ability to maintain frequency under load are paramount criteria. Standard vibrators frequently experience a 15% to 20% drop in vpm when plunged into dense concrete, reducing their compaction efficiency. Conversely, high-frequency motor-in-head units typically maintain their operational speed within a tight 3% to 5% margin, ensuring consistent energy transfer.
| Feature | Standard Flexible-Shaft Vibrator | High-Frequency Motor-in-Head |
|---|---|---|
| Operating Frequency | 9,000 – 11,000 vpm | 12,000 – 17,000 vpm |
| Frequency Loss Under Load | 15% – 20% drop | 3% – 5% drop |
| Amplitude Profile | High (moves large aggregate) | Low-to-Medium (fluidizes mortar) |
| Drive Mechanism | External motor via flex shaft | Internal miniaturized electric motor |
| Best Suited For | Flatwork, footings, low-rebar walls | Congested rebar, architectural finishes |
Best Use Cases for Reinforced Concrete
Standard vibrators remain highly effective for slab-on-grade construction, massive footings, and mass concrete placements where reinforcement is sparse and high amplitude is required to move large aggregate particles over wider areas.
Conversely, high-frequency vibrators are indispensable for highly engineered structures. Their primary use cases include high-rise shear walls, bridge pylons, precast concrete manufacturing, and any application requiring a Class A architectural finish. The ability to snake a high-frequency head through congested post-tensioning cables and dense rebar cages without losing consolidation power makes them the definitive standard for critical infrastructure projects.
Cost, Productivity, and Quality Trade-Offs
The initial capital expenditure for a high-frequency vibrator system is notably higher than for standard alternatives. A complete high-frequency setup, including the necessary electronic frequency converter, typically costs between $1,500 and $3,000—often estimated at 40% to 60% more than a standard mechanical vibrator.
However, the productivity gains and quality improvements can rapidly offset this initial premium. High-frequency units consolidate concrete up to 20% faster per insertion, reducing active labor hours during the pour. More importantly, the reduction in post-pour rework yields substantial economic savings. Depending on the region and severity, contractors historically estimate that patching structural defects and fixing aesthetic blemishes can cost $30 to $50 per square meter; eliminating this rework helps amortize the higher cost of the advanced equipment.
How to Specify and Deploy High-Frequency Concrete Vibrators
Successful deployment of high-frequency concrete vibrators requires strict adherence to industry specifications and rigorous field protocols. Even the most advanced equipment will fail to achieve the desired concrete densities if specified incorrectly for the rebar layout or operated by untrained personnel.
Bridging the gap between equipment procurement and field execution requires establishing clear operating guidelines based on the specific geometry of the pour.
Selection Specifications to Check
Specifying the correct vibrator head size and centrifugal force is the first critical step. According to general industry guidelines such as ACI 309R, the vibrator head diameter should be the largest practical size that can pass through the rebar cage while maintaining a minimum clearance of 25 mm. High-frequency heads typically range from 30 mm to 65 mm.
| Head Diameter | Minimum Clear Rebar Spacing | Approx. Radius of Action | Compaction Rate (m³/hr) |
|---|---|---|---|
| 30 mm – 35 mm | 40 mm | 100 mm – 150 mm | 5 – 10 |
| 40 mm – 45 mm | 55 mm | 150 mm – 200 mm | 10 – 20 |
| 50 mm – 55 mm | 65 mm | 200 mm – 300 mm | 15 – 25 |
| 60 mm – 65 mm | 80 mm | 300 mm – 400 mm | 25 – 35 |
Verifying power source requirements is also essential. Modern high-frequency vibrators either require an external frequency converter (inverter) to step up standard grid power to 200 Hz, or they feature built-in electronic converters housed within the switch box. While built-in units offer greater mobility on the deck, their sensitive electronics are vulnerable to concrete ingress, moisture damage, and rough handling, often leading to costly and complex field repairs compared to the rugged simplicity of standard mechanical shafts.
Insertion Spacing and Operating Practices
The operational technique for high-frequency vibrators is rigid and requires discipline. The vibrator head should be inserted rapidly under its own weight to the bottom of the concrete lift, ensuring it penetrates at least 150 mm into the previously placed, still-plastic layer to prevent the formation of cold joints.
The insertions must follow a systematic grid, spaced closely together—typically every 400 mm to 500 mm—ensuring that the radius of action overlaps by at least 100 mm to 150 mm. The withdrawal process is the most critical phase for preventing voids: the head must be pulled up slowly at a continuous rate of approximately 25 mm to 75 mm per second. This slow withdrawal allows the mortar to flow back into the space vacated by the vibrating head, preventing the formation of a trapped air pocket or "rat hole."
Documentation and Quality Control
For critical structural elements, active documentation of the vibration process is highly recommended. This includes mapping the insertion grid and logging the time spent per insertion, which typically ranges from 5 to 15 seconds depending on the mix design, slump, and head diameter.
Advanced high-frequency systems now incorporate digital monitoring capabilities, allowing site managers to track exact runtimes, frequency stability under load, and motor temperatures via Bluetooth or RFID. If the frequency drops by more than 5% during an insertion, it may indicate that the concrete is losing its plasticity, that the mix is too stiff, or that the vibrator is undersized for the aggregate mass. This data prompts an immediate review of the pouring sequence to prevent structural failures.
How to Decide If High-Frequency Vibration Is Worth It
The decision to upgrade from standard to high-frequency concrete vibrators hinges on a careful analysis of structural requirements, safety regulations, and project economics. While not necessary for every flatwork pour, high-frequency vibration provides a definitive competitive edge in complex structural environments.
Evaluating whether the demands of a specific project portfolio justify the transition to advanced consolidation technology is a critical step in equipment planning.
Applications That Justify High-Frequency Vibration
High-frequency vibration is fully justified—and often mandated by structural specifications—in the construction of liquid natural gas (LNG) containment tanks, nuclear power facilities, and municipal water treatment plants. In these harsh environments, concrete impermeability is a critical safety and durability factor.
A void-free concrete matrix prevents the ingress of chlorides and moisture, which are the primary causes of rebar corrosion and concrete spalling. For these high-stakes applications, achieving a residual air content of less than 1.5% is a common stringent specification that standard flexible-shaft vibrators struggle to meet consistently. Furthermore, precast concrete plants across many industrialized sectors widely adopt high-frequency systems to maintain rapid production cycles, achieve high early strength, and deliver flawless architectural finishes right out of the mold.
Safety, Compliance, and Training Needs
Operator health and safety are increasingly major drivers in the adoption of high-frequency equipment. Prolonged exposure to the intense vibrations of standard equipment can lead to Hand-Arm Vibration Syndrome (HAVS), a debilitating occupational injury that affects the nerves and blood vessels in the hands and arms.
High-frequency vibrators, particularly motor-in-head models, transmit less vibration back through the handling hose to the operator. Premium units are engineered with shock-absorbing components designed to keep operator vibration exposure below regulatory action values (such as 2.5 m/s² in many jurisdictions) for an 8-hour working shift.
However, this does not eliminate the need for safety protocols; active vibration monitoring and strict maintenance of rubber dampeners are still required. Furthermore, motor-in-head designs introduce different ergonomic challenges: the steel heads are significantly heavier, and the internal wiring makes the handling hoses stiffer and more cumbersome to maneuver. Consequently, targeted training is necessary to ensure personnel can safely handle the equipment's weight while executing the specific insertion speeds and overlap requirements unique to high-frequency tools.
Balancing Quality Gains with Project Cost
Ultimately, the justification for high-frequency vibrators comes down to a comprehensive total cost of ownership and risk mitigation analysis. If a commercial project involves massive volumes of highly reinforced structural concrete, the cost of cosmetic repairs, structural patching, and potential timeline delays due to rejected pours far outweighs the capital investment in advanced vibration equipment.
To determine if high-frequency vibration is the right choice, project teams should apply the following decision checklist:
- Assess Structural Complexity: Mandate high-frequency units if the pour involves highly congested rebar, complex post-tensioning cables, or strict Class A architectural finish requirements.
- Evaluate Power Infrastructure:Confirm the site can reliably support sensitive electronic frequency converters without damaging voltage drops, or budget for specialized remote Generators.
- Analyze Mix Design Compatibility: Ensure the specified concrete is not an ultra-low slump mix (which resists low-amplitude vibration) or a highly fluid pump mix that is prone to segregation under high frequencies.
- Calculate Rework ROI: Compare the higher initial equipment and maintenance costs against projected savings from reduced patching; contractors frequently report significant improvements in defect rates that justify the premium.
Contractors who systematically evaluate these factors consistently find that high-frequency vibration is a strategic necessity for high-performance concrete construction.
Key Takeaways
- Use high-frequency internal vibrators in reinforced concrete to remove entrapped air that can account for up to 20% of fresh concrete volume.
- Prevent strength loss by consolidating thoroughly, because each 1% of entrapped air can reduce concrete strength by roughly 5% to 6%.
- Select high-frequency units operating around 12,000 to 17,000 vpm when standard 9,000 to 11,000 vpm vibrators may not penetrate dense rebar zones effectively.
- Consider motor-in-head vibrator designs for low-slump or heavily congested pours because they maintain more stable frequency under load.
- Apply proper internal vibration to reduce honeycombing, cold joints, patching, epoxy repair, and potential demolition of defective reinforced concrete elements.
Frequently Asked Questions
What is a high-frequency concrete vibrator used for?
It is used to consolidate freshly placed reinforced concrete by removing entrapped air, improving paste flow around rebar, and reducing voids, honeycombing, and weak spots in structural pours.
How fast does a high-frequency concrete vibrator operate?
High-frequency models typically operate around 12,000 to 17,000 vibrations per minute, compared with about 9,000 to 11,000 vpm for many standard flexible-shaft vibrators.
Why is vibration important in reinforced concrete?
Fresh concrete can contain significant entrapped air. If voids remain, they weaken compressive strength and reduce the bond between concrete and reinforcing steel, especially in congested rebar cages.
Can high-frequency vibration improve concrete strength?
Yes. Proper consolidation helps remove air voids; even 1% entrapped air can reduce concrete strength by about 5% to 6%, so effective vibration directly supports structural performance.
Is a motor-in-head vibrator better for low-slump concrete?
Often, yes. Motor-in-head designs maintain stable frequency inside dense or low-slump mixes because the motor is located in the vibrator head rather than losing energy through a long flexible shaft.