Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


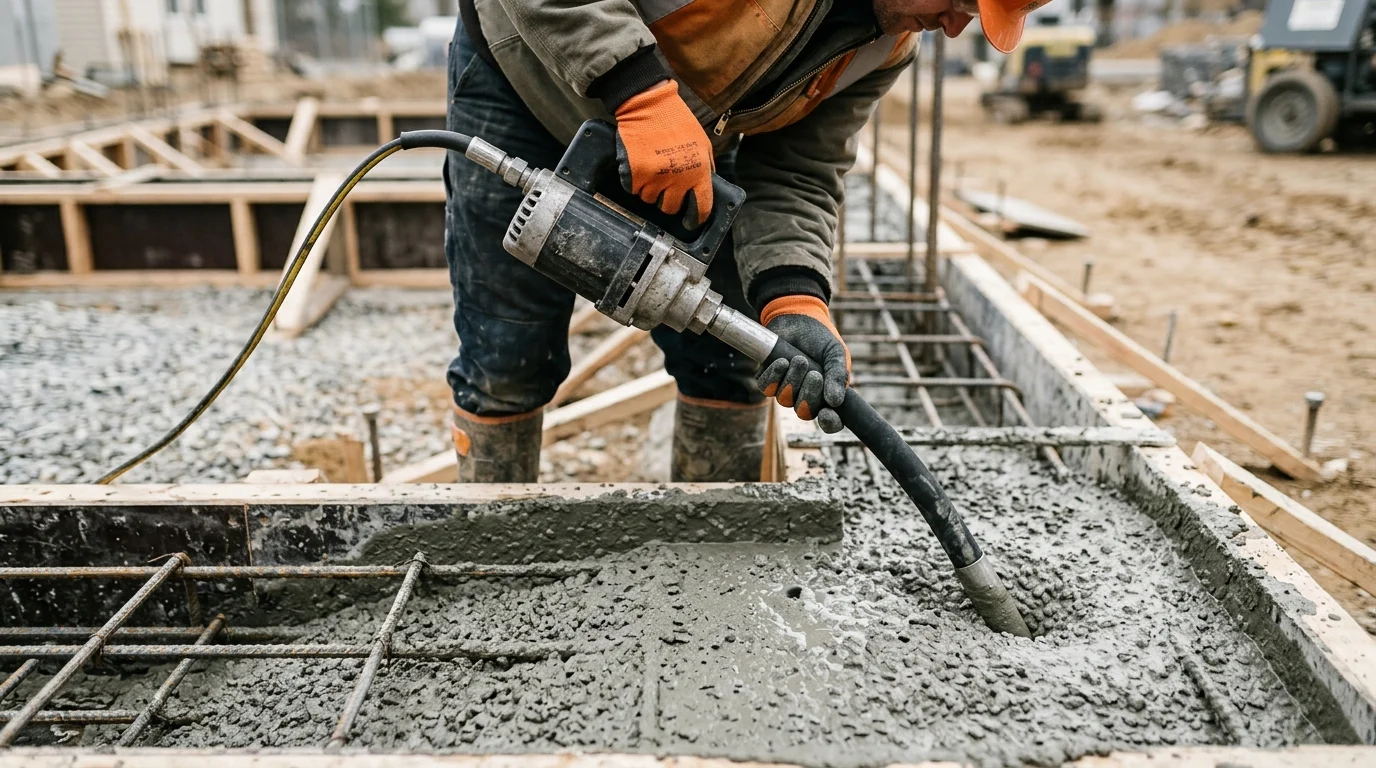
Poorly consolidated concrete can hide costly problems long before cracks or surface defects appear. Fresh concrete may contain 5% to 20% entrapped air, and those voids can compromise strength, durability, reinforcement bonding, and finish quality. A high frequency concrete vibrator solves this by rapidly liquefying the mix, helping aggregate settle and air rise before the concrete sets. For contractors working on structural slabs, columns, walls, and commercial pours, the right vibration method can mean fewer honeycombs, fewer bug holes, stronger hardened concrete, and less remedial patching. This guide explains how high frequency vibration works, why it matters, and what quality improvements it can deliver on site.
Why High Frequency Concrete Vibrators Matter
Concrete consolidation is a critical phase in structural construction, dictating the ultimate durability, strength, and aesthetic finish of the cured material. When concrete is initially poured, internal friction between coarse aggregate particles prevents the mix from naturally settling into a dense configuration. This freshly placed concrete typically contains between 5% and 20% entrapped air by volume, appearing as irregular voids and pockets.
Mechanical vibration temporarily overcomes this internal friction, transforming the concrete mix from a plastic state into a highly fluid, workable liquid. High frequency concrete vibrators are specialized tools engineered to deliver rapid, localized kinetic energy to the mix. By operating at elevated rotational speeds, these devices accelerate the consolidation process, ensuring that the concrete completely fills the formwork, encapsulates reinforcing steel, and expels detrimental air voids.
How vibration improves concrete quality
The primary mechanism of vibration relies on inducing thixotropy—the property of certain gels or fluids to become less viscous when subjected to mechanical stress. As the High Frequency Vibrator transmits energy waves through the mix, the mortar fraction liquefies, drastically reducing the yield stress of the concrete.
This liquefaction serves two immediate purposes: it allows heavy aggregates to settle into a tightly packed matrix under the influence of gravity, and it forces lighter entrapped air bubbles to rise to the surface. The impact on structural performance is profound. Industry studies demonstrate that for every 1% of entrapped air removed from the concrete matrix, the compressive strength of the cured concrete increases by approximately 5%. A properly vibrated pour will typically reduce the entrapped air volume to a structurally negligible 1% to 3%.
Common defects reduced by proper vibration
Inadequate consolidation directly causes several expensive and structurally compromising defects. Honeycombing occurs when coarse aggregates cluster together without sufficient mortar to fill the interstitial spaces, leaving exposed rock and deep voids. Bug holes (surface air voids) manifest as small cavities on the vertical faces of cast-in-place concrete, severely degrading architectural finishes.
Cold joints are another severe defect, occurring when a newly poured lift of concrete fails to seamlessly integrate with the preceding lift before initial set. By utilizing high frequency vibration to penetrate the boundary layer between lifts, the aggregate and mortar are mechanically intermixed, preventing the formation of weak planar interfaces. Proper vibrator application reduces surface patching requirements, which can otherwise cost contractors between $5 and $10 per square foot in post-pour remedial labor.
Why commercial projects require consistent consolidation
Commercial and heavy civil projects impose rigorous demands on concrete performance, often utilizing high-strength, low-water-to-cement ratio mixes. These highly viscous mixes resist natural flow and require immense mechanical energy for proper placement. Standards such as the American Concrete Institute (ACI) 309R, "Guide for Consolidation of Concrete," mandate specific protocols to ensure uniformity across large-scale pours.
Consistent consolidation guarantees that the structural member performs exactly as modeled by the engineering team. In elements subjected to high dynamic loads or aggressive environmental exposures—such as bridge piers, retaining walls, and marine structures—uniform density prevents localized weakness and inhibits the ingress of corrosive chlorides toward the reinforcing steel. High frequency vibrators provide the reliable, repeatable energy output necessary to meet these strict commercial compliance metrics.
How High Frequency Concrete Vibrators Work
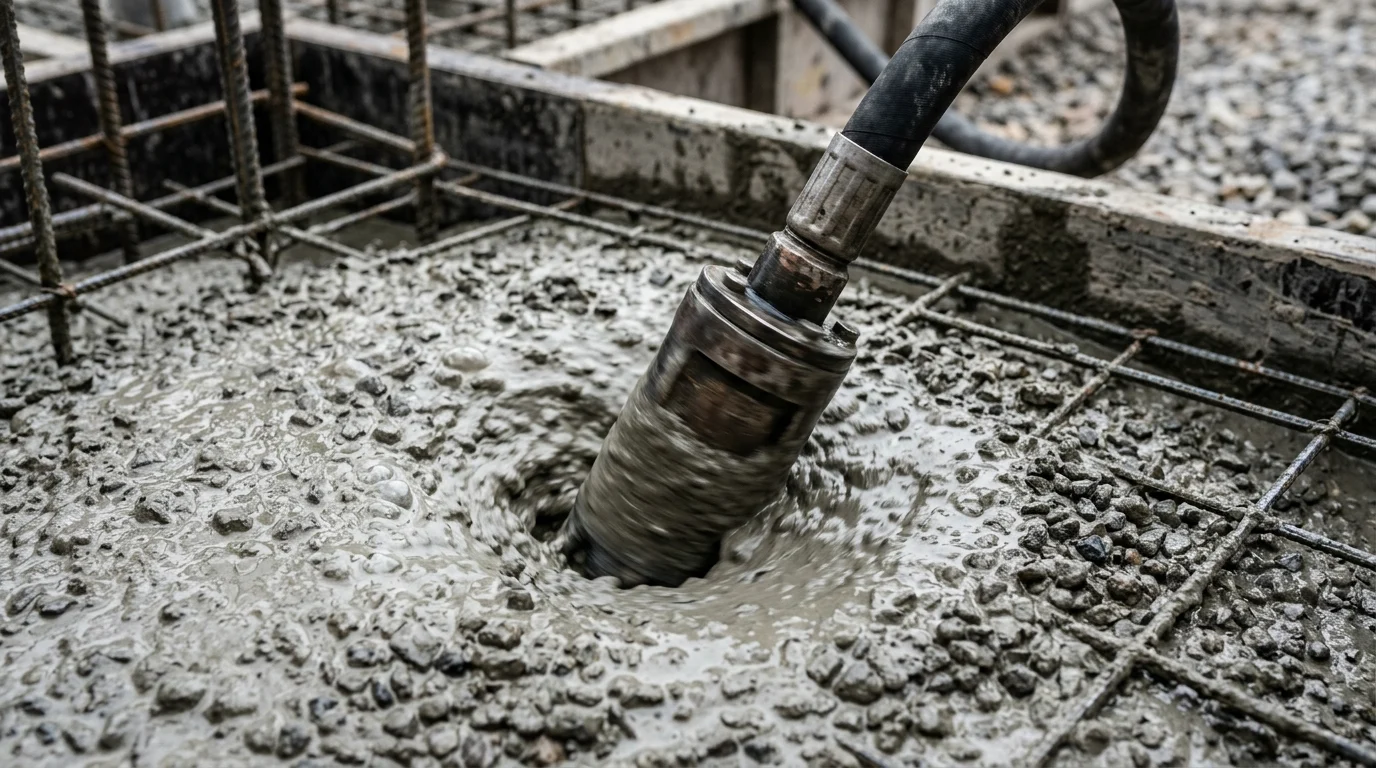
High frequency Concrete Vibrators operate on the principles of dynamic energy transfer, utilizing eccentric weights driven by high-speed motors. The effectiveness of any vibrator is determined by the interplay between its frequency (the number of vibration cycles per minute) and its amplitude (the maximum distance the vibrator head deviates from its resting axis).
Understanding the physics behind these tools is essential for optimizing their deployment on site. The generated kinetic energy propagates outward from the vibrator head as compressive waves, creating an effective radius of action that dictates the required spacing and insertion patterns during the pour.
Key features of high frequency vibration
The defining characteristic of a high frequency vibrator is its rotational speed. While standard vibrators operate at roughly 8,000 to 10,000 vibrations per minute (vpm), high frequency models typically run between 12,000 and 17,000 vpm. This elevated frequency is achieved through direct-drive electric motors integrated into the vibrator head or via specialized pneumatic rotors.
The high vpm specifically targets the finer particles in the concrete mix—the sand and cement paste. By vibrating at a frequency that resonates with these smaller mass particles, the tool rapidly decreases the viscosity of the mortar. Despite the high frequency, these units are engineered to maintain a precise, calculated amplitude (often between 0.04 and 0.08 inches) to ensure sufficient energy is transmitted without causing the mix to segregate.
How internal vibration moves aggregate and air
The internal vibration process occurs in two distinct, sequential stages: initial subsidence and de-aeration. During initial subsidence, the high-frequency waves disrupt the bridging of coarse aggregates. Gravity pulls the heavier stones downward, causing the concrete surface to slump rapidly and fill the contours of the formwork.
Once subsidence is complete, the de-aeration phase begins. The liquefied mortar permits entrapped air bubbles to coalesce and migrate upward. Because of the high frequency, these bubbles are agitated and freed from the aggregate surfaces, rising at an average rate of 1 to 3 inches per second. The operator must maintain the vibrator's position long enough for this de-aeration to complete, visually confirming the process when bubbles cease breaking at the surface and a thin sheen of mortar appears.
Internal versus external vibrator applications
Internal (immersion or poker) vibrators are the standard choice for the vast majority of concrete placements. They are plunged directly into the plastic mix, transferring energy with maximum efficiency since the waves propagate 360 degrees outward into the material. However, internal vibration is not viable in all scenarios.
External (form) vibrators are clamped directly to the exterior of the formwork. They are deployed when heavy rebar congestion—such as a grid of #8 reinforcing bars at tight 2-inch spacing—physically blocks the insertion of an internal vibrator. External units require rigid, structurally reinforced formwork to withstand the intense vibrational forces without deflecting or failing. While internal vibrators are more energy-efficient,external high-frequency vibrators are indispensable for heavily reinforced architectural precast elements and complex tunnel linings.
High Frequency Versus Conventional Vibrators
Selecting the appropriate consolidation equipment requires a technical evaluation of the concrete mix design and the structural configuration of the formwork. Contractors must routinely decide between high frequency vibrators and conventional low-frequency models, balancing the need for rapid mortar liquefaction against the physical movement of large aggregates.
While standard vibrators are sufficient for high-slump, easily workable residential flatwork, commercial specifications increasingly demand the unique rheological modifications provided by high frequency equipment. The distinction lies primarily in how the differing wavelengths interact with the mass of the concrete constituents.
Performance differences contractors should compare
Conventional vibrators rely on higher amplitude and lower frequency to physically punch through stiff mixes and move large, heavy aggregates. In contrast, high frequency vibrators prioritize rapid oscillations to fluidize the cement paste, creating a low-friction environment where aggregates settle naturally. Contractors must match the vibrator's output to the mix's aggregate size and slump.
| Metric | High Frequency Vibrator | Conventional Vibrator |
|---|---|---|
| Operating Frequency | 12,000 – 17,000 vpm | 8,000 – 10,000 vpm |
| Typical Amplitude | 0.03 – 0.08 inches | 0.06 – 0.12 inches |
| Primary Action | Liquefies mortar, rapid de-aeration | Moves large aggregate, mass consolidation |
| Ideal Mix Slump | Low to medium (1 – 4 inches) | Medium to high (3 – 6+ inches) |
| Surface Finish Quality | Exceptional (minimal bug holes) | Standard (requires moderate finishing) |
By comparing these metrics, project managers can optimize labor efficiency. High frequency units generally achieve de-aeration 20% to 30% faster in stiff mixes, directly increasing the pace of the pour and reducing the physical strain on operators.
Best uses for reinforced and dense concrete
Structural members designed to carry immense loads, such as shear walls and transfer beams, are characterized by dense rebar cages and low-water mixes. These low-slump concretes (often yielding a slump test result of less than 3 inches) possess high yield stress and are prone to honeycombing if improperly vibrated.
High frequency vibrators are the optimal choice for these conditions. The rapid oscillations easily penetrate the narrow gaps between tightly spaced rebar, fluidizing the paste so it flows seamlessly around the steel. This ensures a flawless mechanical bond between the concrete and the reinforcement, a critical factor for transferring tensile stresses. Furthermore, the localized fluidization prevents the coarse aggregate from segregating and accumulating against the rebar, a common issue when using high-amplitude conventional vibrators in congested forms.
Cost, productivity, and durability trade-offs
The procurement of high frequency equipment involves distinct financial and operational trade-offs. Upfront capital expenditures for high-frequency units are generally 30% to 50% higher than those for standard flex-shaft vibrators, driven by the cost of precision micro-motors or specialized high-cycle inverters.
However, this initial premium is rapidly offset by productivity gains and reduced rework. Because high frequency vibrators consolidate concrete faster and produce superior architectural finishes, contractors save significantly on post-pour cosmetic repairs. Additionally, high-frequency units with motor-in-head designs eliminate the mechanical flex shaft, a component highly susceptible to wear and tear in conventional models. This reduction in moving parts extends the mean time between failures (MTBF) and lowers long-term maintenance costs.
Key Specifications and Site Practices
Successful concrete consolidation is not solely dependent on the equipment; it relies heavily on precise execution and adherence to established operational parameters. The interaction between the vibrator's specifications and the operator's technique dictates the final quality of the structural member.
Site engineers must establish a systematic vibration plan that accounts for the geometry of the pour, the depth of the lifts, and the specific rheology of the concrete mix. Haphazard insertion patterns or incorrect timing can easily lead to under-vibration (leaving voids) or over-vibration (causing segregation).
Frequency, amplitude, head size, and power requirements
To achieve optimal consolidation, the vibrator's physical dimensions and power output must be scaled to the task. Vibrator head diameters typically range from 3/4 inch for narrow, congested forms up to 3 inches or more for massive civil placements. A standard 2-inch high-frequency head might draw 15 to 20 amps and generate an effective radius of action spanning 7 to 14 inches radially from the center of the tool.
Power sources also dictate site logistics. High-cycle electric vibrators often require specialized generators that output 180 Hz to 200 Hz current, while pneumatic vibrators demand robust air compressors capable of delivering 40 to 80 cubic feet per minute (CFM) at 90 to 100 PSI. Matching the power supply to the vibrator specifications ensures the unit does not experience a voltage or pressure drop under load, which would drastically reduce the operating frequency.
Proper insertion, spacing, and withdrawal techniques
The geometry of the insertion pattern is critical. The vibrator must be inserted vertically, allowing gravity to assist the penetration and ensuring the energy radiates evenly in a horizontal plane. Inserting the vibrator at an angle can cause the head to drag against rebar, potentially damaging the equipment and leaving localized zones of unconsolidated concrete.
Spacing between insertions should be approximately 1.5 times the radius of action. If a 2-inch head has a 10-inch radius of action, insertions should occur every 15 inches to ensure overlapping zones of influence. Furthermore, the vibrator must be allowed to sink rapidly to the bottom of the lift, penetrating the previous, still-plastic lift by roughly 6 inches to knit the layers together. Withdrawal must be slow and deliberate—approximately 1 inch per second—to allow the liquefied mortar to flow back and close the hole left by the vibrator head.
How mix design, slump, and aggregate size affect results
The behavior of concrete under vibration is highly sensitive to its mix design. Mixes with a high proportion of coarse aggregate and a low slump (1 to 2 inches) possess high internal friction. These stiff mixes require longer vibration times—sometimes up to 15 seconds per insertion—to fully liquefy and release entrapped air.
Conversely, high-slump mixes or those incorporating superplasticizers (chemical admixtures that increase flowability) require significantly less vibration. Applying high-frequency vibration to a highly fluid mix for too long will cause dynamic segregation: the heavy coarse aggregates will sink rapidly to the bottom of the form, while the lighter water and cement paste (laitance) will rise to the surface. This creates a weak, dusting surface and a structurally compromised base. Operators must constantly read the surface of the concrete, halting vibration the moment the surface becomes glossy and large air bubbles cease escaping.
How to Choose the Right Vibrator
Procuring the right concrete consolidation equipment requires a comprehensive analysis of project demands, lifecycle costs, and quality assurance protocols. For contractors managing diverse portfolios ranging from basic foundations to complex architectural superstructures, standardizing on a specific type of vibrator impacts both the bottom line and compliance with structural codes.
Decision-makers must evaluate whether the rigorous demands of their typical projects justify the investment in high frequency technology, and how to verify that the equipment is performing to specification in the field.
Ownership cost, rental value, and maintenance needs
The financial modeling for vibrator acquisition must account for initial capital expenditure (CapEx), daily operational costs, and ongoing maintenance. While conventional flex-shaft vibrators are inexpensive commodities, high-frequency units represent a more significant investment. An electric motor-in-head high-frequency vibrator typically costs between $1,200 and $2,500, whereas standard units may cost $400 to $800.
| Cost / Maintenance Factor | High Frequency (Motor-in-Head) | Conventional (Flex-Shaft) |
|---|---|---|
| Average Purchase Price | $1,200 – $2,500 | $400 – $800 |
| Average Daily Rental Rate | $60 – $90 | $30 – $50 |
| Primary Maintenance Focus | Stator/Rotor, Cable integrity | Flex-shaft lubrication, Brushes |
| Bearing Inspection Interval | Every 200 – 300 operating hours | Every 100 operating hours |
| Lifespan Expectancy | 3 to 5 years (heavy use) | 1 to 3 years (heavy use) |
For contractors with sporadic needs for high-performance consolidation, renting at $60 to $90 per day is highly cost-effective. However, for specialized concrete contractors, the extended lifespan and reduced mechanical maintenance of high-frequency units yield a lower total cost of ownership over a 5-year horizon.
Quality control and compliance checks
In highly regulated sectors such as nuclear, aerospace, and heavy civil infrastructure, quality control extends beyond the concrete mix to the equipment itself. Inspectors operating under ACI 301 ("Specifications for Structural Concrete") may require contractors to prove that their vibrators are operating within the specified frequency range while submerged in the concrete.
To ensure compliance, quality control technicians utilize vibrating reed tachometers or advanced digital frequency meters. A critical compliance check is measuring the RPM drop under load. A high-quality, high-frequency vibrator should not experience a frequency drop exceeding 10% when plunged into a stiff mix. If a unit rated for 12,000 vpm drops below 10,800 vpm under load, it indicates inadequate motor torque, requiring immediate replacement to prevent substandard consolidation.
When a high frequency vibrator is the best choice
The decision to mandate a high frequency vibrator ultimately hinges on the required performance of the finished concrete. If the project involves slip-form paving, architectural precast panels, or heavily congested structural columns, high frequency vibration is not merely an option—it is a technical necessity.
These specialized units excel where surface aesthetics and absolute structural density are non-negotiable. By rapidly fluidizing the cement paste without displacing large aggregate matrices, high frequency vibrators ensure that complex formwork is filled flawlessly, rebar is tightly encapsulated, and the resulting concrete achieves its maximum designed compressive strength and durability.
Key Takeaways
- Use high frequency vibration to reduce entrapped air in fresh concrete from as much as 5% to 20% down to about 1% to 3%.
- Apply vibration consistently because every 1% of entrapped air removed can increase concrete compressive strength by approximately 5%.
- Penetrate between concrete lifts with the vibrator to help blend layers and reduce the risk of weak cold joints.
- Choose sufficient vibration energy for low-water, high-strength commercial mixes because these mixes resist natural flow and require mechanical consolidation.
- Proper consolidation helps prevent honeycombing, bug holes, and patching work that can add significant post-pour labor costs.
Frequently Asked Questions
What does a high frequency concrete vibrator do?
It delivers rapid mechanical vibration into fresh concrete, temporarily making the mix more fluid so aggregates settle, entrapped air escapes, and the concrete fills formwork and surrounds reinforcement more completely.
How much air can proper vibration remove from concrete?
Fresh concrete may contain about 5% to 20% entrapped air. Proper vibration can typically reduce this to around 1% to 3%, improving density, strength, and long-term durability.
Why does removing air improve compressive strength?
Entrapped air creates voids that weaken the hardened concrete matrix. Industry guidance commonly notes that removing each 1% of entrapped air can increase compressive strength by about 5%.
What defects can high frequency vibration help prevent?
Correct vibration helps reduce honeycombing, bug holes, weak cold joints, exposed aggregate pockets, and surface blemishes that may otherwise require costly patching after formwork removal.
Is high frequency vibration important for commercial concrete pours?
Yes. Commercial and civil projects often use low-water, high-strength mixes that do not flow easily. Consistent vibration helps meet consolidation expectations and supports structural performance.