Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


Choosing a Concrete Vibrator is not just a matter of picking a tool that “looks big enough.” The right head diameter, frequency, amplitude, and power directly affect air removal, consolidation speed, finish quality, and structural strength. Fresh concrete can contain significant entrapped air, and even small amounts left behind can sharply reduce compressive performance. This guide explains how vibrator size relates to radius of action, placement rate, rebar spacing, and mix behavior, so contractors can avoid honeycombing, cold joints, segregation, and formwork problems. Whether you are working on slabs, walls, columns, precast forms, or heavy civil pours, correct sizing helps turn vibration into a controlled quality process.
How to Choose the Right Concrete Vibrator Size
Proper concrete consolidation is a critical structural requirement, not merely an aesthetic finishing step. When concrete is poured, it typically contains between 5% and 20% entrapped air by volume, depending on the mix design and placement method. In structural engineering, it is a widely accepted metric that for every 1% of entrapped air left in the cured concrete, the compressive strength of the structural element decreases by approximately 5% to 6%. Selecting the correct concrete vibrator size is the primary defense against this structural degradation.
Sizing a concrete vibrator involves calculating the optimal balance between the physical dimensions of the equipment and the dynamic forces it imparts to the concrete mix. An undersized vibrator will fail to mobilize the aggregate, leaving voids and honeycombing, while an oversized unit risks displacing reinforcing steel, blowing out formwork, or causing severe aggregate segregation. The selection process demands a rigorous evaluation of the pour geometry, the concrete mix specifications, and the placement rate.
Why vibrator sizing affects quality and productivity
The primary objective of internal vibration is to temporarily liquefy the mortar matrix, allowing trapped air bubbles to rise to the surface while heavier aggregates settle into a dense, uniform matrix. The size of the vibrator directly dictates the radius of action—the volumetric zone of influence where this liquefaction occurs. If the radius is too small for the pour rate, operators will inevitably rush the insertions, leaving localized zones of un-consolidated material known as honeycombing.
Productivity on the jobsite is mathematically tethered to vibrator sizing. A crew utilizing a 1-inch diameter vibrator head can typically consolidate between 1 and 5 cubic yards per hour. Conversely, upgrading to a 2.5-inch head increases the theoretical consolidation capacity to 25 to 40 cubic yards per hour. If a pump truck is delivering concrete at a rate of 50 cubic yards per hour, utilizing undersized vibrators will create an immediate bottleneck, leading to cold joints as the lower lifts begin to set before the crew can adequately vibrate them.
Furthermore, the quality of the finish is heavily dependent on consistent vibration. Undersized equipment forces the operator to drag the vibrator through the mix—a severe procedural error that leaves distinct trails and structural weaknesses. Correctly sized equipment allows for rapid, vertical insertions and slow withdrawals, seamlessly integrating successive lifts without disrupting the homogeneity of the mix.
Key sizing terms: head diameter, frequency, amplitude, and power
To accurately specify a concrete vibrator, project managers must navigate a specific set of electromechanical and kinetic metrics. The interaction of these four primary variables determines the effective consolidation power of the unit.
Head Diameter: This is the physical width of the vibrating casing inserted into the concrete, typically ranging from 0.75 inches for highly congested precast forms up to 6 inches for massive dam constructions. The diameter is the primary factor governing the volume of concrete affected per insertion.
Frequency (VPM): Measured in Vibrations Per Minute, frequency dictates how rapidly the vibrator head oscillates. Most internal vibrators operate between 8,000 and 17,000 VPM. High frequencies are particularly effective at moving the fine sand and cement paste, making them ideal for high-slump mixes and achieving smooth architectural finishes.
Amplitude: This is the maximum distance the vibrator head displaces from its resting axis during one oscillation cycle, usually measuring between 0.015 and 0.080 inches. Higher amplitude generates the brute kinetic force required to move large, coarse aggregates and is essential for low-slump, stiff concrete mixes.
Power Output: Rated in horsepower (HP) or watts, the motor must possess sufficient torque to maintain the rated frequency and amplitude when submerged in dense concrete. A drop of more than 10% in VPM under load indicates an underpowered unit.
| Metric | Typical Range for Commercial Pours | Primary Effect on Concrete Mix |
|---|---|---|
| Head Diameter | 1.0 in – 3.0 in | Determines the radius of action and placement rate. |
| Frequency | 10,000 – 14,000 VPM | Liquefies mortar; removes entrapped air bubbles. |
| Amplitude | 0.030 in – 0.060 in | Mobilizes coarse aggregate; overcomes mix stiffness. |
| Motor Power | 1.5 HP – 3.0 HP | Prevents RPM drop under hydrostatic load. |
Match Vibrator Head Size to the Concrete and Formwork
Matching the vibrator to the physical constraints of the formwork requires precise spatial planning. The golden rule of clearance dictates that the vibrator head must be at least 0.75 to 1 inch smaller than the narrowest gap between reinforcing steel bars (rebar), and similarly smaller than the distance between the rebar and the formwork face. Forcing a vibrator into a congested rebar cage not only damages the equipment but can permanently displace the structural reinforcement.
Beyond physical clearance, the vibrator must be matched to the rheological properties of the concrete itself. Variables such as slump, aggregate gradation, and the depth of the pour all dictate the kinetic energy required to achieve maximum density without inducing segregation.
How to compare head diameter and radius of action
The radius of action is the radial distance from the center of the vibrator head within which the concrete is fully consolidated. As a general industry heuristic, the radius of action is approximately four to eight times the diameter of the vibrator head, heavily dependent on the mix slump and the vibrator's amplitude.
For example, a standard 2-inch diameter vibrator head typically yields a radius of action of 8 to 14 inches. This means that each vertical insertion covers a circular area 16 to 28 inches across. When planning insertion points, the operator must overlap these zones of influence by approximately one-third of the radius to ensure no dead zones remain.
| Vibrator Head Diameter | Est. Radius of Action | Overlap Spacing (1.5x Radius) | Est. Consolidation Rate |
|---|---|---|---|
| 1.0 inch | 3 to 6 inches | 4.5 to 9 inches | 1 - 5 CY/hr |
| 1.5 inches | 5 to 10 inches | 7.5 to 15 inches | 5 - 10 CY/hr |
| 2.0 inches | 8 to 14 inches | 12 to 21 inches | 10 - 20 CY/hr |
| 2.5 inches | 10 to 18 inches | 15 to 27 inches | 20 - 30 CY/hr |
| 3.0 inches | 12 to 20 inches | 18 to 30 inches | 25 - 40 CY/hr |
How slump, aggregate size, reinforcement, and lift depth affect
sizing
Concrete mix design dramatically alters how a vibrator performs. Slump, which measures the workability of the fresh concrete, is the most critical variable. Low-slump concrete (1 to 3 inches) is highly viscous and requires vibrators with large diameters and high amplitude to physically force the coarse aggregates into place. Conversely, high-slump concrete (5 to 8 inches) flows easily but is highly susceptible to segregation; it requires higher frequency and lower amplitude to gently coax air out without driving the heavy aggregates to the bottom of the form.
Aggregate size also limits equipment choices. If the mix utilizes massive 1.5-inch coarse aggregates, a small 1-inch vibrator will simply bounce off the stones, lacking the kinetic mass to displace them. The vibrator head diameter should ideally be larger than the maximum aggregate size used in the mix.
Finally, lift depth—the thickness of each layer of concrete poured—dictates the length of the vibrator head and the required shaft length. Standard placement practices dictate that lifts should not exceed 12 to 20 inches in depth. The vibrator head must be long enough to completely penetrate the current lift and extend approximately 6 inches into the underlying, previously placed lift to knit the two layers together and prevent cold joints.
When to use internal, external, form, or surface vibrators
While internal (poker) vibrators are the default choice for 90% of commercial concrete placements, certain formwork geometries and mix designs necessitate alternative consolidation technologies.
External or form vibrators are rigidly mounted to the exterior of the formwork. They are mandatory when the rebar congestion is so dense that an internal poker cannot be inserted, such as in heavily reinforced shear walls, tunnel linings, or complex precast concrete molds. Form vibrators require exceptionally sturdy formwork capable of withstanding continuous, high-energy impacts without blowing out, and typically require 1 to 2 minutes of vibration time per lift.
Surface vibrators, including vibrating screeds and pan vibrators, are utilized exclusively for flatwork such as slabs, pavements, and bridge decks. A vibrating screed can effectively consolidate concrete to a depth of roughly 6 to 8 inches. If a slab exceeds 8 inches in thickness, surface vibration alone is inadequate; the lower portion of the slab must first be consolidated with an internal vibrator before the surface screed is applied.
Power Requirements for Different Jobsite Conditions
Delivering consistent kinetic energy to the concrete requires a robust and reliable power source. The environment of the jobsite—whether a high-rise tower with ample electrical drops, a remote bridge abutment, or an underground tunnel—dictates the optimal power class for the vibrator fleet.
A critical metric in assessing power requirements is the motor's ability to maintain its rated frequency under hydrostatic load. When a vibrator is submerged in dense, wet concrete, the resistance causes the motor's RPM to drop. High-quality power units are engineered with sufficient torque reserves to keep the frequency drop below 10%, ensuring the VPM stays within the optimal 10,000 to 14,000 range necessary for structural concrete.
Electric, pneumatic, gasoline, and hydraulic power options
Electric Vibrators are the industry standard for enclosed or urban jobsites. Operating on standard 115V or 230V single-phase power, these units typically draw between 10 and 15 amps. High-frequency electric vibrators contain the motor directly within the head, eliminating the need for a flexible drive shaft and allowing for highly efficient power transmission. They are relatively lightweight, emission-free, and require minimal maintenance.
Pneumatic (air-driven) vibrators are the heavy-duty workhorses of massive infrastructure projects. They require a dedicated industrial air compressor, typically demanding 40 to 100 CFM of airflow at 80 to 100 PSI. Because they lack electrical components and stay cool by venting exhaust air, pneumatic vibrators can run continuously for hours without overheating, making them ideal for massive, continuous pours like dam construction.
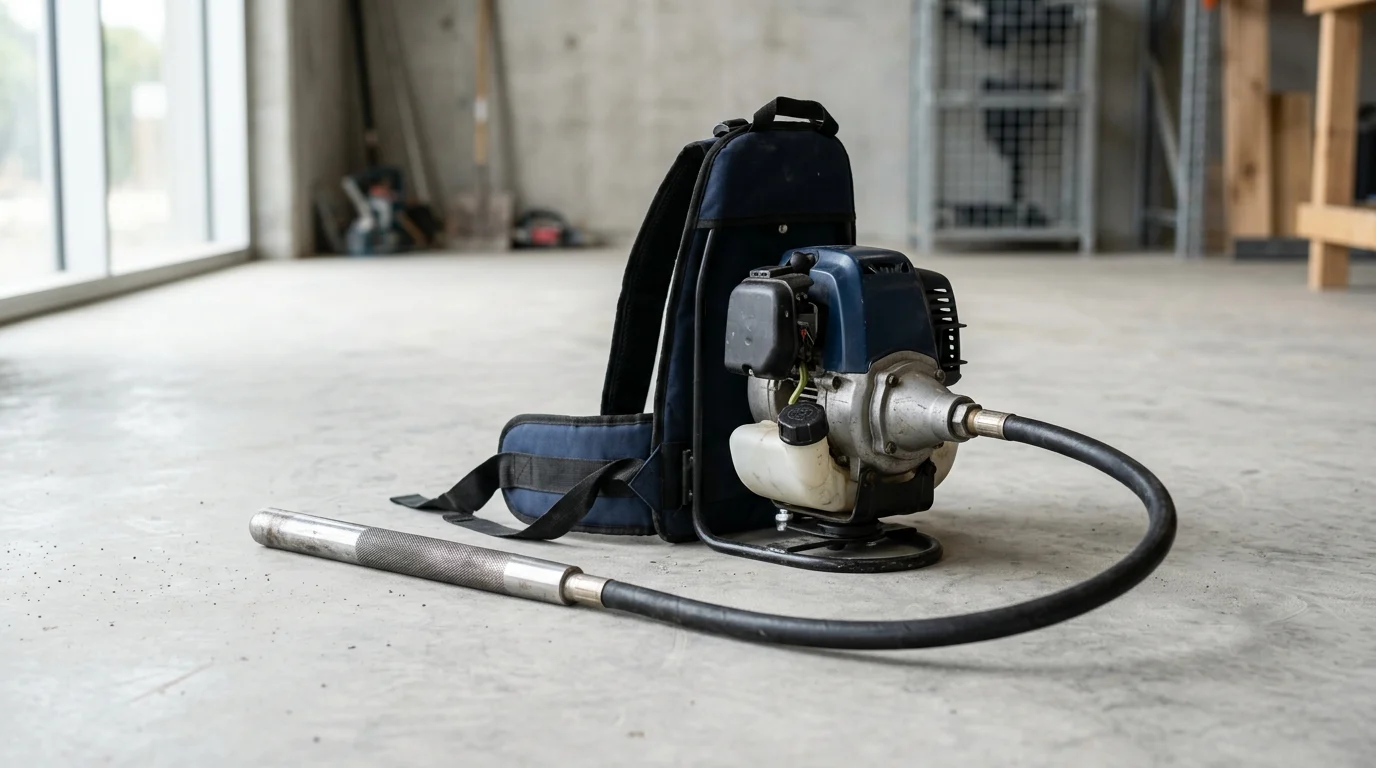
Gasoline-powered vibrators offer maximum mobility for flatwork and remote sites lacking electrical infrastructure. Often configured as backpack units weighing roughly 24 to 30 pounds, they utilize small 4-stroke engines producing 1.5 to 3.0 horsepower. While they offer unparalleled freedom of movement, they introduce exhaust emissions, making them strictly prohibited for indoor or deep-trench applications.
Hydraulic vibrators are typically mounted directly to heavy machinery, such as slip-form pavers or excavators. Utilizing the carrier machine's hydraulic PTO, these units deliver immense, variable-speed power and are capable of driving multiple large-diameter vibrator heads simultaneously in automated paving operations.
Shaft length, motor output, and frequency stability
The flexible drive shaft on electric and gas vibrators serves as the critical transmission link between the power unit and the eccentric weight inside the head. Shaft lengths vary drastically, from compact 2-foot whips for shallow slabs to heavy-duty 21-foot cables for deep column pours. However, physics dictates a penalty for extended reach.
As shaft length increases, internal friction within the casing absorbs rotational energy, reducing the ultimate motor output delivered to the head. A motor that easily drives a 2-inch head on a 5-foot shaft may experience severe RPM degradation—or frequency instability—if paired with a 21-foot shaft. When specifying long shafts for deep forms, contractors must upsize the motor output by roughly 0.5 to 1.0 HP to compensate for this frictional loss.
Frequency stability under load is the hallmark of a properly matched motor and shaft. If the motor bogs down and the VPM drops below 8,000, the vibrator will no longer effectively liquefy the mortar, forcing the operator to leave the head in the concrete for extended periods, which critically delays the placement rate and increases the risk of cold joints.
Safety, noise, access, and compliance considerations
Equipment selection must strictly adhere to occupational safety and environmental compliance standards. Noise exposure is a significant differentiator among power types. Pneumatic and gas-powered vibrators routinely exceed 90 decibels (dB(A)) under load, triggering mandatory OSHA hearing conservation protocols and PPE requirements. Conversely, modern electric internal vibrators typically operate below the 85 dB(A) threshold.
Electrical safety is paramount on wet concrete jobsites. All 115V/230V electric vibrators must be routed through Ground Fault Circuit Interrupter (GFCI) protection. For highly conductive environments, such as steel-lined forms or tunnel inverts, low-voltage (42V) high-frequency vibrators operated via step-down inverters are often mandated by safety engineers to eliminate the risk of fatal electrocution.
Access and ergonomic limits also dictate power choices. Prolonged use of heavy equipment induces operator fatigue, directly impacting consolidation quality. Backpack gasoline units, while mobile, limit the operator to roughly 20-30 pounds of carried weight, meaning they cannot practically drive heads larger than 2.5 inches. For deep, highly congested forms requiring massive 3-inch heads, crane-suspended pneumatic or heavy-duty electric units are required to bypass human ergonomic limitations.
How to Size the Number of Vibrators Needed
Determining the exact number of vibrators required for a pour is an exercise in matching the volumetric output of the delivery system (pump trucks, buckets, or conveyors) to the volumetric consolidation capacity of the vibrator fleet. Failing to perform this calculation often results in crews being overrun by the concrete supply.
A standard rule of thumb for commercial construction is to calculate the fleet size based on the maximum anticipated delivery rate, and then add a strict redundancy factor. A $50,000 structural pour should never be compromised by the failure of a $600 piece of equipment.
Step-by-step sizing workflow
The step-by-step sizing workflow begins with identifying the peak placement rate. If a concrete pump is scheduled to deliver 60 cubic yards per hour, the consolidation fleet must process exactly that amount. Next, determine the capacity of the selected vibrator based on head diameter and form restrictions. If clearance limits you to a 1.5-inch vibrator (which consolidates roughly 8 CY/hr), you divide the pour rate by the unit capacity: 60 / 8 = 7.5.
In this scenario, a minimum of 8 active vibrators are required to keep pace with the pump truck. The final step is factoring in redundancy. Industry best practice mandates a minimum of one standby vibrator for every three active units. Therefore, this specific pour requires a total fleet of 11 vibrators on-site (8 active, 3 backup).
This workflow must be adjusted if the pour geometry changes. A wide-open mat foundation allows operators to move quickly, maximizing the vibrator's theoretical CY/hr rating. A heavily reinforced column requires slow, deliberate insertions and careful maneuvering around ties, which can reduce the effective consolidation rate of the same vibrator by 30% to 40%.
Placement rate, lift thickness, and insertion spacing
The interplay between placement rate, lift thickness, and insertion spacing dictates the physical rhythm of the crew. Concrete should be placed in level lifts no deeper than 20 inches. If a pump operator dumps a 40-inch localized mound of concrete, the vibrator cannot reach the bottom of the lift, and attempting to drag the concrete laterally with the vibrator will cause severe aggregate segregation.
Insertion spacing must follow a strict geometric grid. The distance between insertions should be roughly 1.5 times the radius of action. For a 2-inch head with a 10-inch radius, insertions should occur every 15 inches. The operator must insert the head vertically under its own weight, allow it to dwell for 5 to 15 seconds until the surface takes on a sheen and large air bubbles stop escaping, and then withdraw it slowly at a rate of roughly 1 to 3 inches per second.
This slow withdrawal is critical; it allows the mortar to flow back together behind the head, filling the void left by the casing. If the withdrawal is too fast, particularly in stiff, low-slump mixes, a permanent "vibrator hole" or core will be left in the cured concrete, creating a severe structural defect.
Field signs of under-vibration and over-vibration
Field supervisors must constantly monitor the pour for signs of improper vibration. Under-vibration is the most common error, visually manifesting after form removal as honeycombing (exposed coarse aggregate with no mortar binding it), large bug holes (surface air voids exceeding 0.5 inches in diameter), and distinct cold joints between lifts.
Over-vibration, while less common, is equally destructive, particularly in high-slump or self-consolidating concrete (SCC) mixes. If a vibrator is left in a high-slump mix for more than 20 seconds, the kinetic energy drives the heavy coarse aggregates to the bottom of the form while the lighter water and fine cement paste rise to the top. This is known as segregation.
The immediate field sign of over-vibration is the rapid accumulation of a frothy, watery layer on the top surface of the lift, known as laitance. Laitance possesses virtually no compressive strength and prevents the subsequent lift from bonding properly. Additionally, excessive vibration against the form face can cause formwork deflection or catastrophic blowout due to the localized spike in hydrostatic pressure.
Best Concrete Vibrator Size and Power Class by Application
Synthesizing all the variables—clearance, slump, power, and placement rate—allows project managers to standardize their equipment choices based on the structural element being cast. Establishing a baseline vibrator specification for common applications minimizes guesswork and ensures the right tool is mobilized for the job.
The following matrices and recommendations represent industry consensus for commercial and heavy civil concrete placements, balancing the need for rapid consolidation with the physical realities of modern, heavily reinforced structural designs.
Selection matrix for slabs, walls, columns, and footings
Different structural elements impose distinct constraints on equipment selection. Slabs and flatwork typically feature shallow depths and minimal vertical rebar, allowing for high-mobility setups.
Key Takeaways
- Select the vibrator head diameter based on pour geometry, rebar congestion, and the radius of action needed for full consolidation.
- Do not leave consolidation to chance, because every 1% of entrapped air remaining in cured concrete can reduce compressive strength by about 5% to 6%.
- Match vibrator output to placement speed, since a 1-inch head may consolidate only 1 to 5 cubic yards per hour while a 2.5-inch head may handle 25 to 40 cubic yards per hour.
- Avoid undersized vibrators because they create bottlenecks, honeycombing, and cold-joint risks when concrete arrives faster than the crew can consolidate it.
- Avoid oversized vibrators in tight forms because excessive energy can displace reinforcement, stress formwork, and cause aggregate segregation.
- Use rapid vertical insertions and slow withdrawals instead of dragging the vibrator through the mix to maintain uniform strength and finish quality.
Frequently Asked Questions
What happens if I use a concrete vibrator that is too small?
An undersized vibrator has a limited radius of action, so it may leave trapped air, voids, and honeycombing. It can also slow production and create cold-joint risks when concrete placement outpaces consolidation.
Can a concrete vibrator be too large for the pour?
Yes. An oversized vibrator can cause aggregate segregation, move reinforcing steel, damage forms, or over-consolidate the mix. Size should match the form geometry, rebar spacing, mix design, and placement rate.
How much strength can trapped air remove from concrete?
Concrete often contains 5% to 20% entrapped air during placement. As a rule of thumb, each 1% of air left in cured concrete can reduce compressive strength by about 5% to 6%.
What is the most important sizing factor for an internal concrete vibrator?
Head diameter is usually the starting point because it determines the radius of action and how much concrete each insertion can consolidate. Frequency, amplitude, and motor power must also match the job.
How do I match vibrator size to concrete placement rate?
Choose a vibrator that can consolidate concrete at least as fast as it is being placed. For example, a 1-inch head may handle 1 to 5 cubic yards per hour, while a 2.5-inch head may reach 25 to 40 cubic yards per hour.