Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


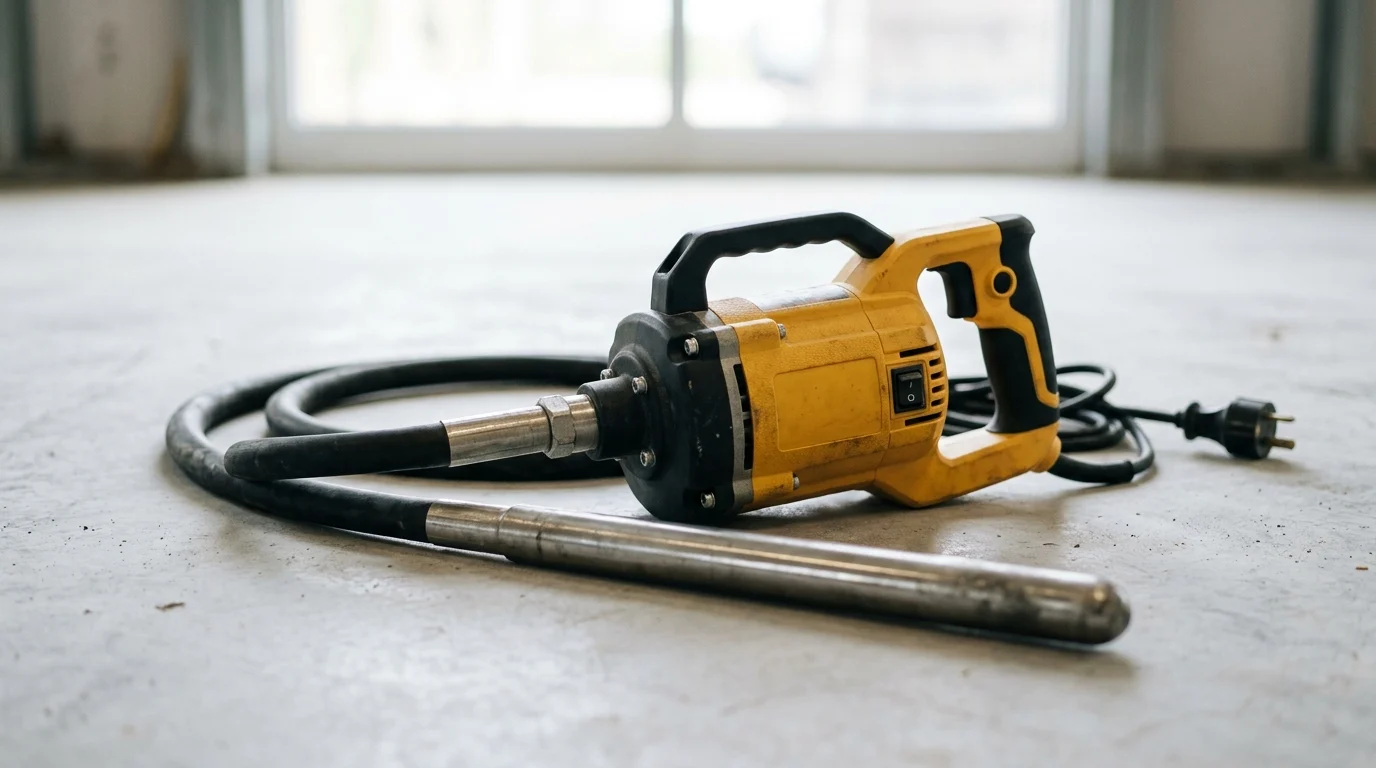
Concrete consolidation is one of the few jobsite steps that can quietly determine whether a structure reaches its designed strength or develops costly defects later. A high-frequency Concrete Vibrator is built for situations where ordinary vibration may not move enough entrapped air fast enough—especially in low-slump mixes, congested reinforcement, bridge piers, mat foundations, and other demanding pours. Because fresh concrete can hold significant trapped air, the right vibration method directly affects density, steel bond, surface finish, and long-term durability. This guide explains when high-frequency vibration is the better choice, how it improves quality and productivity, and where contractors should use caution to avoid over-consolidation.
Why Choose a High-Frequency Concrete Vibrator
Deploying a high-frequency concrete vibrator improves the consolidation dynamics of freshly poured concrete in commercial and civil engineering projects. Proper consolidation is not merely a cosmetic requirement; it is a structural imperative necessary to achieve the designed compressive strength and durability of the concrete element. Operating at elevated frequencies—typically exceeding 12,000 vibrations per minute (vpm) under load—these specialized tools rapidly fluidize stiff, low-slump mixes that standard equipment cannot effectively process.
In demanding environments, the margin for error is exceptionally narrow. Failing to adequately remove entrapped air voids compromises the structural matrix and exposes reinforcing steel to accelerated corrosion. By utilizing high-frequency consolidation, contractors ensure uniform aggregate distribution and maximum density, satisfying rigorous engineering specifications and extending the concrete asset's lifecycle.
Productivity and Concrete Quality Benefits
The primary technical advantage of high-frequency vibration lies in its significant impact on concrete density and compressive strength. When initially placed, concrete can contain 5% to 20% entrapped air by volume, depending on the mix design and placement method. A high-frequency concrete vibrator accelerates the upward migration of these air bubbles, systematically reducing the entrapped air volume below the critical 2% threshold.
This reduction in air voids translates directly into enhanced mechanical properties. For every 1% of entrapped air remaining in the cured concrete, compressive strength decreases by approximately 3% to 5%. Furthermore, high-frequency action ensures a tighter bond between the cement paste and the aggregate, as well as between the concrete and reinforcing steel. This superior bond strength is vital in seismic zones and high-load-bearing infrastructure. However, operators must exercise caution with lightweight or air-entrained structural concrete; excessive high-frequency vibration can collapse intentionally entrained microscopic air voids, which are necessary for freeze-thaw resistance.
Commercial Value for Contractors
Beyond structural integrity, utilizing high-frequency equipment presents significant commercial advantages for concrete contractors. The financial implications of poor consolidation are severe; remediating surface defects like honeycombing, bugholes, and cold joints can incur substantial costs per square foot in specialized labor and repair materials. By achieving a dense, highly uniform finish straight out of the formwork, contractors drastically reduce post-pour patching and cosmetic remediation expenses.
Additionally, high-frequency vibrators expedite the pour cycle. Their ability to rapidly liquefy the concrete matrix allows placement crews to work faster without sacrificing quality. In large-scale commercial projects, accelerating the pour rate can shave days off the critical path schedule. This reduces overhead costs, equipment rental durations, and labor hours, boosting the overall return on investment.
Key Use Cases
High-frequency vibrators are the equipment of choice across a spectrum of demanding civil and commercial applications. In mass pouring projects—such as dam construction, mat foundations, and bridge piers—the sheer volume of concrete requires equipment capable of sustained, high-output performance to prevent cold joints between massive lifts.
Slip-form paving operations also rely heavily on high-frequency consolidation. Because slip-forming utilizes extremely low-slump concrete that must support its own weight immediately upon exiting the paver, high-frequency external or internal vibrators are necessary to fluidize the mix just long enough to pass through the forms. Similarly, constructing high-rise elevator cores, shear walls, and precast concrete elements demands high-frequency tools to ensure flawless architectural finishes and structural continuity.
What Defines a High-Frequency Concrete Vibrator
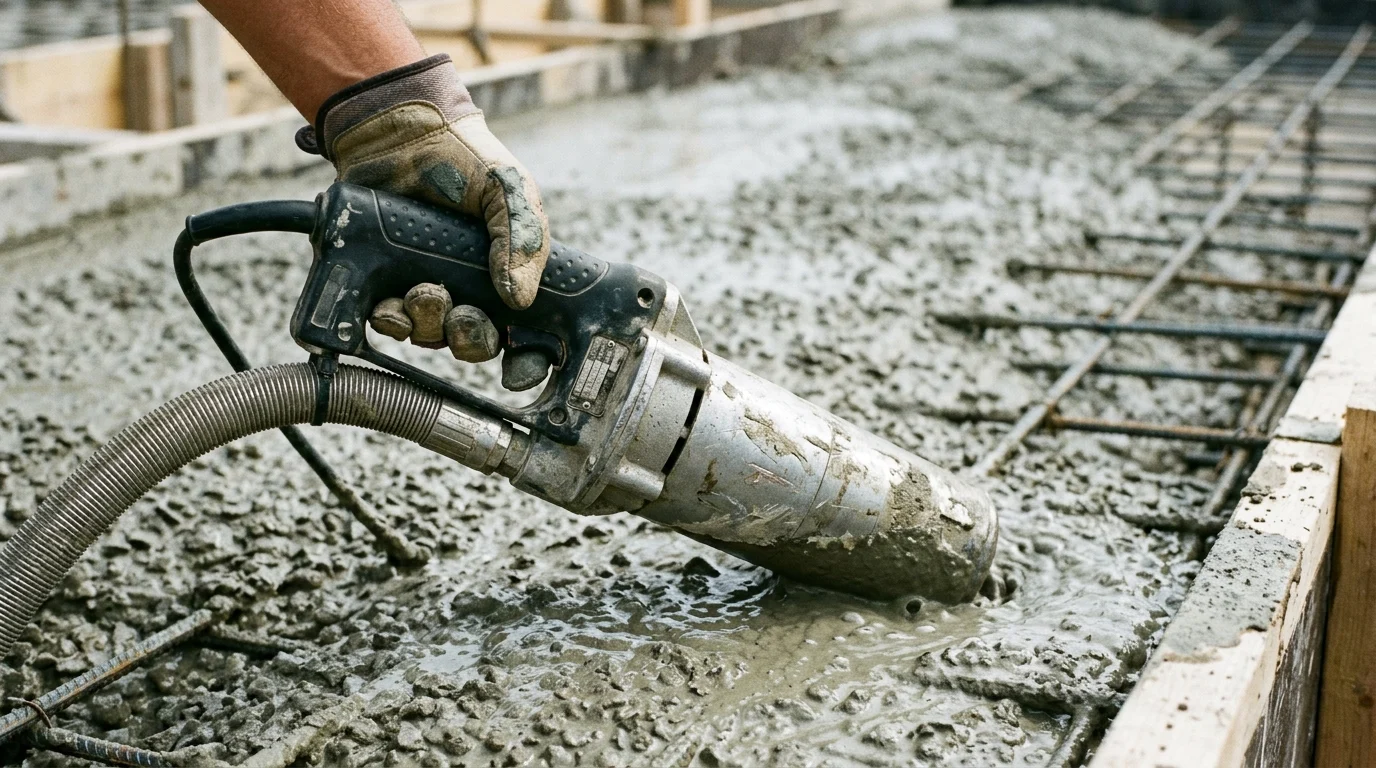
Defining high-frequency equipment requires examining the physical properties of mechanical vibration and how these forces interact with cementitious materials. The classification of a high-frequency concrete vibrator generally begins at a baseline of 10,000 vpm, with premium commercial units operating efficiently between 12,000 and 14,000 vpm under the heavy load of wet concrete.
Unlike standard flex-shaft vibrators that rely on lower frequencies and higher amplitudes to move large aggregates, high-frequency models are specifically tuned to target the internal friction of the cement paste. By rapidly breaking this friction, the paste liquefies, allowing heavier coarse aggregates to settle naturally into a dense matrix while forcing lighter air pockets to the surface.
Frequency, Amplitude, and Head Diameter
The performance of any internal vibrator is governed by the interplay of frequency, amplitude, and head diameter. Frequency dictates the speed at which the cement paste liquefies, while amplitude—the maximum distance the vibrator head travels from its resting axis—dictates the movement of the coarse aggregate. High-frequency models typically feature a lower, tighter amplitude ranging from 0.04 to 0.10 inches, optimizing them for rapid paste fluidization rather than aggressive aggregate displacement.
Head diameter further influences the tool's radius of action (ROA), which is the effective zone of consolidation around the vibrator. High-frequency internal vibrator heads generally range from 1.5 to 3 inches in diameter. A larger diameter displaces more material and generates a wider ROA, but it requires significantly more power to maintain speeds above 12,000 vpm. Selecting the correct balance ensures the tool processes the mix efficiently without bogging down the motor.
Internal, External, Pneumatic, and Electric Types
High-frequency vibrators are categorized by their power source and application methodology. Internal vibrators (poker or spud vibrators) are submerged directly into the mix, while external vibrators are securely mounted to the exterior of the formwork, transferring vibrational energy through the forms into the concrete. Power sources further differentiate these tools into electric, pneumatic, and specialized high-cycle categories.
| Vibrator Type | Power Source | Typical Frequency Range | Primary Application |
|---|---|---|---|
| High-Cycle Electric (Internal) | 42V / 200Hz Inverter | 12,000 vpm | Heavy civil, dense rebar, low-slump mixes |
| Standard Electric (Internal) | 115V / 60Hz | 10,000 - 12,000 vpm | General commercial flatwork and walls |
| Pneumatic (Internal/External) | Air Compressor (CFM dependent) | 10,000 - 15,000 vpm | Hazardous environments, mass pours |
| High-Frequency External | 115V or 230V | 9,000 - 12,000 vpm | Precast yards, complex architectural forms |
High-cycle Electric Vibrators are particularly notable in this category. They utilize a built-in or external frequency converter to step standard 60Hz power up to 200Hz. This electrical transformation allows the motor—housed directly inside the vibrator head rather than in an external drive unit—to spin at 12,000 RPM consistently, eliminating the RPM loss associated with mechanical flex-shafts.
Key Specification Factors
When specifying a high-frequency concrete vibrator, engineers and contractors must look beyond basic RPM ratings. Centrifugal force, measured in pounds-force (lbf) or Newtons, is a critical metric indicating the actual compaction power delivered into the mix. A commercial 2-inch high-frequency head typically generates between 1,000 and 1,800 lbf, while massive 3-inch models can exceed 3,000 lbf.
Another vital specification is the previously defined ROA, which dictates the spacing of insertions during a pour. Failure to properly align the equipment's centrifugal force and ROA with the project's pour volume can lead to localized under-consolidation.
When High-Frequency Vibration Works Best
High-frequency vibration is not a universal requirement for all concrete placement scenarios; rather, it is a specialized intervention that excels under strict engineering constraints. It becomes indispensable when placing stiff, low-slump concrete—typically defined as having a slump of less than 3 inches. Standard-frequency equipment often struggles to overcome the internal friction of these stiff mixes, leading to incomplete compaction and honeycombing.
Understanding when to deploy high-frequency technology requires assessing the formwork geometry, the density of the reinforcement detailing, and the specific rheology of the concrete mix. When applied correctly, high-frequency tools navigate extreme spatial constraints and challenging mix designs with an efficiency that lower-frequency alternatives cannot match.
Dense Rebar and Complex Formwork
One of the most critical use cases for high-frequency vibrators involves congested reinforcement grids. In modern seismic and high-rise structural designs, rebar congestion frequently leaves clearances of less than 2 inches. Standard coarse aggregates can easily bridge across these tight gaps, creating severe voids and rock pockets within the core of the structural element.
High-frequency vibration effectively fluidizes the cement paste to a near-liquid state. This allows the paste to fully encapsulate dense rebar matrices, lubricating the coarse aggregate so it can slip through narrow structural bottlenecks. Furthermore, the motor-in-head design of many high-frequency units eliminates the bulky mechanical flex-shaft, allowing the operator to thread the vibrator head deep into complex formwork without snagging.
Avoiding Over-Vibration and Segregation
While highly effective, the power of a high-frequency concrete vibrator introduces a heightened risk of over-vibration. Because these tools liquefy the mix so rapidly, leaving the vibrator head in a single insertion point for too long can cause segregation. Segregation occurs when heavy coarse aggregate sinks to the bottom of the lift, forcing weak, water-rich laitance to the surface, which drastically compromises the element's structural integrity.
To mitigate this risk, operators must adhere to strict insertion timing. While standard vibrators might require 15 to 20 seconds per insertion, a 12,000 vpm high-frequency unit often achieves full consolidation in just 5 to 15 seconds. Continuous visual monitoring of the concrete surface is mandatory to ensure the vibrator is extracted the moment the surface achieves a smooth sheen and large air bubbles cease escaping.
Comparison With Standard Concrete Vibrators
Comparing standard low-frequency equipment against high-frequency alternatives helps clarify the operational boundaries of each tool. Standard vibrators are highly effective for high-slump, highly workable mixes commonly found in residential and light commercial flatwork. Conversely, high-frequency units represent an engineered solution for heavy civil and specialized architectural applications.
| Specification / Feature | Standard Flex-Shaft Vibrator | High-Frequency Motor-in-Head |
|---|---|---|
| Typical Frequency | 8,000 - 10,000 vpm | 12,000 - 14,000+ vpm |
| Primary Application | High-slump residential/commercial | Low-slump, dense rebar, mass pours |
| Drive Mechanism | External motor with flexible shaft | Motor built directly into the vibrator head |
| Amplitude | Higher (displaces large aggregate) | Lower (optimizes paste fluidization) |
| Cost Bracket | Lower upfront capital ($300 - $800) | Higher initial investment ($1,200 - $3,500) |
The absence of a flexible drive shaft in high-frequency electric models also results in a more consistent power curve. Flex-shafts inherently lose RPMs as the shaft bends and encounters friction inside the casing. High-frequency motor-in-head units maintain their full 12,000 vpm rating regardless of how the power cable is routed through the scaffolding.
How to Use High-Frequency Internal Vibrators
Operational execution with high-frequency internal vibrators dictates the ultimate structural integrity of the final concrete element. Even the most advanced equipment will fail to prevent honeycombing and cold joints if deployed using improper techniques. Industry standards demand rigorous adherence to systematic insertion patterns, controlled lift depths, and strict extraction rates.
Operators must be trained to treat the high-frequency concrete vibrator as a precision instrument. Managing the intense centrifugal force requires a disciplined approach to the concrete pour cycle. Additionally, operating high-frequency equipment requires strict adherence to safety and ergonomics protocols. These tools generate hazardous noise levels, making hearing protection mandatory. Operators must also be certified or trained on OSHA/NIOSH vibration exposure limits to prevent ergonomic injuries during prolonged use.
Lift Thickness and Insertion Spacing
The foundational rule of internal vibration is managing the depth of the concrete lift. Industry best practices stipulate that individual pour lifts should be limited to a maximum thickness of 20 inches. Attempting to consolidate deeper lifts prevents the high-frequency vibrator's amplitude from fully penetrating and fluidizing the entire layer, leading to trapped air and incomplete compaction at the base of the lift.
Insertion spacing must be mathematically tied to the vibrator's established ROA. If a specific high-frequency head has an ROA of 14 inches, insertions must not be spaced 28 inches apart. Instead, spacing should be approximately 1.5 times the ROA—roughly 20 to 21 inches—to guarantee a 1-to-2-inch overlap between the fields of action. This overlapping grid ensures no localized zones of uncompacted concrete remain.
Placement Rate and Cold Joint Prevention
In continuous mass pours or tall structural columns, preventing cold joints between successive lifts is a paramount concern. A cold joint occurs when a lower lift of concrete begins to set before the subsequent lift is placed and consolidated, creating a distinct plane of weakness. High-frequency vibrators are highly effective at knitting these layers together, provided the placement rate is carefully synchronized with the consolidation effort.
To achieve a monolithic structure, the operator must allow the vibrator head to penetrate through the current lift and extend at least 6 inches into the preceding lift. Because high-frequency units liquefy paste rapidly, this deep penetration thoroughly blends the coarse aggregates and cement paste of the two layers while the lower lift remains in a plastic state. The vibrator must then be extracted slowly—at a rate of approximately 1 inch per second—allowing the fluidized concrete to collapse seamlessly behind the head.
Quality Control Checks
Quality control during high-frequency consolidation relies heavily on the operator's ability to read visual cues from the concrete surface. The primary indicators of optimal consolidation are the cessation of large, entrapped air bubbles breaking the surface, the settling of the concrete to an even level within the form, and the appearance of a thin, glossy film of mortar (sheen) across the top.
On highly regulated infrastructure projects, defect rate reduction metrics are strictly enforced, often requiring surface defects to remain below stringent percentage thresholds. Quality control inspectors monitor the vibrator's operating frequency under load using digital tachometers to ensure the equipment maintains the mandatory 12,000 vpm threshold. If the RPM drops significantly, it indicates either a power supply issue or that the vibrator head is undersized for the stiffness of the mix.
How to Specify, Rent, or Purchase the Right Vibrator
The procurement of concrete consolidation equipmentinvolves balancing upfront capital expenditures against long-term operational efficiencies and project-specific technical demands. Commercial-grade high-frequency Concrete Vibrators represent a significant investment, typically ranging from $1,200 to $3,500 per unit, depending on the power source, head diameter, and integrated converter technology.
Contractors must approach this investment strategically. Selecting the wrong equipment not only wastes capital but can also lead to costly pour failures, rejected elements, and severe project delays. A structured procurement approach ensures the chosen vibrator aligns perfectly with the mix design, the site's logistical constraints, and the contractor's financial parameters.
Matching the Vibrator to the Mix Design
The first step in equipment specification is matching the vibrator's mechanical output to the specific rheology of the concrete mix. High-frequency units are specifically engineered for conventional low-slump mixes, harsh mixes with high ratios of coarse aggregate, and mixes utilizing heavy supplementary cementitious materials (SCMs) like silica fume, which dramatically increase mix stickiness.
Conversely, high-frequency vibrators must be specified with extreme caution—or avoided entirely—when working with Self-Consolidating Concrete (SCC). SCC is chemically designed to flow and consolidate under its own weight. Applying internal high-frequency vibration to an SCC mix risks gradual segregation, driving heavy aggregate to the bottom and compromising the pour. While external vibration may sometimes be used cautiously, internal high-frequency tools are generally avoided for SCC. Understanding these chemical-mechanical interactions is vital for correct specification.
Rental, Purchase, and Total Cost Factors
Financial decision-making hinges on the frequency of use and project duration. Rental rates for high-frequency motor-in-head vibrators generally average between $150 and $250 per week. For short-term projects or specialized one-off mass pours, renting preserves capital and eliminates maintenance overhead. However, reliance on rentals can be costly for contractors specializing in heavy civil or high-rise construction.
A standard break-even analysis typically reveals that purchasing the equipment becomes more economical if the high-frequency vibrator is required for more than four to six weeks annually. When calculating the total cost of ownership, contractors must also factor in the cost of necessary auxiliary equipment. For example, standard high-cycle vibrators require external 42V/200Hz Generators or electronic inverters, which can add $2,000 to $4,000 to the total system cost. In contrast, models with built-in electronic converters plug directly into standard 115V outlets but carry a higher per-unit price.
Final Selection Framework
To finalize the selection, project managers should utilize a systematic framework that evaluates power availability, rebar density, and total pour volume. Use the following checklist to guide the decision process:
- Assess Power Infrastructure: If the site lacks robust electrical access, pneumatic high-frequency vibrators powered by diesel air compressors may be the only viable option. If standard 115V power is abundant, plug-and-play electric models with integrated converters offer the highest mobility.
- Analyze Structural Clearances: Review the structural drawings to determine the tightest rebar clearances. The vibrator head diameter must be at least 0.5 inches smaller than the narrowest clearance to prevent the tool from becoming wedged in the steel.
- Calculate Placement Rate: Determine the required cubic yards per hour. The chosen vibrator's ROA and centrifugal force must be capable of processing the concrete faster than the pump trucks deliver it, ensuring the consolidation phase never becomes the bottleneck of the operation.
Key Takeaways
- Use high-frequency concrete vibrators for reinforced, low-slump, and mass pours where rapid air removal and dense consolidation are required.
- Target proper consolidation because fresh concrete can contain 5% to 20% entrapped air, and every 1% of remaining air may reduce compressive strength by about 3% to 5%.
- Select high-frequency equipment operating around or above 12,000 vpm under load when standard vibrators cannot efficiently fluidize stiff mixes.
- Avoid over-vibrating lightweight or air-entrained concrete because excessive vibration can reduce freeze-thaw durability or cause mix segregation.
- In large commercial pours, faster consolidation can reduce patching, limit honeycombing, shorten pour cycles, and lower labor or equipment rental costs.
Frequently Asked Questions
What makes a concrete vibrator “high-frequency”?
A high-frequency concrete vibrator typically operates above 12,000 vibrations per minute under load. This faster vibration helps fluidize stiff or low-slump concrete, move trapped air upward, and improve consolidation around aggregate and reinforcing steel.
When should contractors choose a high-frequency concrete vibrator?
Choose it for reinforced concrete, low-slump mixes, bridge piers, mat foundations, dams, columns, walls, and other pours where dense consolidation, strong steel bond, and minimal voids are critical.
How does high-frequency vibration improve concrete strength?
Fresh concrete may contain 5% to 20% trapped air. Proper high-frequency vibration can reduce voids toward below 2%, improving density and helping protect compressive strength, since each 1% of remaining air can reduce strength by about 3% to 5%.
Can high-frequency vibration damage concrete?
Yes, if overused. Excessive vibration can cause segregation or collapse intentionally entrained air in freeze-thaw resistant concrete. Operators should match vibration time, spacing, and head size to the mix design and project specifications.
Why is high-frequency vibration useful in reinforced concrete?
Reinforcing steel creates congestion that can trap air and prevent concrete from fully flowing around bars. High-frequency vibration improves paste flow, reduces honeycombing, and helps create a stronger bond between concrete and rebar.