Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


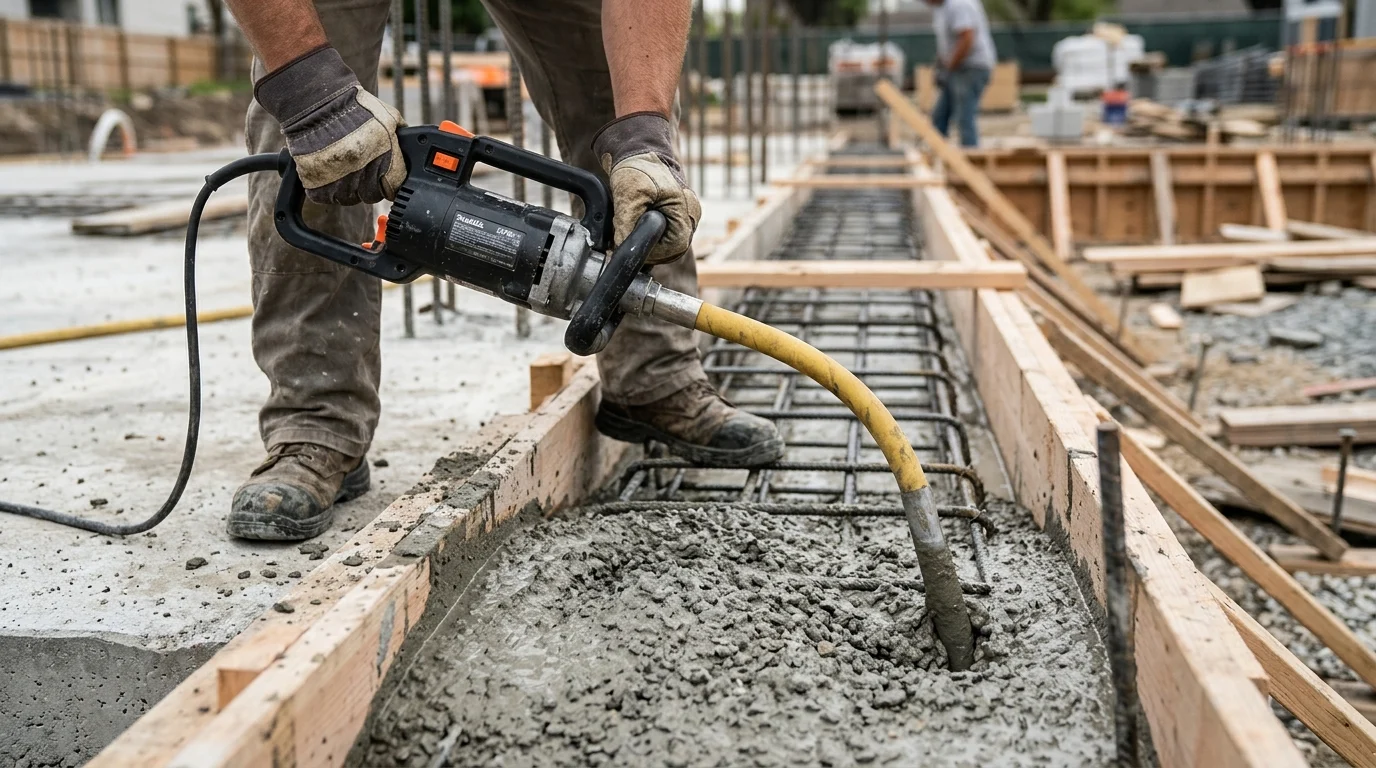
Concrete defects rarely start as surface problems; they usually begin inside the pour, where trapped air, stiff mortar, and congested reinforcement prevent full consolidation. Concrete Vibratorssolve this quality-control challenge by converting vibration energy into denser placement, stronger rebar bond, and fewer voids before the concrete sets. The stakes are measurable: even small percentages of entrapped air can sharply reduce compressive strength, while visible honeycombing can trigger repair costs, schedule delays, and durability concerns. This article explains how vibration works, why it prevents voids and segregation when used correctly, and what contractors should consider when choosing equipment such as internal vibrators, vibrator shafts, and external vibration tools.
Why Concrete Vibrators Are Critical for Quality Control
Freshly poured concrete is not a solid mass; it is a complex, high-viscosity suspension of cement, water, fine aggregates, and coarse aggregates. During placement, a significant volume of air inherently becomes trapped within this matrix due to the friction between particles and the dropping of the material into formwork. Unconsolidated concrete can contain up to 20% entrapped air by volume, a condition that severely compromises the structural density, permeability, and durability of the finished element. Concrete vibrators serve as the primary mechanical intervention to expel this entrapped air, transforming the stiff, heterogeneous mixture into a dense, uniform, and fluid-like state. This process, known as consolidation, is a non-negotiable phase of quality control in commercial, industrial, and heavy civil construction.
Without active mechanical consolidation, the internal friction of the concrete mix prevents the aggregate from nesting tightly and stops the mortar from filling the interstitial spaces. Relying solely on gravity or manual rodding is insufficient for modern mix designs, which often feature lower water-to-cement ratios to achieve higher early strengths. By introducing localized kinetic energy, concrete vibrators temporarily alter the rheology of the mix, enabling the release of entrapped air and ensuring the concrete fully encapsulates reinforcing steel and embedments.
How Concrete Vibrators Protect Structural Integrity
The relationship between concrete density and structural integrity is governed by strict mathematical realities. For every 1% of entrapped air left in a concrete matrix, the compressive strength of that structure decreases by approximately 5%. Consequently, a void ratio of just 5% can result in a 25% reduction in load-bearing capacity, rapidly rendering the concrete non-compliant with standard structural specifications. Concrete vibrators prevent this degradation by transmitting high-frequency mechanical waves into the mix, which temporarily overcome the yield stress of the cement paste.
As the mortar liquefies under vibration, the heavier coarse aggregates settle under the force of gravity, and the lighter entrapped air bubbles are forced upward to the surface. Furthermore, proper vibration ensures optimal bonding between the concrete and the reinforcing steel. Structural design relies heavily on the assumption of a continuous, void-free interface between rebar and concrete to transfer tensile loads effectively. Honeycombing or macro-voids along the reinforcement drastically reduce this bond strength and provide direct pathways for moisture, oxygen, and chlorides, thereby accelerating rebar corrosion and severely reducing the asset's overall lifecycle.
Commercial Risks of Honeycombing, Voids, and Segregation
The commercial implications of poor consolidation extend far beyond theoretical strength reductions. Honeycombing—characterized by exposed coarse aggregate with a severe deficiency of mortar—and segregation represent massive financial liabilities for general contractors and concrete subcontractors. When formwork is stripped to reveal extensive voids, the immediate consequences involve project delays, specialized engineering reviews, and costly remediation protocols that disrupt the critical path of the construction schedule.
Remediation techniques, such as high-pressure epoxy injection, structural patching, or carbon fiber jacketing, frequently cost between $150 and $300 per square foot, depending on the severity, elevation, and accessibility of the defect. In severe cases where the core structural integrity is compromised, the engineer of record may mandate the complete demolition and replacement of the affected element. Beyond direct repair costs, visible honeycombing often leads to aesthetic rejection in architectural concrete applications, triggering contractual disputes, withheld retainage, and permanent damage to a contractor's reputation. Implementing a rigorous vibration protocol is a high-ROI quality assurance measure that systematically mitigates these catastrophic commercial risks.
What Causes Honeycombing in Concrete
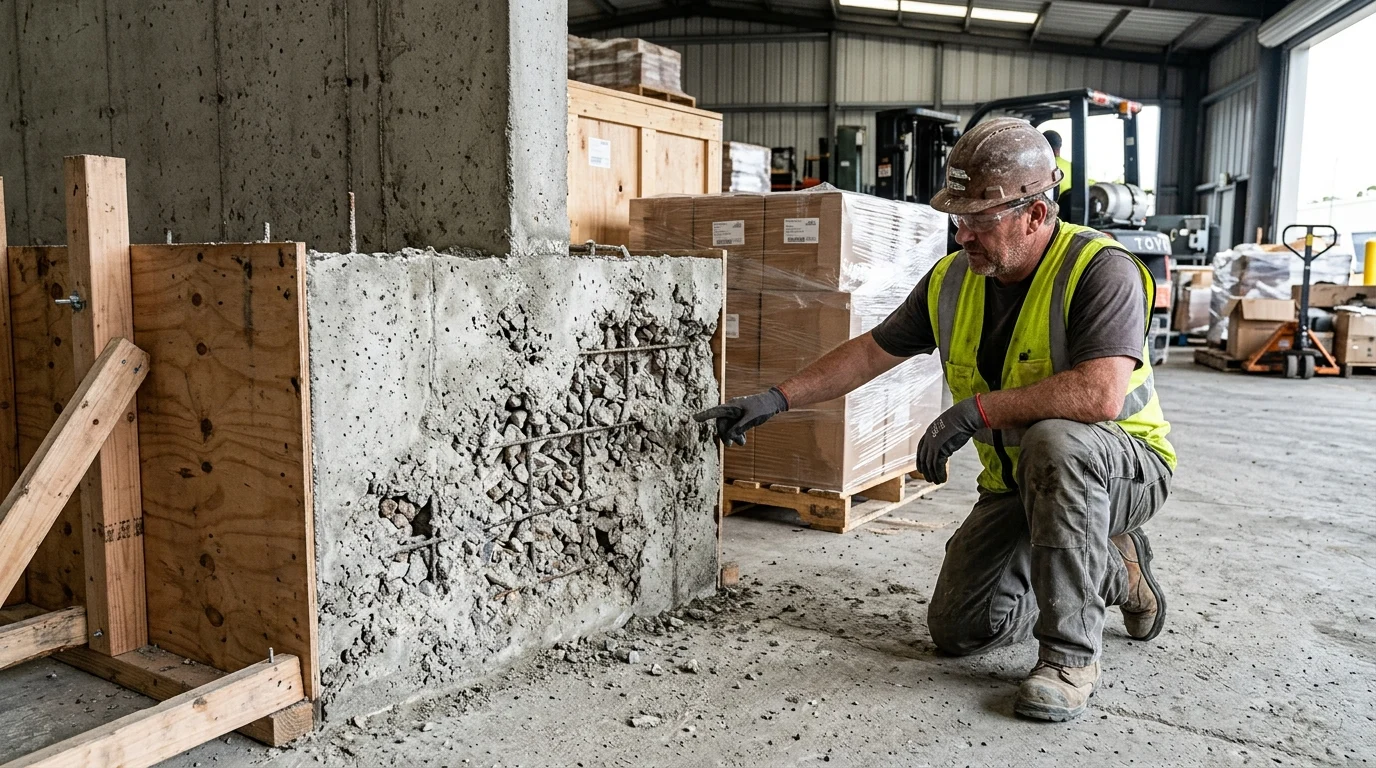
Understanding how to prevent honeycombing requires an examination of the physical mechanisms that cause it. Honeycombing occurs when coarse aggregates bridge together, preventing the finer mortar from filling the voids between them. This phenomenon is almost entirely driven by improper rheological management during the pour. When concrete is placed, its internal friction is high; the angularity of the crushed stone and the cohesiveness of the cement paste resist flow. If the energy applied to the concrete is insufficient to break this friction, the material remains in a state of localized suspension, locking air pockets and aggregate clusters permanently in place.
Several factors compound this issue, including excessive free-fall distances during placement, congested reinforcing steel, and highly viscous mix designs. When concrete is dropped from heights exceeding 3 to 5 feet without the use of a tremie or elephant trunk, the larger aggregates separate from the mortar, leading to segregation. Once segregation occurs, honeycombing is inevitable unless aggressive and precise mechanical vibration is applied to reintegrate the mix components.
Entrapped Air and Poor Aggregate Movement
The primary culprit behind honeycombing is the inability of entrapped air and aggregate to move freely within the formwork. Fresh concrete behaves as a Bingham plastic; it will not flow until a specific threshold of force, known as the yield stress, is applied. Until this yield stress is overcome, the entrapped air bubbles—which can range from microscopic voids to pockets several inches in diameter—are trapped by the surrounding aggregate matrix. Because air is significantly less dense than the surrounding materials, it possesses a natural buoyancy, but it lacks the kinetic energy required to push past the interlocking coarse aggregates.
Poor aggregate movement also occurs when the mix design features a high volume of coarse aggregate relative to the fine aggregate and paste content. In heavily congested forms, such as shear walls or mat foundations with complex rebar cages, coarse aggregates can easily snag on the steel. Without the fluidizing effect of a concrete vibrator, these aggregates form dams that block the flow of mortar, starving lower sections of the formwork of cement paste and resulting in severe, localized honeycombing.
How Frequency, Amplitude, and Energy Improve Consolidation
Concrete vibrators solve the problem of entrapped air and aggregate bridging through the precise application of frequency, amplitude, and centrifugal force. Frequency, measured in vibrations per minute (vpm), dictates the speed of the oscillatory movement. Amplitude measures the maximum distance the vibrator head travels from its axis of rotation. Together, these metrics determine the kinetic energy transferred to the concrete, effectively lowering its dynamic viscosity.
| Vibration Parameter | Typical Operating Range | Primary Effect on Concrete Matrix |
|---|---|---|
| Frequency | 8,000 – 17,000 vpm | Liquefies the mortar, reduces internal friction, and mobilizes fine particles. |
| Amplitude | 0.015 – 0.080 inches | Displaces coarse aggregate, breaks aggregate bridging, and drives out large entrapped air voids. |
| Centrifugal Force | 100 – 3,000 lbs | Determines the overall radius of action and the depth of energy penetration into the mix. |
High-frequency vibration (typically above 10,000 vpm) is particularly effective at fluidizing the mortar phase of the concrete, allowing the paste to coat the aggregates and flow into tight spaces. Conversely, higher amplitude is required to physically push the heavier coarse aggregates out of the way, creating channels for the buoyant air bubbles to escape to the surface. The synergistic effect of optimal frequency and amplitude ensures that the mix is thoroughly consolidated, eliminating the voids that cause honeycombing while preventing the heavier aggregates from sinking too rapidly, which would cause segregation.
Best Concrete Vibrators for Different Placement Conditions
Selecting the correct concrete vibrator is not a one-size-fits-all endeavor. The equipment must be matched to the specific placement conditions, including the geometry of the formwork, the density of the reinforcing steel, and the rheological properties of the concrete mix. Deploying an undersized vibrator will fail to consolidate the mix, while using an oversized vibrator in a confined space can lead to over-vibration, formwork blowout, or severe segregation.
Vibrators are generally classified by their method of application: internal (immersion or poker vibrators), external (form vibrators), and surface (screed vibrators). Understanding the operational parameters and limitations of each category is critical for developing an effective concrete placement plan that guarantees structural integrity and aesthetic quality.
When to Use Internal Concrete Vibrators
Internal Concrete Vibrators, commonly referred to as poker or immersion vibrators, are the industry standard for the vast majority of concrete placements, including slabs, columns, beams, and structural walls. They consist of a vibrating head connected to a power unit via a flexible shaft. Internal vibrators are utilized whenever the formwork allows direct access to the freshly placed concrete, enabling the operator to insert the vibrating head directly into the core of the mix.
The effectiveness of an internal vibrator is defined by its radius of action—the distance from the center of the vibrator head to the outer edge of the consolidated concrete. This radius typically ranges from 3 to 14 inches, depending on the head diameter and the slump of the concrete. Internal vibration is the most efficient method of consolidation because 100% of the mechanical energy is transferred directly into the concrete mass, unlike external vibration where energy is lost through the formwork.
Comparison of Concrete Vibrator Types
Different placement scenarios demand different modes of vibration. While internal vibrators are ubiquitous, external and surface vibrators play crucial roles in specialized applications.
| Vibrator Category | Typical Application | Radius / Depth of Effect | Common Power Sources |
|---|---|---|---|
| Internal (Poker) | Columns, walls, slabs, foundations | 3 to 14 inches (radius) | Electric, Pneumatic, Gas, Battery |
| External (Form) | Precast elements, heavily congested walls, tunnel linings | 6 to 12 inches (depth penetration) | Electric, Pneumatic |
| Surface (Screed) | Large flatwork, bridge decks, industrial floors | Up to 8 inches (depth penetration) | Gas, Electric |
External vibrators are rigidly attached to the exterior of the formwork. They are essential when the internal reinforcement is so dense that a poker vibrator cannot be inserted, or in precast manufacturing where automated, consistent vibration is required. Surface vibrators, such as vibrating screeds, are deployed for flatwork. They consolidate the concrete from the top down while simultaneously striking off the surface to the desired elevation, though their effective depth is limited, often requiring supplementary internal vibration for slabs thicker than 8 inches.
How Mix Design, Aggregate Size, and Form Geometry Affect Selection
The physical characteristics of the concrete mix and the spatial constraints of the formwork directly dictate vibrator selection. For low-slump concrete (less than 3 inches), the internal friction is exceptionally high. Consolidating these stiff mixes requires vibrators with high amplitude and high centrifugal force to physically displace the sluggish aggregates. Conversely, high-slump or self-consolidating concretes (SCC) require minimal vibration; applying high-amplitude energy to a fluid mix will rapidly induce segregation, driving the coarse aggregates to the bottom and leaving a weak layer of laitance at the top.
Aggregate size and rebar congestion further refine the selection process. The diameter of the vibrator head must be at least 0.25 inches smaller than the tightest clear spacing between reinforcing bars to prevent the equipment from becoming wedged. In heavily congested columns, operators may be restricted to using 1-inch to 1.5-inch diameter heads. Because smaller heads have a significantly reduced radius of action, the operator must increase the number of insertions to ensure overlapping zones of consolidation, directly impacting the labor time required for the pour.
How to Use Concrete Vibrators on Site
Even the most advanced concrete vibrator will fail to prevent honeycombing if it is operated incorrectly. Consolidation is a precise, repetitive process that relies heavily on the technique of the operator. Poor practices, such as dragging the vibrator through the concrete, leaving it in one spot for too long, or failing to penetrate the previous lift, are common sources of structural defects.
Effective on-site execution requires a systematic approach to insertion spacing, careful observation of the concrete's behavioral changes during vibration, and tight logistical coordination between the concrete delivery rate and the consolidation capacity of the placement crew.
Insertion Spacing, Depth, and Duration
To achieve uniform consolidation, the vibrator must be inserted vertically into the concrete at regular, overlapping intervals. The standard rule of thumb is to space insertions at a distance equal to 1.5 times the vibrator's radius of action. For a typical 2-inch diameter head with an 8-inch radius of action, insertions should occur every 12 inches. Random or widely spaced insertions will leave unconsolidated dead zones between the radii, resulting in internal honeycombing.
The depth and duration of each insertion are equally critical. When placing concrete in multiple lifts, the vibrator head must penetrate at least 6 inches into the previously placed, still-plastic lift. This stitches the two layers together, eliminating the risk of cold joints. The vibrator should remain in place for 5 to 15 seconds per insertion, depending on the mix stiffness. Withdrawal must be slow and deliberate—typically at a rate of 1 inch per second—to allow the concrete to flow back together and fill the hole left by the vibrator head. Rapid extraction will leave a permanent void, commonly known as a "bug hole" or "rathole."
Field Signs of Proper and Poor Consolidation
Operators must rely on visual and auditory cues to determine when a section of concrete is fully consolidated. The most obvious field sign of proper consolidation is the cessation of large air bubbles escaping to the surface. As the entrapped air is driven out, the surface of the concrete will take on a flattened, glistening appearance, indicating that a thin film of mortar has coated the top. Additionally, experienced operators listen for a distinct change in the pitch of the vibrator motor; as the concrete densifies, the load on the motor increases, causing a recognizable drop in the frequency tone.
Conversely, signs of poor consolidation include visible pockets of coarse aggregate at the surface or against the formwork. On the other end of the spectrum, over-vibration presents its own set of field warnings. If a thick layer of watery paste (laitance) rapidly accumulates on the surface, or if the coarse aggregates completely disappear from view, the mix has begun to segregate. Over-vibration severely weakens the top layer of the concrete, leading to surface scaling, dusting, and reduced abrasion resistance in the final product.
Coordinating Vibration With Concrete Delivery and Placement
Consolidation cannot be viewed in isolation; it must be perfectly synchronized with the concrete delivery and placement rates. Every vibrator has a maximum processing capacity, typically measured in cubic yards per hour. For example, a standard 2-inch internal vibrator can effectively consolidate roughly 3 to 6 cubic yards of concrete per hour. If the pump truck is placing 20 cubic yards per hour, a single operator will be hopelessly overwhelmed, virtually guaranteeing that large sections of the pour will remain unconsolidated.
Project managers must calculate the required number of vibrators and operators based on the anticipated pour rate, always keeping backup units on standby in case of mechanical failure. Furthermore, concrete should be placed in level lifts, generally not exceeding 12 to 20 inches in depth. Attempting to vibrate massive, deep piles of concrete limits the escape routes for entrapped air and forces the operator to use the vibrator to move the concrete laterally—a practice that inevitably causes severe segregation and honeycombing.
How to Specify and Procure Concrete Vibrators
Procuring the right concrete vibrators for a commercial or industrial project involves balancing capital costs, operational efficiency, and job-site infrastructure constraints. The specification process must translate structural engineering requirements into mechanical equipment parameters.
Contractors must evaluate not only the raw performance metrics of the vibrators but also the regulatory compliance, power availability, and long-term maintenance implications of their fleet. A structured procurement framework ensures that the selected equipment maximizes labor productivity while minimizing the risk of defective concrete placement.
Key Specification Factors: Head Diameter, Power, and Frequency
The three most critical specification factors for an internal concrete vibrator are head diameter, power source, and frequency. Head diameter dictates the volume of concrete that can be processed per insertion. While a 1-inch head is necessary for tight rebar configurations, it may only process 1 to 2 cubic yards per hour. Stepping up to a 2.5-inch head increases the processing capacity to upwards of 8 cubic yards per hour, significantly reducing labor time on mass pours. Therefore, specifications must detail a fleet mix that addresses both bulk placement and congested zones.
Power source selection depends on site conditions. High-frequency Electric Vibrators are lightweight and highly portable, making them ideal for commercial building construction. Pneumatic vibrators, driven by compressed air, offer exceptional durability and continuous high-amplitude operation without the risk of electrical burnout, making them favored in heavy civil and tunneling projects. However, pneumatic units require substantial infrastructure, often demanding 40 to 60 CFM (cubic feet per minute) of air per vibrator. Gas-powered backpack units provide ultimate mobility for flatwork but introduce emissions restrictions in enclosed spaces.
Compliance, Safety, Noise, and Electrical Protection
Safety and regulatory compliance must heavily influence procurement decisions. Concrete vibrators generate significant noise and mechanical stress. Under OSHA regulations, operators exposed to noise levels exceeding 85 dBA as an 8-hour Time-Weighted Average (TWA) must be enrolled in a hearing conservation program. Procurement teams should prioritize vibrators engineered with noise-dampening motor housings to minimize job-site acoustic hazards.
Additionally, prolonged use of high-vibration equipment exposes operators to Hand-Arm Vibration Syndrome (HAVS). Specifying vibrators with ergonomically isolated handles or vibration-dampening shafts is critical for occupational health. From an electrical standpoint, any 115V or 230V electric vibrator must be paired with Ground Fault Circuit Interrupter (GFCI) protection due to the inherently wet nature of concrete placement. Alternatively, many modern high-frequency systems operate on a safer 42V to 48V platform via an external inverter, dramatically reducing the risk of fatal electrical shocks on the job site.
Decision Framework for Choosing Concrete Vibrators
Choosing the optimal concrete vibrator requires a comprehensive decision framework that accounts for lifecycle cost analysis rather than just initial purchase price. For high-volume, continuous pouring operations, investing in heavy-duty pneumatic vibrators may yield a lower total cost of ownership due to their mechanical simplicity and resistance to overheating, despite the higher initial cost of air compressors.
For mid-sized commercial contractors, a standardized fleet of 115V electric flexible-shaft vibrators offers the best balance of versatility, cost, and ease of maintenance.
Key Takeaways
- Use mechanical vibration during placement because unconsolidated concrete can contain significant entrapped air that weakens density and durability.
- Treat each 1% of remaining entrapped air as a major quality risk because it can reduce compressive strength by about 5%.
- Vibrate concrete around rebar, corners, and embedments to eliminate voids that can reduce bond strength and accelerate corrosion.
- Stop vibration when visible air release subsides and the surface becomes glossy to avoid over-vibration and segregation.
- Select the vibrator type, shaft size, and frequency to match the formwork depth, reinforcement spacing, and concrete mix workability.
Frequently Asked Questions
What causes honeycombing in concrete?
Honeycombing occurs when trapped air and voids remain in fresh concrete, preventing mortar from fully surrounding coarse aggregate, rebar, and formwork corners.
How does a concrete vibrator remove trapped air?
A concrete vibrator sends high-frequency energy into the mix, temporarily fluidizing the mortar so air bubbles rise and aggregates settle into a denser structure.
How much can trapped air reduce concrete strength?
As a rule of thumb, every 1% of entrapped air can reduce compressive strength by about 5%, so poor consolidation quickly becomes a structural risk.
Can concrete be consolidated without a vibrator?
Manual rodding may help small, simple placements, but it is usually insufficient for reinforced forms, low-slump mixes, and commercial concrete work.
What types of concrete vibrators are commonly used?
Common options include internal vibrators with flexible shafts, external form vibrators, and surface vibrators, many of which are supplied by construction equipment manufacturers such as Max Machinery.