Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


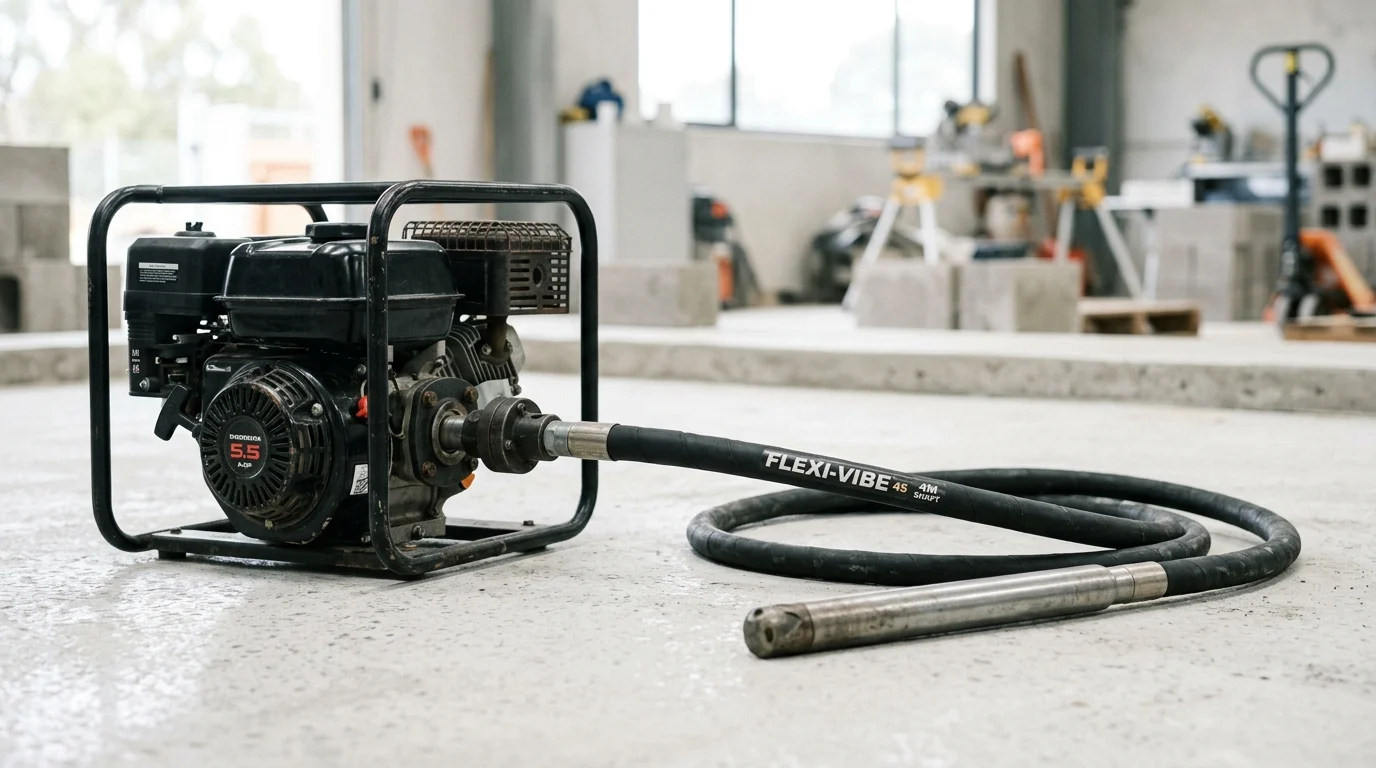
A jammed Concrete Vibrator can turn a controlled pour into a costly race against setting time. Flexible shaft units are built to deliver high-frequency consolidation, often in the 10,000–12,000 VPM range, but their performance depends on clean rotation, proper lubrication, sound casing, and correct operator technique. When friction rises or the head becomes trapped in reinforcement, vibration output can fall fast, leaving concrete vulnerable to air voids, honeycombing, and weak zones. This article explains the practical reasons these tools seize during construction, how to read early warning signs, and what crews can do to protect equipment, labor productivity, and finished concrete quality.
Why Flexible Shaft Concrete Vibrators Jam
The flexible shaft concrete vibrator is an indispensable tool in modern construction, engineered to consolidate freshly poured concrete by eliminating entrapped air and ensuring uniform aggregate distribution. This equipment relies on a high-speed rotational mechanism to generate vibrations, which temporarily liquefy the concrete mix to remove voids and consolidate the material around complex reinforcement structures.
However, despite its critical role, the flexible shaft is highly susceptible to operational failures, with jamming being one of the most frequent and disruptive issues encountered on the job site. A jammed vibrator halts the consolidation process, threatening the structural integrity of the pour and introducing severe logistical bottlenecks. Understanding the root causes of these jams requires a comprehensive analysis of mechanical fatigue, material dynamics, and operator technique.
Common causes of vibrator jamming
Jamming in flexible shaft concrete vibrators typically stems from a convergence of mechanical degradation, incorrect operational techniques, and adverse material conditions. The core mechanism involves an inner wire rope shaft rotating at high speeds within a protective outer casing. Under optimal conditions, a standard pendulum-type vibrator operates at frequencies between 10,000 and 12,000 Vibrations Per Minute (VPM).
When the rotational friction exceeds the motor's torque capacity, the shaft binds or seizes. Common catalysts include the ingress of abrasive concrete slurry through microscopic tears in the outer casing, insufficient lubrication of the inner core, and severe physical entrapment between reinforcing steel bars. Furthermore, a sudden drop in operating frequency below 8,000 VPM is often the first quantitative indicator of an impending jam, signaling that the drive unit is struggling against abnormal internal or external resistance.
How downtime affects concrete quality and labor
When a vibrator jams mid-pour, the immediate consequence is an abrupt interruption of the consolidation process, leading directly to compromised concrete quality. Unconsolidated concrete is highly prone to honeycombing, severe surface blemishes, and excessive entrapped air voids, which collectively reduce the final compressive strength of the structure by up to 30%.
Beyond structural integrity, equipment downtime introduces severe labor and financial penalties. Concrete possesses a strict setting time window, typically ranging from 45 to 90 minutes depending on the mix design and ambient temperature. If a jammed vibrator cannot be rapidly replaced or repaired within this window, the risk of forming cold joints increases exponentially. Consequently, unexpected equipment failures can incur costs ranging from $500 to over $1,500 per delayed truckload, factoring in wasted material, idle labor hours, and subsequent concrete remediation efforts.
When jamming signals a serious equipment issue
Not all jams are created equal; it is critical for site managers to distinguish between a temporary operational snag and a catastrophic equipment failure. A temporary jam often occurs when the vibrator head becomes wedged in tightly spaced rebar, requiring only a brief repositioning by the operator to resolve. However, if the shaft remains immobilized while the motor continues to draw power, the situation escalates rapidly.
A hard mechanical jam often signals a broken inner core, a shattered eccentric weight bearing, or a completely stripped motor coupling. If the inner core snaps under torsional overload, the kinetic energy is instantly transferred to the outer casing, potentially causing it to violently rupture. In these scenarios, the jamming is not merely an inconvenience but a definitive end-of-life event for the shaft assembly, necessitating immediate replacement and a thorough inspection of the drive unit to ensure the electrical components have not suffered thermal damage.
Mechanical Causes of Shaft and Head Failure
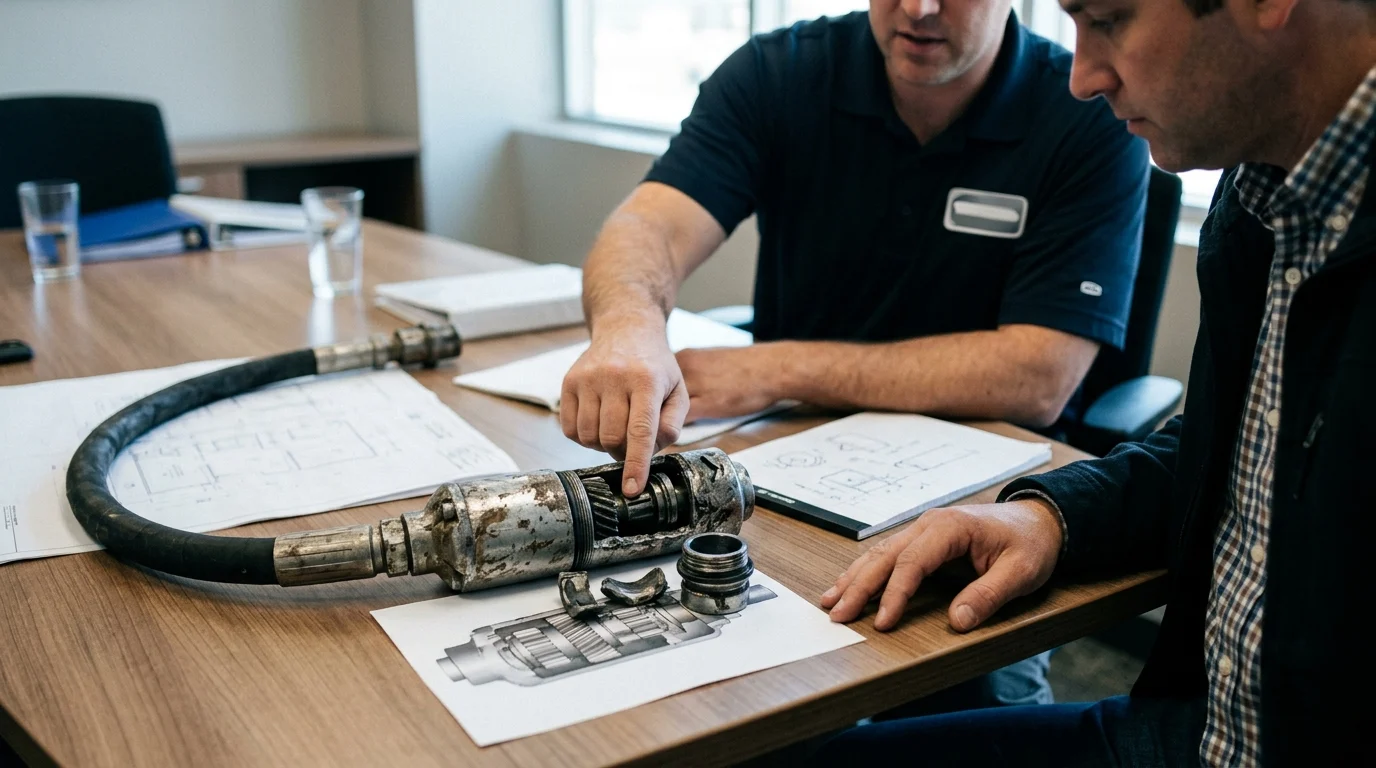
A thorough understanding of the internal mechanics is required to diagnose why flexible shaft Concrete Vibrators fail under load. The primary powertrain consists of an electric or internal combustion drive unit, a quick-disconnect coupling, a flexible transmission shaft, and the vibrating head containing an eccentric weight.
The flexible shaft itself is a highly engineered component, consisting of a multi-layered, high-tensile steel wire core spinning inside a reinforced rubber and steel mesh outer casing. The tolerances within this assembly are exceptionally tight, and any mechanical deviation rapidly compounds into excessive friction, heat generation, and eventual seizure.
Motor, coupling, casing, and shaft problems
Mechanical failures frequently originate at the interface points between the motor, the coupling, the casing, and the shaft. Misalignment between the drive unit and the flexible core connection is a primary culprit, leading to uneven rotational stress that quickly strips the coupling threads or shears the drive pins.
Furthermore, the integrity of the outer casing is paramount. Standard manufacturing tolerances dictate a radial clearance of roughly 1.5mm to 2.0mm between the spinning inner core and the outer casing lining. If the casing suffers a puncture or severe abrasion, highly abrasive cementitious paste can penetrate this narrow clearance. Once inside, the silica particles act as a destructive grinding compound, rapidly eroding the inner core and causing the rotating assembly to lock solid against the casing walls.
Wear patterns inside the flexible shaft and vibrator head
Internal wear patterns provide critical forensic evidence when diagnosing a jammed vibrator. When a flexible shaft is extracted for inspection, maintenance personnel often observe distinct polishing or fraying along specific sections of the wire rope core. Fraying indicates localized torsional fatigue, usually caused by the core binding momentarily while the motor continues to apply rotational force.
Inside the vibrator head, failure patterns are typically centered around the high-speed bearings supporting the eccentric weight. Because these bearings endure immense radial loads and operate in a high-vibration environment, any degradation in bearing lubrication leads to rapid thermal expansion. Once the bearings expand beyond their engineered tolerances, they seize within the head housing, instantly locking the flexible shaft and causing a catastrophic jam.
Effects of bending radius, shaft length, and lubrication
The most frequent mechanical catalyst for shaft seizure is a violation of the flexible shaft's minimum bending radius. The inner core relies on a relatively straight alignment to rotate freely. Bending the shaft too tightly forces the spinning wire rope into direct, high-pressure contact with the outer casing, increasing friction exponentially.
Industry standards dictate specific minimum bending radii based on the outer diameter of the flexible shaft. Exceeding these limits can increase internal friction by up to 300%, leading to rapid overheating and core breakage. Additionally, longer shafts (exceeding 6 meters) suffer from increased torsional wind-up, making proper lubrication vital. High-temperature lithium grease must be maintained along the entire length to mitigate the friction generated during normal flexing.
| Shaft Diameter (mm) | Standard Shaft Length (m) | Minimum Safe Bending Radius (mm) | Jamming Risk if Exceeded |
|---|---|---|---|
| 25 - 28 | 1.0 - 3.0 | 400 | High (Rapid Core Fraying) |
| 35 - 38 | 3.0 - 6.0 | 500 | Severe (Thermal Seizure) |
| 45 - 50 | 4.0 - 8.0 | 600 | Critical (Casing Rupture) |
| 60 - 70 | 4.0 - 12.0 | 800 | Critical (Motor Overload) |
Site Operation Errors That Cause Jamming
Even premium-grade consolidation equipment will succumb to jamming if operators deploy poor techniques during the pour. Site operation errors impose unnatural mechanical loads on the vibrator, forcing the equipment to operate outside its designed engineering parameters.
The interaction between the vibrating head, the dense network of reinforcing steel, and the heavy aggregate of the concrete mix creates a highly unforgiving environment. Consequently, operator training is just as critical as equipment maintenance in preventing mid-pour jams.
Improper insertion angle and excessive pulling force
Proper insertion technique dictates that the vibrator head must enter the concrete vertically and be allowed to sink under its own weight. A common operational error is forcing the vibrator into the mix at an angle or using it to drag concrete horizontally across the formwork. This improper lateral movement bends the shaft sharply at the point of entry and places immense shear stress on the head assembly.
Furthermore, operators must manage their extraction speed carefully. The standard withdrawal rate should be maintained between 1 to 3 inches per second to allow the concrete to flow back into the void left by the vibrator head. Pulling the shaft out too forcefully, especially when the head is temporarily wedged beneath rebar, applies extreme tensile load to the core. This excessive pulling force stretches the wire rope, narrowing its diameter slightly and causing it to slip or bind within the coupling mechanism, ultimately leading to a jam.
Impact of aggregate size, slump, rebar congestion, and concrete mix
The rheology and structural environment of the concrete pour significantly influence the likelihood of equipment jamming. Low slump concrete (measuring less than 2 inches) is highly viscous and offers immense resistance to the vibrating head, requiring higher amplitude to achieve consolidation. If an undersized vibrator is deployed in a low-slump mix, the motor may bog down and stall.
Additionally, rebar congestion is a primary physical hazard. In highly engineered structures, the density of #5 or #6 reinforcing bars creates narrow physical traps. If the aggregate size of the concrete mix is exceptionally large (e.g., exceeding 1.5 inches) and becomes wedged between the vibrator head and the rebar lattice, the vibrator can become permanently immobilized. The resulting friction from the spinning eccentric weight against the trapped aggregate can overheat and seize the head in minutes.
Warning signs of overheating, bearing failure, or blockage
Operators must be trained to recognize the pre-jamming warning signs to prevent irreversible equipment damage. One of the most immediate indicators is an audible drop in motor pitch, signaling a sudden loss of RPM due to overwhelming resistance. This is often accompanied by an increase in violent, erratic vibrations transmitted up the shaft into the operator's hands.
Thermal indicators are equally critical. Under normal operation, the cooling effect of the surrounding wet concrete regulates the temperature of the vibrator head and submerged casing. However, the exposed section of the flexible shaft should never become too hot to touch. A standard operational threshold dictates that the casing temperature should not exceed 60°C (140°F). Temperature spikes beyond this limit indicate severe internal friction, bearing degradation, or a localized blockage, warning the operator to shut down the unit immediately before the core snaps.
How to Troubleshoot a Jammed Concrete Vibrator
When a flexible shaft concrete vibrator jams on site, immediate and systematic troubleshooting is essential to mitigate downtime and prevent cascaded damage to the drive unit. Hasty attempts to force a jammed shaft to rotate by repeatedly cycling the power will almost certainly result in catastrophic motor burnout or a shattered internal core.
Effective troubleshooting requires isolating the mechanical components from the electrical or pneumatic power source, allowing maintenance personnel to diagnose the exact point of failure within the powertrain. A step-by-step approach ensures that replacement parts are deployed efficiently and safely.
Step-by-step inspection before restarting
The first protocol upon experiencing a jam is to immediately cut power to the drive unit to prevent thermal overload. Once safe, the operator should conduct a visual inspection of the outer casing, looking for sharp kinks, deep abrasions, or areas where the rubber has melted. Any severe kink in the casing is a definitive indicator of where the inner core is binding.
Next, the flexible shaft must be disconnected from the motor coupling. Maintenance personnel should attempt to turn the inner core manually using specialized grips or pliers. If the core rotates freely by hand but the unit fails to vibrate when connected, the issue likely resides in a stripped motor coupling. Conversely, if the core is completely immovable by hand, the fault is isolated to a mechanical seizure within the shaft casing or the vibrator head bearings.
How to separate mechanical faults from electrical faults
Differentiating between a seized mechanical component and a failing electrical motor is a critical step in the troubleshooting matrix. This is achieved by running the drive unit independently of the flexible shaft. If the motor runs smoothly at its rated RPM without the shaft attached, the electrical system is viable, and the jam is entirely mechanical.
To verify motor health, technicians should utilize a multimeter to check the amperage draw under no-load and simulated load conditions. For example, a standard 1.5 HP Electric Vibrator motor typically draws between 10 to 12 Amps under a normal concrete consolidation load. If the motor draws in excess of 18 Amps immediately upon startup with the shaft attached, it confirms a severe mechanical bind is forcing the motor into a locked-rotor state, which will trip thermal breakers or melt stator windings if left unchecked.
| Symptom Observed | Electrical or Mechanical | Diagnostic Action Required | Expected Resolution |
|---|---|---|---|
| Motor hums, shaft won't spin | Electrical / Mechanical | Disconnect shaft; test motor amps | Replace seized shaft or blown capacitor |
| Shaft spins, head doesn't vibrate | Mechanical | Inspect inner core and head assembly | Replace snapped core or seized bearings |
| Erratic RPM, casing overheating | Mechanical | Check shaft bend radius and lubrication | Straighten shaft, apply lithium grease |
| Repeated breaker tripping | Electrical | Inspect power cord, plug, and stator | Repair electrical short; verify voltage |
When to clean, lubricate, repair, or replace parts
Once the fault is isolated, maintenance personnel must decide the appropriate intervention: clean, lubricate, repair, or replace. If the inner core exhibits minor surface rust or dry spots but remains structurally intact, it can be extracted, thoroughly cleaned with a solvent, and re-lubricated. Industry best practices recommend re-lubricating the inner core every 50 to 100 operating hours with a specific volume of high-temperature lithium grease (typically 1.5 to 2.0 grams of grease per meter of shaft).
However, repair is not always viable. If the inner wire rope shows any signs of fraying, broken strands, or permanent torsional deformation (bird-caging), it must be replaced immediately. Attempting to salvage a compromised core will inevitably result in a secondary break during the next pour. Similarly, if the vibrator head has seized due to concrete slurry penetrating a failed seal, the internal bearings are usually beyond repair, necessitating a complete replacement of the head assembly to restore reliable operation.
How to Select and Maintain the Right Vibrator
Preventing vibrator jamming begins long before the equipment reaches the construction site. Strategic procurement, based on the specific structural demands of the project, combined with a rigorous, proactive maintenance schedule, forms the foundation of reliable concrete consolidation.
Contractors must view flexible shaft vibrators not as disposable commodities, but as precision mechanical assets. Selecting the correct specifications and balancing upfront costs against long-term operational lifespan drastically reduces the frequency of mid-pour equipment failures.
Key specifications for shaft, head, motor, and job size
Proper equipment selection requires matching the vibrator's specifications to the structural parameters of the concrete formwork. The most critical dimension is the vibrator head diameter. As a strict engineering rule, the vibrator head diameter must be at least 1 inch (25mm) smaller than the minimum clear spacing between the reinforcing steel bars to prevent physical entrapment and jamming.
Furthermore, the motor output and shaft length must be scaled to the job size. Deep wall pours require longer shafts, but specifying a shaft longer than necessary increases internal friction and the probability of kinking. Contractors must also evaluate the radius of action—the area over which the vibrator effectively consolidates concrete. A 50mm (2-inch) head typically offers a radius of action of 350mm to 500mm. Selecting an undersized head forces the operator to overwork the equipment, pushing the motor and shaft beyond their thermal limits and accelerating the conditions that lead to jamming.
Preventive maintenance schedule for daily and periodic use
A rigorous preventive maintenance schedule is the most effective defense against unexpected jamming. Daily maintenance should include thoroughly wiping down the outer casing to remove wet concrete before it cures, as hardened concrete limits the shaft's flexibility and promotes cracking. Operators must also visually inspect the casing for pinhole leaks and verify the integrity of the quick-disconnect coupling before every shift.
Periodic maintenance requires a deeper mechanical intervention. Every 100 operating hours, the flexible shaft should be decoupled from the head and motor. The inner core must be fully extracted, inspected for microscopic fraying, and re-greased. Simultaneously, the oil level in the vibrator head (if applicable to the specific design) must be checked and replenished. Neglecting this periodic teardown guarantees that friction will eventually overcome the powertrain, resulting in a sudden, costly seizure.
Balancing purchase cost, spare parts, and service life
Procurement decisions often dictate the long-term reliability of consolidation equipment. While budget-tier flexible shaft vibrators present an attractive initial purchase price, they frequently utilize lower-grade steel cores and thinner rubber casings that are highly susceptible to premature wear and jamming under heavy commercial use.
Analyzing the Total Cost of Ownership (TCO) reveals that investing in premium equipment is highly economical. High-frequency vibrators with reinforced, multi-ply casings and precision-machined bearings may carry a 40% higher upfront purchase cost. However, field data demonstrates that these premium units can reduce jamming-related downtime by over 60% and double the operational service life of the shaft. For contractors managing large-scale pours, avoiding the $1,000 penalty of a single delayed concrete truck yields a positive Return on Investment (ROI) on premium vibrators within the first six months of continuous operation.
Key Takeaways
- Monitor vibrator frequency because a drop from the normal 10,000–12,000 VPM range to below 8,000 VPM can indicate rising friction or an impending jam.
- Inspect the outer casing before every pour, since small tears can allow abrasive concrete slurry to enter and seize the rotating inner core.
- Keep the flexible shaft properly lubricated to reduce internal friction, overheating, and premature mechanical wear.
- Avoid forcing a vibrator head trapped in dense reinforcement, and instead stop, reposition, and restart only when the shaft can move freely.
- Prepare backup equipment before critical pours because concrete may begin setting within 45 to 90 minutes, increasing the risk of cold joints during downtime.
- Treat repeated jamming as a maintenance warning, not a minor inconvenience, because worn bearings, a damaged core, or a failing head can compromise both equipment and concrete quality.
Frequently Asked Questions
What is the most common reason a flexible shaft concrete vibrator jams?
The most common causes are insufficient lubrication, slurry entering a damaged casing, worn inner core components, or the head becoming trapped between reinforcing bars.
What operating speed indicates a vibrator may be close to jamming?
A healthy pendulum-type vibrator often runs around 10,000 to 12,000 VPM. A drop below about 8,000 VPM can signal abnormal resistance, wear, or an impending jam.
Can a jammed vibrator affect concrete strength?
Yes. Poor consolidation can leave honeycombing, air voids, and weak zones, potentially reducing concrete compressive strength and increasing repair costs.
Should operators force the vibrator free if it is stuck in rebar?
No. Forcing the shaft can kink the core, damage the casing, or break internal parts. Stop, reposition carefully, and restart only after confirming the shaft can rotate freely.
How often should a flexible shaft vibrator be inspected?
Inspect the shaft, casing, couplings, head, and lubrication condition before each pour. High-use equipment should receive more frequent maintenance based on site conditions.