Internal Vibrator
 External Vibrator
 Submersible Pump
 Eccentric shaft
 Pendulum shaft
 Portable vbrator shaft
 Portable concrete mixer
 Vertical concrete mixer
 Hydraulic concrete mixer
 Walk behind power trowel
 Ride on power trowel
 Concrete screed
 Tamping rammer
 Plate compactor
 Vibratory roller


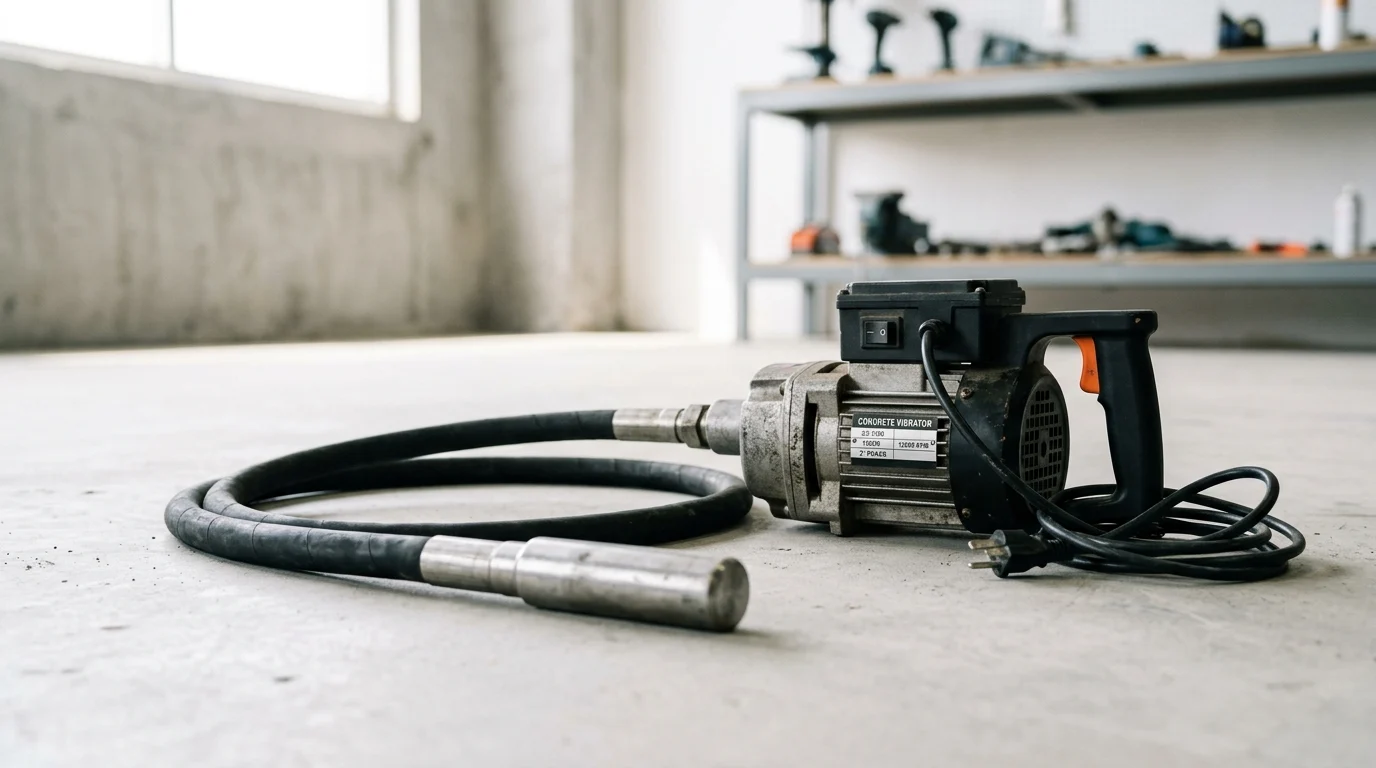
A jammed flexible shaft vibrator can turn a routine concrete pour into a costly delay within seconds. These tools are designed to deliver high-speed consolidation—often around 10,000 to 12,000 vibrations per minute—but that performance depends on smooth rotation through the shaft, casing, and poker head. When resistance changes from normal concrete drag to mechanical lock-up, the result can be twisted shafts, damaged casings, tripped breakers, and poor concrete compaction. This article explains how to recognize the difference between ordinary operating load and a true jam, what symptoms operators should watch for, and how proper handling and maintenance help protect both equipment and finished concrete quality.
Why Flexible Shaft Concrete Vibrators Jam
Flexible shaft concrete vibrators are critical instruments in modern construction, engineered to consolidate freshly poured concrete by expelling entrapped air and eliminating voids. These devices operate by transmitting high-speed rotational energy from an external power unit—typically an electric motor or a small internal combustion engine—through a flexible, wire-wound inner core to an eccentric mass located inside the poker head. Under optimal conditions, this mechanism generates operating frequencies ranging from 10,000 to 12,000 vibrations per minute (vpm), effectively fluidizing the mortar matrix and allowing aggregates to settle into a dense, uniform structure.
However, the operational environment of a concrete pour is inherently hostile. The flexible shaft must navigate congested reinforcement grids, highly abrasive materials, and demanding duty cycles. When the rotational movement of the inner core is restricted or halted entirely while the power unit continues to apply torque, a jam occurs. This mechanical interruption not only halts consolidation but introduces severe torsional stress that can permanently deform the shaft, rupture the outer casing, or cause significant electrical failure in the drive motor.
Jam vs Normal Operating Load
Distinguishing between the normal operational drag of concrete and a mechanical jam is the first step in equipment management. Fresh concrete acts as a dense, viscous fluid that naturally resists the high-frequency oscillations of the vibrator head. When inserted into a standard structural mix with a slump of 3 to 5 inches, the vibrator will experience a predictable load increase. This normal operating load typically causes a slight drop in motor speed—often reducing the rotational velocity by 10% to 15%—which is accompanied by a deeper, sustained pitch from the motor.
A jam, conversely, represents an immediate and abnormal spike in mechanical resistance that exceeds the torque capacity of the drive system. Rather than a steady, manageable drag, a jam arrests the rotation of the eccentric weight or binds the inner core against the casing. It manifests as a sudden lock-up where the kinetic energy of the motor is abruptly converted into intense torsional strain along the flexible shaft, often causing the casing to forcefully twist or buck in the operator's hands.
Common Symptoms on Site
On an active construction site, a jammed flexible shaft vibrator presents several immediate, identifiable symptoms. The most obvious indicator is acoustic: the drive motor will transition from a steady hum to a high-pitched whine or a deep, struggling growl as it attempts to overcome the immobility of the shaft. Electric power units will draw excessive current, frequently tripping thermal overload protectors or standard 15-amp to 20-amp circuit breakers at the distribution panel.
Physical symptoms are equally pronounced. An operator holding the flexible casing will feel the high-frequency vibrations drop instantly to zero. Instead of vibration, the shaft may exhibit strong torque reaction, stiffening rigidly or twisting into a helical coil as the inner wire rope binds against the rubberized outer tube. In cases where the jam is caused by internal friction rather than a wedged head, the casing may rapidly overheat, emitting the distinct odor of melting synthetic rubber or burning grease.
Effects on Productivity and Concrete Finish
The immediate consequence of a jammed vibrator is a sudden halt in the consolidation process, which poses risks to the structural integrity and aesthetic finish of the concrete element. If the pour continues without adequate vibration, the concrete will fail to flow completely around the rebar network. This results in honeycombing—a condition where coarse aggregates are exposed without a binding mortar matrix—and increases the likelihood of cold joints if subsequent layers are placed over unconsolidated material.
From a quality control perspective, failure to properly vibrate a section due to equipment jamming can leave entrapped air voids exceeding typical structural thresholds, which often allow only 1% to 2% entrapped air. This can noticeably reduce compressive strength. Furthermore, the loss of productivity is financially significant. A jammed vibrator that forces a halt in placement can idle a concrete crew and delay transit mixers, accumulating downtime costs that are often estimated at $150 to $300 per hour depending on the region, not including the potential costs of structural remediation or cosmetic patching required after the forms are stripped.
Mechanical and Material Causes
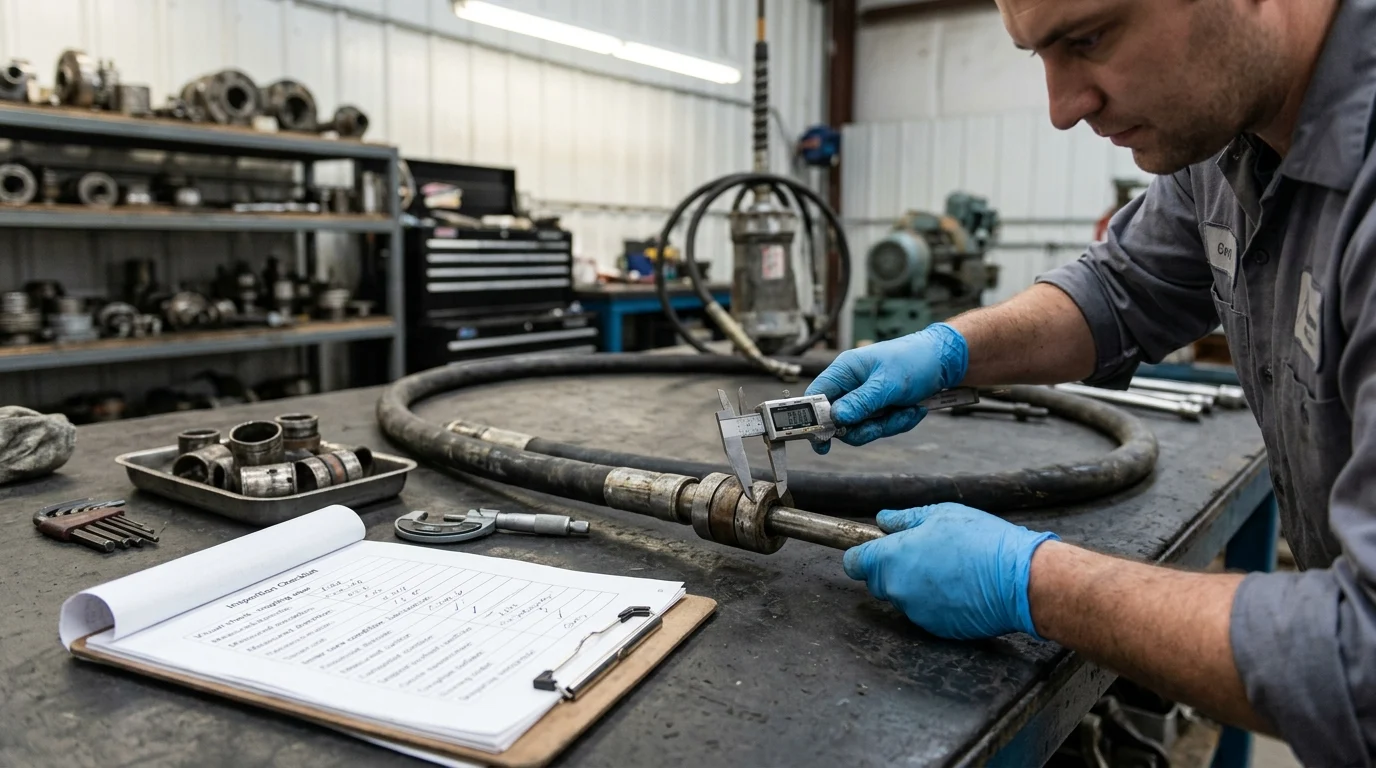
The architecture of a flexible shaft vibrator makes it uniquely vulnerable to a combination of mechanical fatigue and material-induced blockages. The shaft assembly typically consists of an inner core made from multiple layers of high-tensile steel wire wound in alternating directions, housed within an outer casing reinforced by wire braid and synthetic rubber. This design allows the transmission of torque around corners, but it also creates an environment where internal friction and external forces can easily disrupt operation.
Jams generally originate from one of three primary vectors: user-induced geometric stress, neglected internal maintenance, or overwhelming resistance from the concrete mix and surrounding formwork. Understanding the physics behind these failures is essential for implementing effective site protocols.
Over-Bending, Kinking, and Poor Bend Radius
The most frequent cause of internal jamming is the violation of the shaft's minimum bend radius. Flexible shafts are designed to bend, but they are not designed to fold or kink. Depending on the diameter of the core, manufacturers specify a strict minimum bend radius, typically ranging from 18 to 24 inches. When an operator bends the shaft tighter than this threshold—often to reach under a window block-out or around heavy rebar congestion—the inner core is forced into direct, high-pressure contact with the inner wall of the casing.
This over-bending disrupts the clearance necessary for smooth rotation. The high-speed rotation combined with this side-load generates excessive friction. The friction rapidly degrades the internal lining of the casing and can cause the alternating wire layers of the inner core to unspool or bird-cage. Once the core geometry is distorted, it binds within the casing, locking the shaft and stalling the motor.
Worn Bearings, Dry Cores, and Damaged Couplings
Internal mechanical failures frequently stem from poor lubrication and worn components. The inner core relies on a specific thin film of high-temperature grease to minimize friction against the casing. If the core runs dry, the resulting heat can exceed the thermal limits of the rubber casing, causing it to melt internally and fuse with the spinning wire rope. Similarly, the eccentric mass in the vibrator head rotates on precision bearings that endure high centrifugal forces. If these bearings wear out or lose their oil bath, they will seize, instantly halting the head and transferring significant shock loads back up the shaft.
Damaged couplings also play a critical role. The connectors that interface the flexible shaft with the motor and the vibrator head feature specific geometries (such as square drives or hexagonal tangs). Wear, metal fatigue, or the ingress of cement paste into these couplings can cause them to strip or bind.
| Failure Mode | Root Cause | Primary Symptom | Torque Impact |
|---|---|---|---|
| Core Seizure | Insufficient lubrication / Dry core | Shaft runs hot, emits smoke, localized casing melt | Complete loss of rotation, high risk of core snapping |
| Casing Rupture | Exceeded minimum bend radius | Visible wire mesh, irregular shaft twisting | High internal friction, erratic RPM drops |
| Bearing Lock-up | Seal failure, loss of oil in head | Sudden kickback at the head | Immediate torque spike, motor stall |
| Coupling Bind | Cement ingress or stripped tangs | Motor runs but head fails to vibrate | Intermittent power transfer, grinding noise |
Stiff Mixes, Large Aggregate, and Slump Loss
External factors related to the concrete mix design and the placement environment also contribute heavily to jamming incidents. Stiff, low-slump concrete mixes (measuring less than 2 inches of slump) present a significant physical barrier to the vibrator head. While the vibrator is designed to fluidize the mix immediately surrounding it, a highly cohesive, dry mix can collapse back onto the head too quickly, trapping it under the weight of the aggregate.
The presence of unusually large aggregate—particularly crushed stone exceeding 1.5 inches in diameter—exacerbates this risk. When the Vibrating Poker is inserted into heavily reinforced areas, such as columns with #8 rebar spaced tightly at 4-inch intervals, a large piece of aggregate can become wedged between the vibrating head and the steel reinforcement. This mechanical wedging physically locks the head in place. If the operator attempts to forcefully yank the shaft free while the motor is still applying torque, the flexible core can stretch, bind, and ultimately jam within the casing.
How to Diagnose a Jam
When a flexible shaft vibrator ceases to function correctly on the job site, rapid and accurate diagnosis is critical. A systematic approach to troubleshooting not only minimizes costly downtime but also prevents further damage to the equipment. Continuing to apply power to a jammed unit can escalate a simple, repairable bind into a destroyed motor armature or a snapped internal core.
Effective diagnosis requires the operator or mechanic to systematically break down the vibrator into its three primary discrete components: the power unit, the flexible transmission shaft, and the eccentric head. By isolating these elements, technicians can pinpoint the exact location of the mechanical failure.
Isolate the Power Unit, Shaft, and Head
The first diagnostic step is decoupling the system to test each segment independently. Begin by disconnecting the flexible shaft from the power unit. Once separated, activate the motor or engine under a no-load condition. If the electric motor hums smoothly, draws its rated idle current (typically under 5 amps for standard 120V units), and the output drive spins freely, the power unit can be eliminated as the source of the jam.
Next, evaluate the disconnected shaft and head assembly. An experienced technician will attempt to rotate the inner core tang by hand or with a small wrench. Under normal conditions, turning the core to spin the eccentric weight in the head should require minimal effort—often estimated around 5 to 10 in-lbs of torque, depending on the model. If the core refuses to turn, or requires significant leverage, the jam is isolated to either the flexible shaft casing or the bearings within the vibrator head. Disconnecting the head from the shaft allows the final isolation: if the bare shaft core spins freely but the head does not, the bearings have seized.
Match Symptoms to Probable Causes
Once the components are isolated, matching physical symptoms to probable causes dictates the repair strategy. Visual inspections often reveal the root issue without further disassembly. For instance, if the extracted inner core displays a dark blue or black discoloration, it confirms a severe overheating event due to lubrication failure, meaning the core is likely warped and requires replacement.
If the casing itself exhibits localized stretching, a permanent helical twist, or a spot where the internal wire braid has burst through the outer rubber, it indicates an over-torque event. This symptom usually correlates with the vibrator head becoming physically wedged in the formwork or rebar while the motor continued to drive the core. Conversely, if the core is snapped clean with frayed wire ends near the motor coupling, it suggests a sudden lock-up of the head that caused torsional failure before the motor could stall.
Follow Safety Checks Before Clearing
Safety must be the paramount concern when diagnosing and attempting to clear a jammed flexible shaft. A jammed shaft acts as a powerful torsional spring. As the motor attempts to turn the locked head, the high-tensile wire core winds tighter and tighter, storing a substantial amount of kinetic energy. If the jam is suddenly released, or if the shaft is decoupled without caution, this energy is rapidly discharged.
Before attempting any diagnostic disassembly, strict lockout/tagout procedures must be followed. For electric units, the plug must be entirely removed from the power receptacle—simply turning off the switch is insufficient, as a faulty switch could engage. For gas-powered backpacks, the spark plug wire must be disconnected. When uncoupling a jammed shaft from the motor, technicians must maintain a firm grip on the casing and wear heavy leather gloves to protect against lacerations from frayed wires or the sudden whipping motion of the shaft as it unwinds its stored tension.
Prevention Through Operation and Maintenance
The lifespan of a flexible shaft Concrete Vibrator is directly proportional to the rigor of the maintenance program and the operational habits of the user. While these tools are built forheavy-duty construction environments, their internal tolerances require precise care. A proactive approach to maintenance prevents the friction, heat, and fatigue that lead to sudden jamming.
Site managers must enforce strict operational protocols that respect the physical limitations of the equipment. Combining routine preventative maintenance with correct placement techniques ensures that the vibrator operates efficiently, consolidates concrete effectively, and avoids the mechanical stresses that cause the inner core to bind.
Lubrication, Cleaning, and Storage
Proper lubrication of the inner core is the single most critical maintenance task for flexible shaft vibrators. While maintenance intervals vary by manufacturer, a common industry guideline is pulling the inner core from the casing every 50 operating hours for cleaning and re-lubrication. The core should be wiped clean of old, degraded grease and inspected for broken wires or kinks. A fresh coat of specialized, high-temperature vibrator grease should be applied. The coating must be thin—often recommended to be roughly 1/16 inch thick—as over-greasing will cause the lubricant to migrate into the vibrator head, potentially stalling the eccentric mass.
Cleaning the exterior of the equipment is equally important. Concrete paste is highly caustic and abrasive; if allowed to cure on the casing or the motor housing, it restricts flexibility and traps heat. The shaft and head should be washed down immediately after each pour. Storage practices also impact longevity. Flexible shafts should never be stored in tight loops or thrown haphazardly into gang boxes. They must be stored either laid out perfectly flat on a rack or coiled in large, sweeping loops with a minimum diameter of 3 feet to prevent the inner core from taking a permanent set.
Insertion Depth, Withdrawal Rate, and Duty Cycle
Operational technique heavily influences the mechanical strain placed on the vibrator. The poker should always be inserted vertically into the concrete at regular intervals of 12 to 18 inches, allowing gravity to assist the penetration and preventing the shaft from bending sharply at the surface. Dragging the vibrator horizontally through the mix to move concrete is a primary cause of casing damage and core jamming, as it exerts heavy lateral stress on the assembly.
The withdrawal rate and duty cycle must also be managed carefully. The vibrator should be withdrawn slowly, at a rate of approximately 1 inch per second, to allow the concrete to flow back together and close the hole left by the head. Furthermore, operators must respect the tool's duty cycle. The vibrator head relies on the surrounding wet concrete acting as a heat sink to dissipate the high temperatures generated by the bearings (which can approach 200°F in some units). Running the vibrator out of the concrete for more than 10 to 15 seconds will cause the bearings to overheat, expand, and ultimately seize, resulting in an immediate jam.
Spare Shafts, Heads, Couplings, and Service Intervals
To mitigate the impact of inevitable wear and tear, maintaining a strategic inventory of spare parts is essential for any major concrete project. Industry best practice dictates keeping a minimum ratio of one spare shaft and head assembly for every three active power units on site. This redundancy allows for immediate swap-outs if a jam occurs, keeping the pour moving while the compromised shaft is taken offline for diagnosis.
Service intervals should be strictly documented according to the manufacturer's specific guidelines. Quick-disconnect couplings should be inspected weekly for wear and cleaned of any cement dust that could cause binding. Threaded couplings require routine checks for thread galling and should be assembled using medium-strength thread locker to prevent vibration-induced loosening. By adhering to a scheduled replacement program for high-wear items like the inner core and the head bearings, contractors can significantly reduce unexpected jamming incidents.
Selection and Repair Decisions
Preventing vibrator jams begins long before the concrete is poured; it starts with the precise selection of equipment tailored to the specific demands of the project. A mismatch between the vibrator's specifications and the concrete mix design or formwork geometry is a guaranteed pathway to mechanical failure. Selecting the correct shaft length, diameter, and head size ensures that the tool has the appropriate torque and amplitude to fluidize the mix without being overwhelmed.
Furthermore, equipment managers must establish clear criteria for when a jammed or damaged vibrator should be repaired versus when it must be retired. Making sound economic and technical decisions regarding the lifecycle of the equipment maintains site safety and operational efficiency.
Key Specifications: Shaft Length, Diameter, and Head Size
The geometry of the pour dictates the key specifications of the vibrator. Head sizes typically range from 7/8 inch for highly congested, thin-wall applications up to 2.5 inches for heavy civil footings. The rule of thumb is to use the largest head possible that can comfortably pass through the rebar grid with a minimum clearance of 1 to 2 inches on all sides. Forcing a large head into a tight space drastically increases the risk of the head wedging against the steel, leading to a severe jam.
Shaft length and diameter must also be optimized. Shafts are available in lengths from 2 feet up to 21 feet. While a longer shaft provides greater reach for deep wall pours, it also exponentially increases internal friction and torque loss. A thicker core diameter provides greater torsional strength to resist jamming but reduces flexibility. If a deep pour requires navigating multiple bends, operators must balance the need for reach against the core's minimum bend radius to prevent internal binding.
When to Use a Flexible Shaft Vibrator
Flexible shaft vibrators remain the industry standard for most cast-in-place concrete applications due to their versatility, lower initial cost,
When to Use a Flexible Shaft
Flexible shaft vibrators remain the industry standard for most cast-in-place concrete applications due to their versatility, lower initial cost,
Key Takeaways
- Stop the power unit immediately if vibration drops to zero and the flexible shaft twists, stiffens, or coils under torque.
- Treat a 10% to 15% motor speed drop in a 3- to 5-inch slump mix as normal load, but investigate any sudden lock-up or harsh motor sound.
- Watch for electrical warning signs such as thermal overload activation or repeated tripping of 15-amp to 20-amp breakers.
- Inspect the inner core, outer casing, couplings, and poker head before restarting after any jam to prevent permanent shaft or motor damage.
- Avoid sharp bends and forcing the poker head through congested reinforcement, because restricted rotation can overload the flexible shaft assembly.
Frequently Asked Questions
What causes a flexible shaft concrete vibrator to jam?
A jam occurs when the inner core or eccentric head can no longer rotate freely while the motor continues applying torque. Common triggers include binding in the casing, sharp shaft bends, debris, worn components, excessive load, or the poker head getting trapped in dense concrete or reinforcement.
How is a jam different from normal vibrator load?
Normal load in fresh concrete may reduce motor speed by about 10% to 15% and create a deeper steady sound. A jam is sudden: vibration stops, the shaft may twist or stiffen, and the motor may whine, growl, overheat, or trip a breaker.
What should an operator do when the shaft jams?
Stop the power unit immediately, remove the poker head carefully, and inspect the shaft, casing, couplings, and head before restarting. Continuing to run a jammed vibrator can deform the shaft, damage the casing, or overload the electric motor.
Can concrete mix conditions contribute to vibrator jamming?
Yes. Very stiff mixes, congested rebar, large aggregate, or low slump can increase resistance around the head. A standard 3- to 5-inch slump creates expected drag, but sudden lock-up or loss of vibration indicates a mechanical problem, not normal consolidation load.
Why does the breaker trip when a vibrator jams?
When the shaft or head locks, the motor draws excessive current as it tries to overcome the blockage. Electric units may trip thermal overload protection or common 15-amp to 20-amp circuit breakers to prevent overheating and electrical damage.